
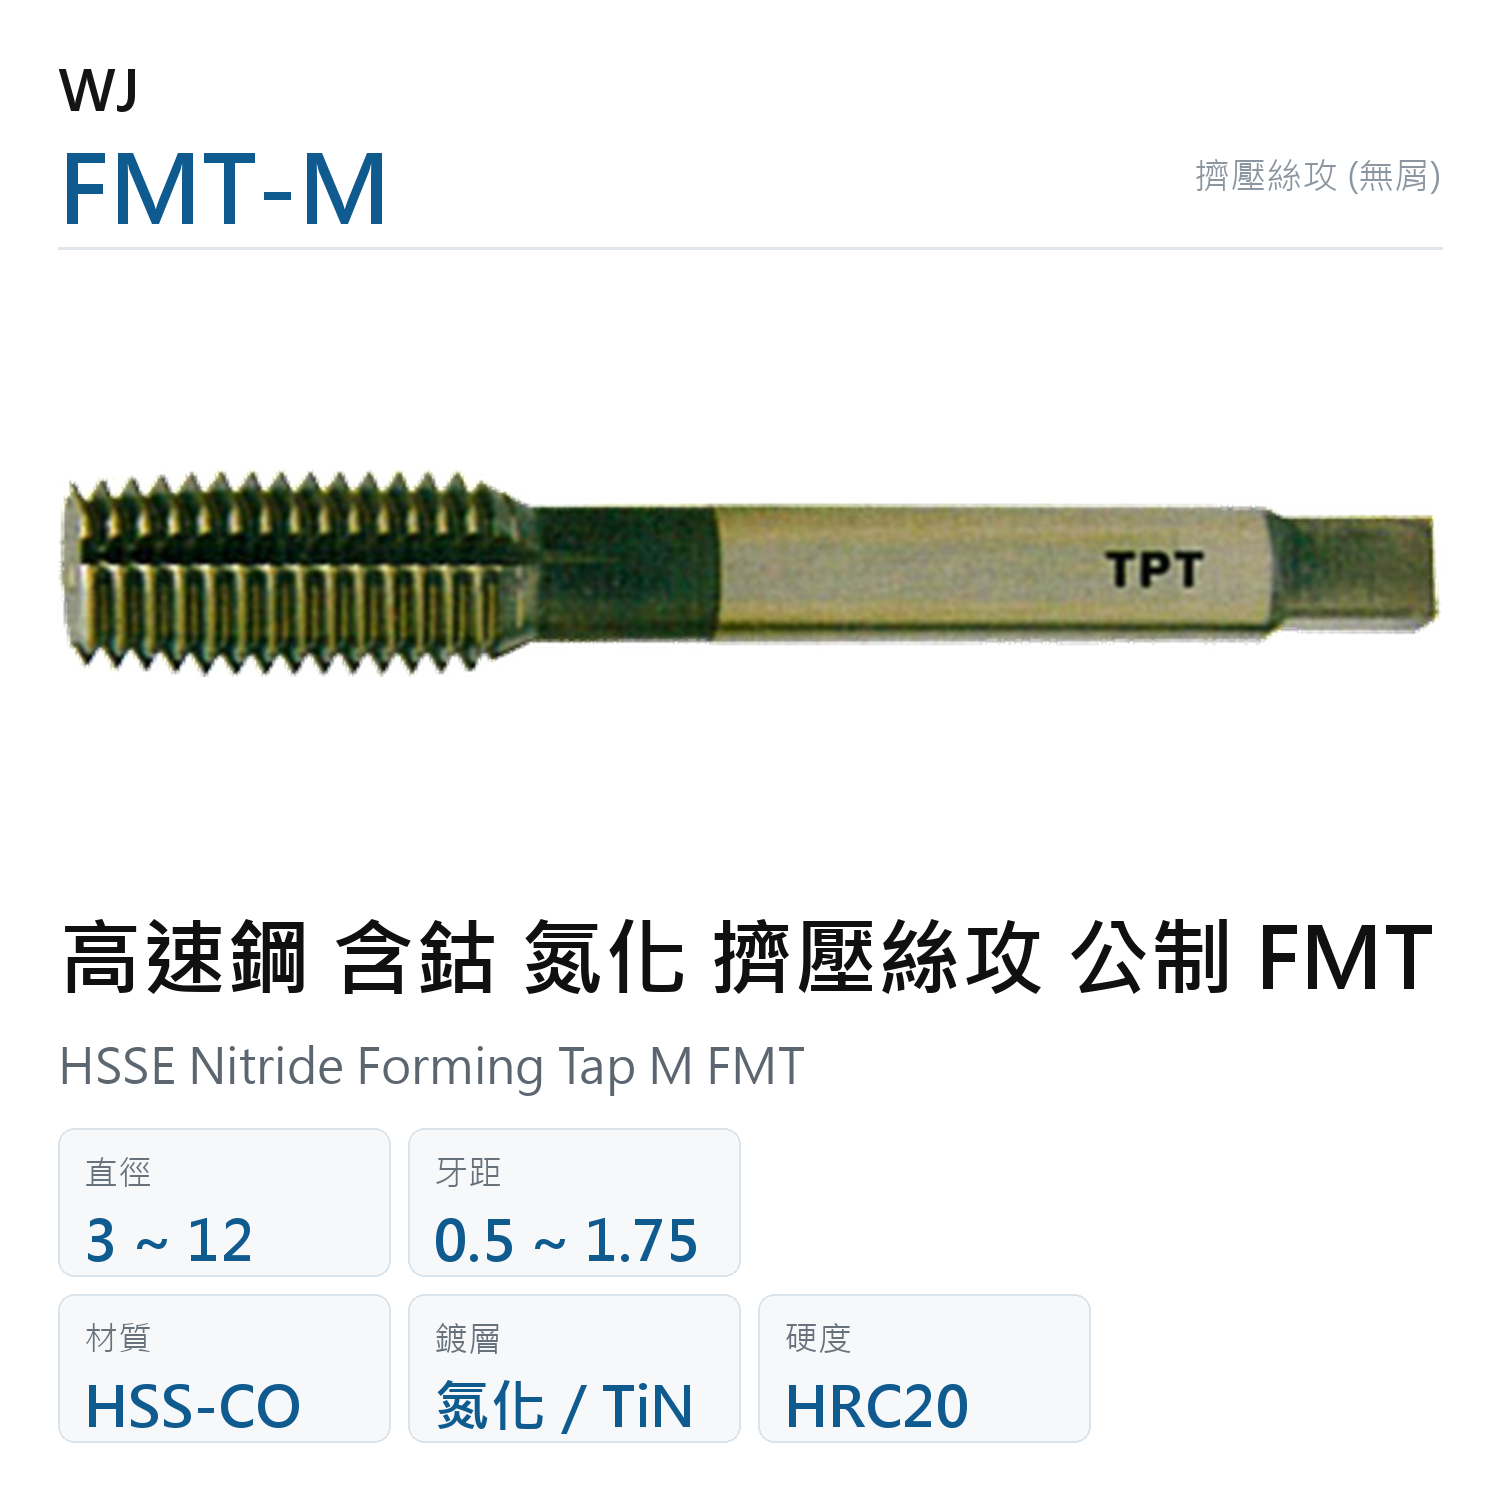
HSSE Nitride Forming Tap M FMT
The WJ HSSE Nitride Forming Tap M FMT does not cut and produces no chips - it forms the thread by cold extrusion, so chip evacuation simply does not arise, and the cold-worked thread comes out denser and stronger.
Specifications (20 items)
| Part No. | Standard | Dia. | Pitch | Flute L. | OAL | Shank Dia. | Tol. Class |
|---|---|---|---|---|---|---|---|
| ANJWJFMT-M3x0.5 | Metric M | 3 | 0.5 | 13 | 46 | 4 | F5 |
| ANJWJFMTT-M3x0.5 | Metric M | 3 | 0.5 | 13 | 46 | 4 | F5 |
| ANJWJFMT-M4x0.7 | Metric M | 4 | 0.7 | 10 | 52 | 5 | F6 |
| ANJWJFMTT-M4x0.7 | Metric M | 4 | 0.7 | 10 | 52 | 5 | F6 |
| ANJWJFMT-M5x0.8 | Metric M | 5 | 0.8 | 10 | 60 | 5.5 | F6 |
| ANJWJFMTT-M5x0.8 | Metric M | 5 | 0.8 | 10 | 60 | 5.5 | F6 |
| ANJWJFMT-M6x1 | Metric M | 6 | 1 | 10 | 62 | 6 | F7 |
| ANJWJFMTT-M6x1 | Metric M | 6 | 1 | 10 | 62 | 6 | F7 |
| ANJWJFMT-M8x1.25 | Metric M | 8 | 1.25 | 18 | 70 | 6.2 | F7 |
| ANJWJFMTT-M8x1.25 | Metric M | 8 | 1.25 | 18 | 70 | 6.2 | F7 |
| ANJWJFMT-M10x1.25 | Metric M | 10 | 1.25 | 19 | 75 | 7 | F7 |
| ANJWJFMTT-M10x1.25 | Metric M | 10 | 1.25 | 19 | 75 | 7 | F7 |
| ANJWJFMT-M10x1.5 | Metric M | 10 | 1.5 | 19 | 75 | 7 | F7 |
| ANJWJFMTT-M10x1.5 | Metric M | 10 | 1.5 | 19 | 75 | 7 | F7 |
| ANJWJFMT-M12x1.25 | Metric M | 12 | 1.25 | 23 | 80 | 8.5 | F10 |
| ANJWJFMTT-M12x1.25 | Metric M | 12 | 1.25 | 23 | 80 | 8.5 | F10 |
| ANJWJFMT-M12x1.5 | Metric M | 12 | 1.5 | 23 | 82 | 8.5 | F10 |
| ANJWJFMTT-M12x1.5 | Metric M | 12 | 1.5 | 23 | 82 | 8.5 | F10 |
| ANJWJFMT-M12x1.75 | Metric M | 12 | 1.75 | 23 | 82 | 8.5 | F10 |
| ANJWJFMTT-M12x1.75 | Metric M | 12 | 1.75 | 23 | 82 | 8.5 | F10 |
Specification Range
| Diameter | 3~12mm |
|---|---|
| Pitch | 0.5~1.75 |
| Flute length | 10~23mm |
| Overall length | 46~82mm |
| Shank diameter | 4~8.5mm |
Product Description
The WJ HSSE Nitride Forming Tap M FMT does not cut and produces no chips - it forms the thread by cold extrusion, so chip evacuation simply does not arise, and the cold-worked thread comes out denser and stronger. The principle itself is the difference: no chips means no chip problem, so it works in through and blind holes alike and nothing packs at the bottom. But forming needs a ductile material - brittle materials such as cast iron are unsuitable - and the pilot hole tolerance is far tighter than for a cutting tap; get it wrong and the tap will simply twist off; for longer tool life choose the TiN coated spec of this tap; for brittle materials such as cast iron use the standard spiral flute tap SFT; for a cutting tap in aluminium choose the aluminium-specific spiral flute tap SFT-AL. Substrate HSSE cobalt high-speed steel, nitrided, rated to HRC20. It cuts metric M threads, in sizes covering nominal size 3~12mm, pitch 0.5~1.75, 10 variants. Made in Taiwan. Are formed threads stronger? Yes - the material's grain flows around the thread form instead of being cut through, and cold working adds to it, so tensile strength is usually higher than a cut thread. What pilot size? Larger than for a cutting tap, and you must use a forming-tap pilot table rather than the cutting-tap figures. Typical applications: chipless tapping of aluminium alloys and low-carbon steel, parts where residual chips are unacceptable, and threads that must carry load.
Workpiece Materials & Hardness
- Steel (P)
- Stainless steel (M)
- Non-ferrous metals (N)
Max. workpiece hardness HRC20
Tags
- Chipless Forming
Related Resources
Can't find the size you need? Use the spec quick filter to search by category.