
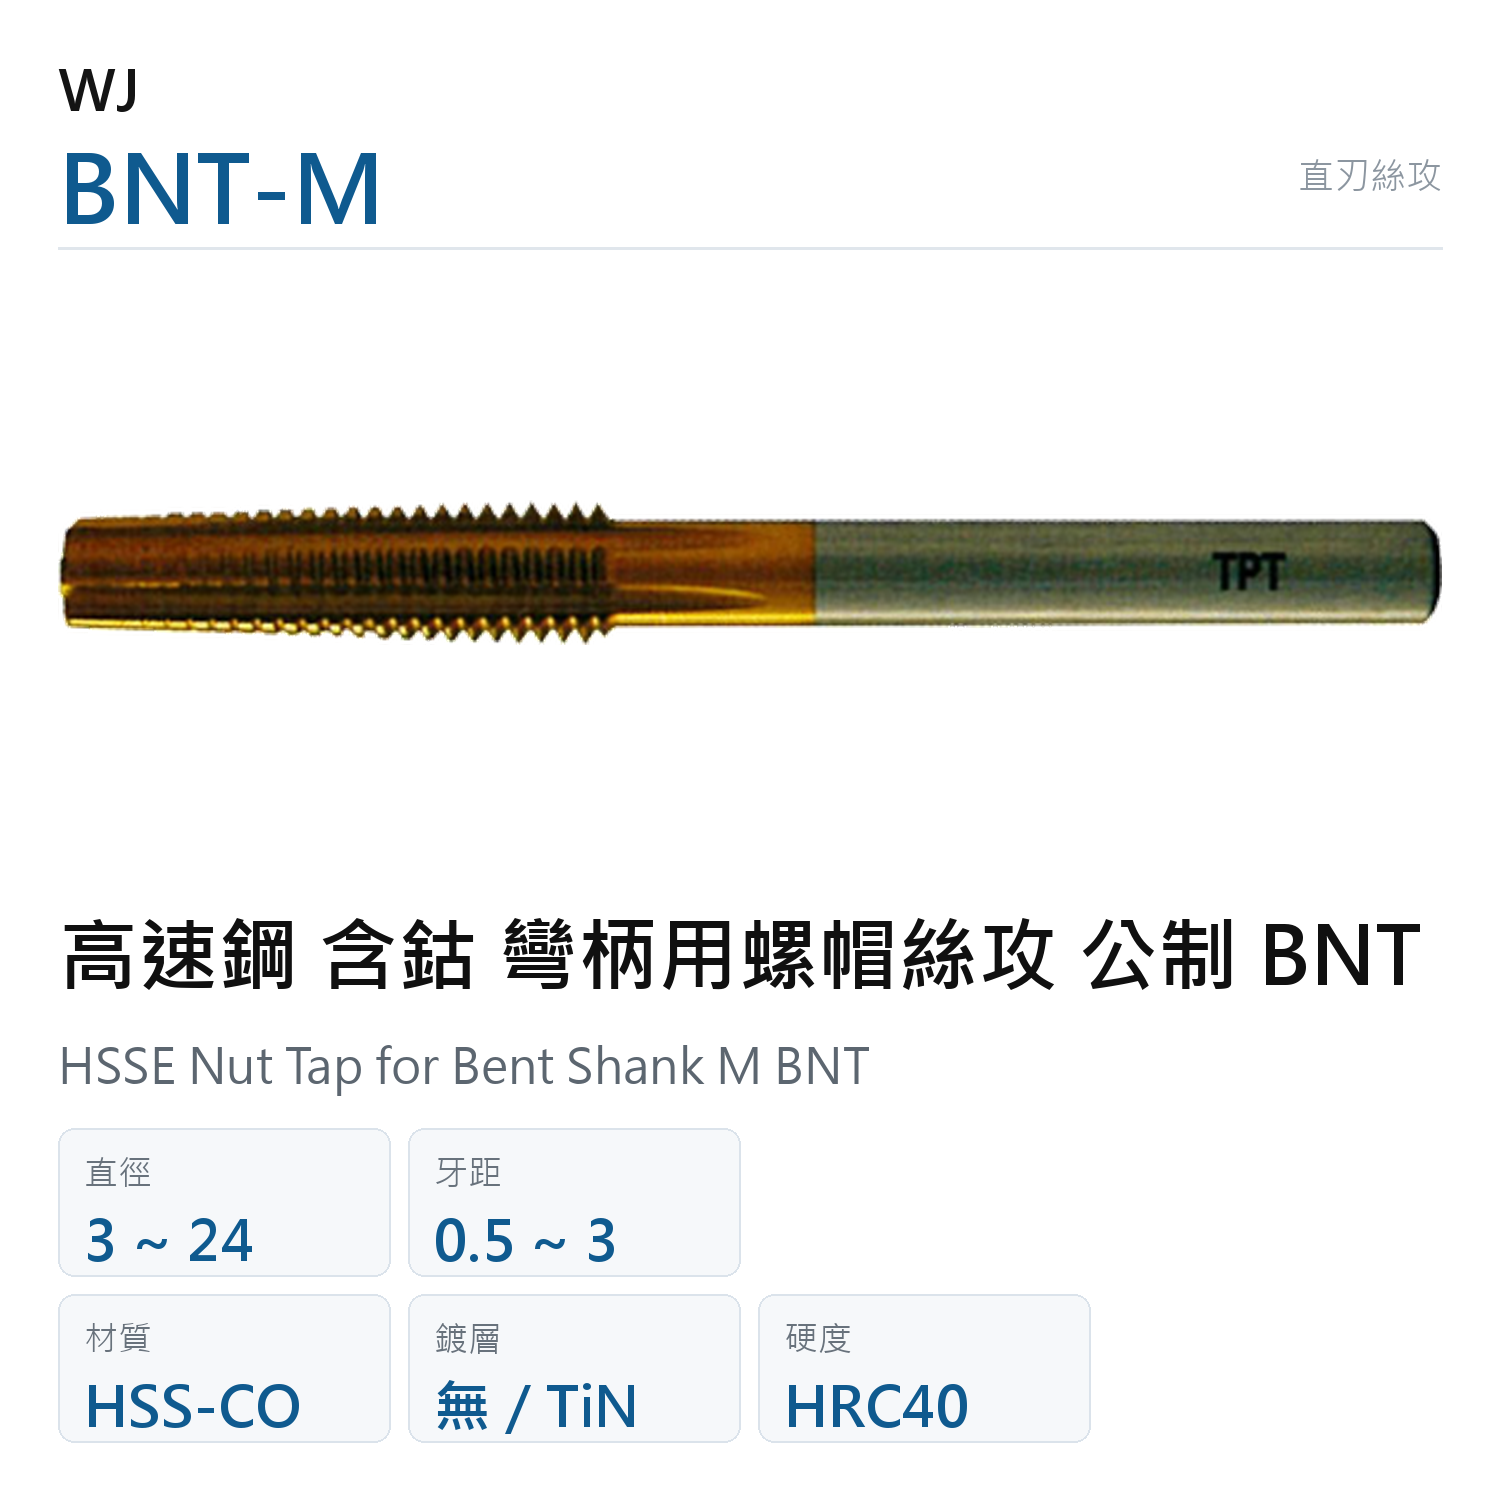
HSSE Nut Tap for Bent Shank M BNT
The WJ HSSE Nut Tap for Bent Shank M BNT is a straight flute tap with a bent shank, made for tapping nuts one after another.
Specifications (34 items)
| Part No. | Standard | Dia. | Pitch | Tol. Class |
|---|---|---|---|---|
| ANSWJBNT-M3x0.5 | Metric M | 3 | 0.5 | GH |
| ANSWJBNTT-M3x0.5 | Metric M | 3 | 0.5 | GH |
| ANSWJBNT-M3.5x0.6 | Metric M | 3.5 | 0.6 | GH |
| ANSWJBNTT-M3.5x0.6 | Metric M | 3.5 | 0.6 | GH |
| ANSWJBNT-M4x0.7 | Metric M | 4 | 0.7 | GH |
| ANSWJBNTT-M4x0.7 | Metric M | 4 | 0.7 | GH |
| ANSWJBNT-M5x0.8 | Metric M | 5 | 0.8 | GH |
| ANSWJBNTT-M5x0.8 | Metric M | 5 | 0.8 | GH |
| ANSWJBNT-M6x1 | Metric M | 6 | 1 | GH |
| ANSWJBNTT-M6x1 | Metric M | 6 | 1 | GH |
| ANSWJBNT-M8x1.25 | Metric M | 8 | 1.25 | GH |
| ANSWJBNTT-M8x1.25 | Metric M | 8 | 1.25 | GH |
| ANSWJBNT-M10x1.25 | Metric M | 10 | 1.25 | GH |
| ANSWJBNTT-M10x1.25 | Metric M | 10 | 1.25 | GH |
| ANSWJBNT-M10x1.5 | Metric M | 10 | 1.5 | GH |
| ANSWJBNTT-M10x1.5 | Metric M | 10 | 1.5 | GH |
| ANSWJBNT-M12x1.5 | Metric M | 12 | 1.5 | GH |
| ANSWJBNTT-M12x1.5 | Metric M | 12 | 1.5 | GH |
| ANSWJBNT-M12x1.75 | Metric M | 12 | 1.75 | GH |
| ANSWJBNTT-M12x1.75 | Metric M | 12 | 1.75 | GH |
| ANSWJBNT-M14x1.5 | Metric M | 14 | 1.5 | GH |
| ANSWJBNTT-M14x1.5 | Metric M | 14 | 1.5 | GH |
| ANSWJBNT-M14x2 | Metric M | 14 | 2 | GH |
| ANSWJBNTT-M14x2 | Metric M | 14 | 2 | GH |
| ANSWJBNT-M16x2 | Metric M | 16 | 2 | GH |
| ANSWJBNTT-M16x2 | Metric M | 16 | 2 | GH |
| ANSWJBNT-M18x2.5 | Metric M | 18 | 2.5 | GH |
| ANSWJBNTT-M18x2.5 | Metric M | 18 | 2.5 | GH |
| ANSWJBNT-M20x2.5 | Metric M | 20 | 2.5 | GH |
| ANSWJBNTT-M20x2.5 | Metric M | 20 | 2.5 | GH |
| ANSWJBNT-M22x2.5 | Metric M | 22 | 2.5 | GH |
| ANSWJBNTT-M22x2.5 | Metric M | 22 | 2.5 | GH |
| ANSWJBNT-M24x3 | Metric M | 24 | 3 | GH |
| ANSWJBNTT-M24x3 | Metric M | 24 | 3 | GH |
Specification Range
| Diameter | 3~24mm |
|---|---|
| Pitch | 0.5~3 |
Product Description
The WJ HSSE Nut Tap for Bent Shank M BNT is a straight flute tap with a bent shank, made for tapping nuts one after another. Each finished nut slides up onto the shank and stacks there, so the tap is never reversed out between parts - the fastest way to produce nuts in volume. The only difference from the hand tap HT is the shank: an HT must be reversed out after every hole, while the BNT lets the workpiece leave by itself. A TiN-coated version of the same tap is also offered as the other surface finish. The uncoated version keeps the price down and is enough for ordinary carbon steel and cast iron; the substrate is cobalt-bearing HSSE, rated to HRC40, recommended for carbon and alloy steels, stainless steel, cast iron, aluminium, copper and other non-ferrous metals. It cuts metric M threads, in sizes covering 3~24mm, 17 variants, thread tolerance GH. Made in Taiwan. Why a bent shank? A straight tap has to be withdrawn after every single nut, whereas a bent shank lets a dozen or more accumulate in one continuous run. What to watch? The bent section cannot be gripped in a chuck - a nut-tapping machine or hand wrench is required - and the nuts must be removed once they build up, or their weight will affect concentricity. For ordinary hand tapping see the hand tap HT; for deep holes the long shank LHT; for machine tapping the spiral flute SFT in blind holes and the spiral point POT in through holes. Typical applications: continuous tapping of nuts and nut-like parts, and thread production lines in the hardware trade. The same family also includes the hand tap HT (nominal diameter 2.6~48mm, rated to HRC30); use HT for ordinary hand tapping and single parts. Choose BNT (nominal diameter 3~24mm, cobalt, rated to HRC40) only for continuous nut tapping where the finished nuts slide off the bent shank. For deep holes switch to the long shank hand tap LHT (nominal diameter 3~20mm, overall length 100~150mm).
Workpiece Materials & Hardness
- Steel (P)
- Stainless steel (M)
- Cast iron (K)
- Non-ferrous metals (N)
Max. workpiece hardness HRC40
Related Resources
Can't find the size you need? Use the spec quick filter to search by category.