
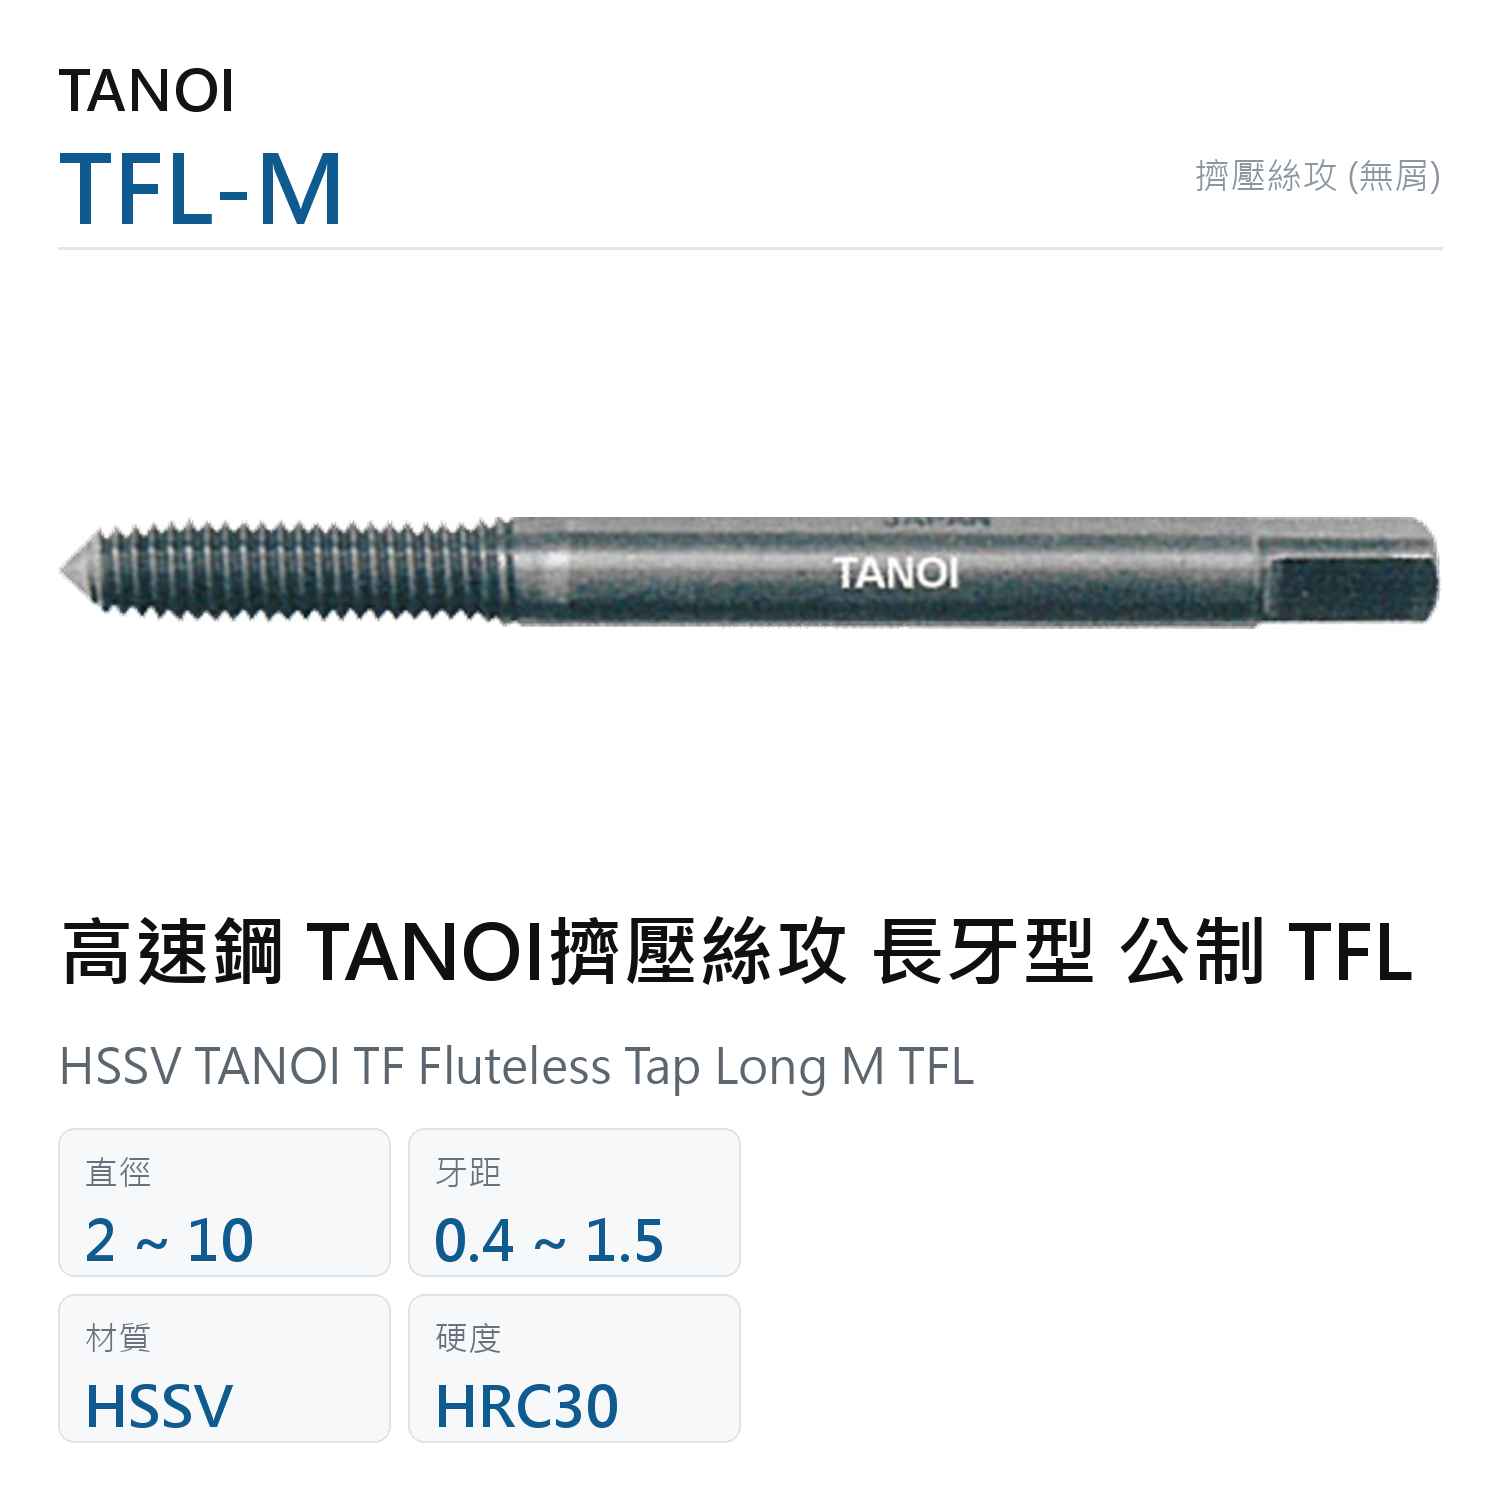
HSSV TANOI TF Fluteless Tap Long M TFL
The HSSV TANOI TF Fluteless Tap Long M TFL is TANOI's long-thread forming tap - no cutting, no chips; the thread is formed by pushing the material into shape.
Specifications (11 items)
| Part No. | Standard | Dia. | Pitch | Flute L. | OAL | Shank Dia. |
|---|---|---|---|---|---|---|
| ANJWJTFL-M2.0x0.4 | Metric M | 2 | 0.4 | 15 | 40 | 3 |
| ANJWJTFL-M2.5x0.45 | Metric M | 2.5 | 0.45 | 16 | 44 | 3 |
| ANJWJTFL-M2.6x0.45 | Metric M | 2.6 | 0.45 | 16 | 44 | 3 |
| ANJWJTFL-M3.0x0.5 | Metric M | 3 | 0.5 | 18 | 46 | 4 |
| ANJWJTFL-M3.5x0.6 | Metric M | 3.5 | 0.6 | 18 | 48 | 4 |
| ANJWJTFL-M4.0x0.7 | Metric M | 4 | 0.7 | 20 | 52 | 5 |
| ANJWJTFL-M5.0x0.8 | Metric M | 5 | 0.8 | 22 | 60 | 5.5 |
| ANJWJTFL-M6.0x1 | Metric M | 6 | 1 | 24 | 62 | 6 |
| ANJWJTFL-M8.0x1.25 | Metric M | 8 | 1.25 | 30 | 70 | 6.2 |
| ANJWJTFL-M10x1.25 | Metric M | 10 | 1.25 | 32 | 75 | 7 |
| ANJWJTFL-M10x1.5 | Metric M | 10 | 1.5 | 32 | 75 | 7 |
Specification Range
| Diameter | 2~10mm |
|---|---|
| Pitch | 0.4~1.5 |
| Flute length | 15~32mm |
| Overall length | 40~75mm |
| Shank diameter | 3~7mm |
Product Description
The HSSV TANOI TF Fluteless Tap Long M TFL is TANOI's long-thread forming tap - no cutting, no chips; the thread is formed by pushing the material into shape. Forming length and size band separate it from the short-thread TFS: a longer forming section gives greater thread engagement, which suits joints needing more clamping strength. Substrate HSSV high-vanadium steel rated to HRC30. Forming needs a ductile material - brittle materials such as cast iron are unsuitable - and the pilot hole tolerance is tighter than for a cutting tap; for small threads or thin parts choose the TANOI forming tap, short thread type TFS; for the Taiwan-made equivalent choose the nitrided forming tap FMT; for brittle materials such as cast iron use the TANOI standard spiral flute tap SP. Substrate HSSV high-vanadium high-speed steel, uncoated, rated to HRC30. It cuts metric M threads, in sizes covering nominal size 2~10mm, pitch 0.4~1.5, 11 variants. Made in Japan. Are formed threads stronger? Yes - the grain flows around the thread form instead of being cut through, and cold working adds to it, so tensile strength is usually higher. What pilot size? Use a forming-tap pilot table, not cutting-tap figures. Typical applications: chipless tapping of aluminium alloys and low-carbon steel, threads needing clamping strength, and lines standardised on Japanese tooling.
Workpiece Materials & Hardness
- Steel (P)
- Stainless steel (M)
- Non-ferrous metals (N)
Max. workpiece hardness HRC30
Tags
- Chipless Forming
Related Resources
Can't find the size you need? Use the spec quick filter to search by category.