
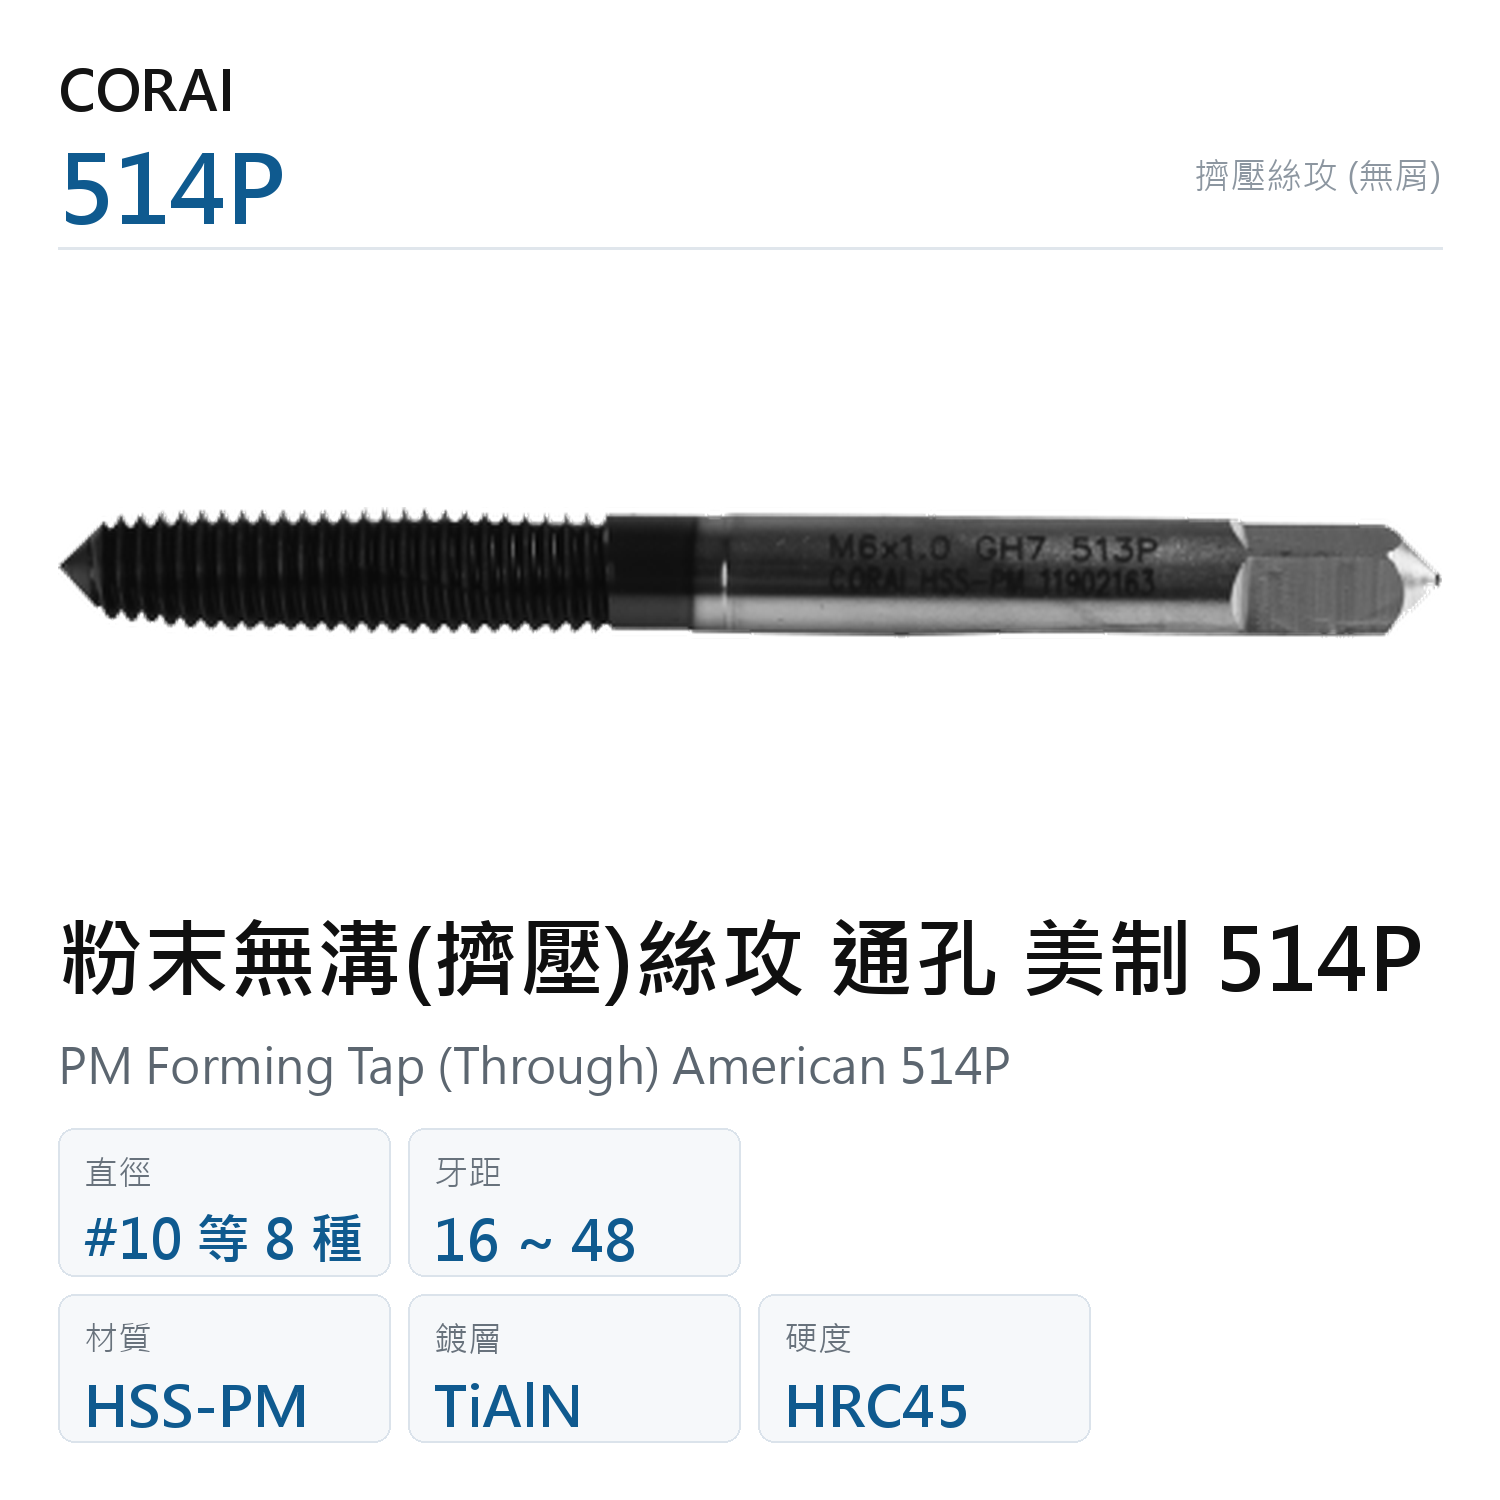
PM Forming Tap (Through) American 514P
Made of powder-metallurgy HSS, the 514P is a French-brand forming (fluteless) tap for through holes, covering both UNC and UNF threads, ideal for chipless thread forming — produces stronger threads with continuous grain, ideal for ductile m
Specifications (13 items)
| Part No. | Standard | Dia. | Pitch | Flute L. | OAL | Shank Dia. | Square | Tol. Class |
|---|---|---|---|---|---|---|---|---|
| ANJCD514PTA_UNC#4-40 | UNC | #4 | 40 | 9.5 | 44 | 3 | 2.5 | GH6 |
| ANJCD514PUNF#4-48-TA | UNF | #4 | 48 | 9.5 | 44 | 3 | 2.5 | GH6 |
| ANJCD514PTA_UNC#6-32 | UNC | #6 | 32 | 13 | 48 | 4 | 3.2 | GH7 |
| ANJCD514PTA_UNC#8-32 | UNC | #8 | 32 | 13 | 52 | 5 | 4 | GH7 |
| ANJCD514PTA_UNC#10-24 | UNC | #10 | 24 | 16 | 60 | 5.5 | 4.5 | GH7 |
| ANJCD514PUNF#10-32-TA | UNF | #10 | 32 | 16 | 60 | 5.5 | 4.5 | GH7 |
| ANJCD514PTA_UNC#12-24 | UNC | #12 | 24 | 16 | 60 | 5.5 | 4.5 | GH7 |
| ANJCD514PTA_UNC1/4-20 | UNC | 1/4 | 20 | 19 | 62 | 6 | 4.5 | GH8 |
| ANJCD514PUNF1/4-28-TA | UNF | 1/4 | 28 | 19 | 62 | 6 | 4.5 | GH8 |
| ANJCD514PTA_UNC5/16-18 | UNC | 5/16 | 18 | 22 | 70 | 6.1 | 5 | GH8 |
| ANJCD514PUNF5/16-24-TA | UNF | 5/16 | 24 | 22 | 70 | 6.1 | 5 | GH8 |
| ANJCD514PTA_UNC3/8-16 | UNC | 3/8 | 16 | 24 | 75 | 7 | 5.5 | GH8 |
| ANJCD514PUNF3/8-24-TA | UNF | 3/8 | 24 | 24 | 75 | 7 | 5.5 | GH8 |
Specification Range
| Diameter | #4~3/8 |
|---|---|
| Pitch | 16~48 |
| Flute length | 9.5~24 |
| Overall length | 44~75 |
| Shank diameter | 3~7 |
Product Description
Made of powder-metallurgy HSS, the 514P is a French-brand forming (fluteless) tap for through holes, covering both UNC and UNF threads, ideal for chipless thread forming — produces stronger threads with continuous grain, ideal for ductile materials. Available in 13 sizes (UNC and UNF #4~3/8, 16~48 TPI, overall length 44~75mm, shank dia 3~7mm). A TiAlN coating offers high-temperature wear resistance. Suitable for machining carbon and alloy steel, stainless steel, workpiece hardness up to HRC45. French brand, consistent quality. 514B is the blind-hole twin on the same catalogue table, also covering UNC and UNF; the difference is the lead - use this 514P for through holes and 514B for blind holes, and the smallest UNC #2-56 is available only as 514B. The metric counterparts are 513P (through) and 513B (blind); for larger sizes or heat-resistant alloys choose 5KC.
Workpiece Materials & Hardness
- Steel (P)
- Stainless steel (M)
Max. workpiece hardness HRC45
Tags
- Fine Thread
Related Resources
Can't find the size you need? Use the spec quick filter to search by category.