Imperial Thread Tolerance Chart|Whitworth, Pipe & P-Class
The imperial thread tolerance chart covers Whitworth (BSW), Unified (UNC/UNF), pipe threads (PF/PT/G/Pg) and STI, controlling major, pitch and minor diameters and their tolerance ranges. Using P-class (P1–P4) or µm tolerances secures thread-fit accuracy and interchangeability. Machining, pipe sealing, automotive and electrical-conduit systems each need the right standard and grade to balance machining stability and assembly quality.
1. What the Chart Is For
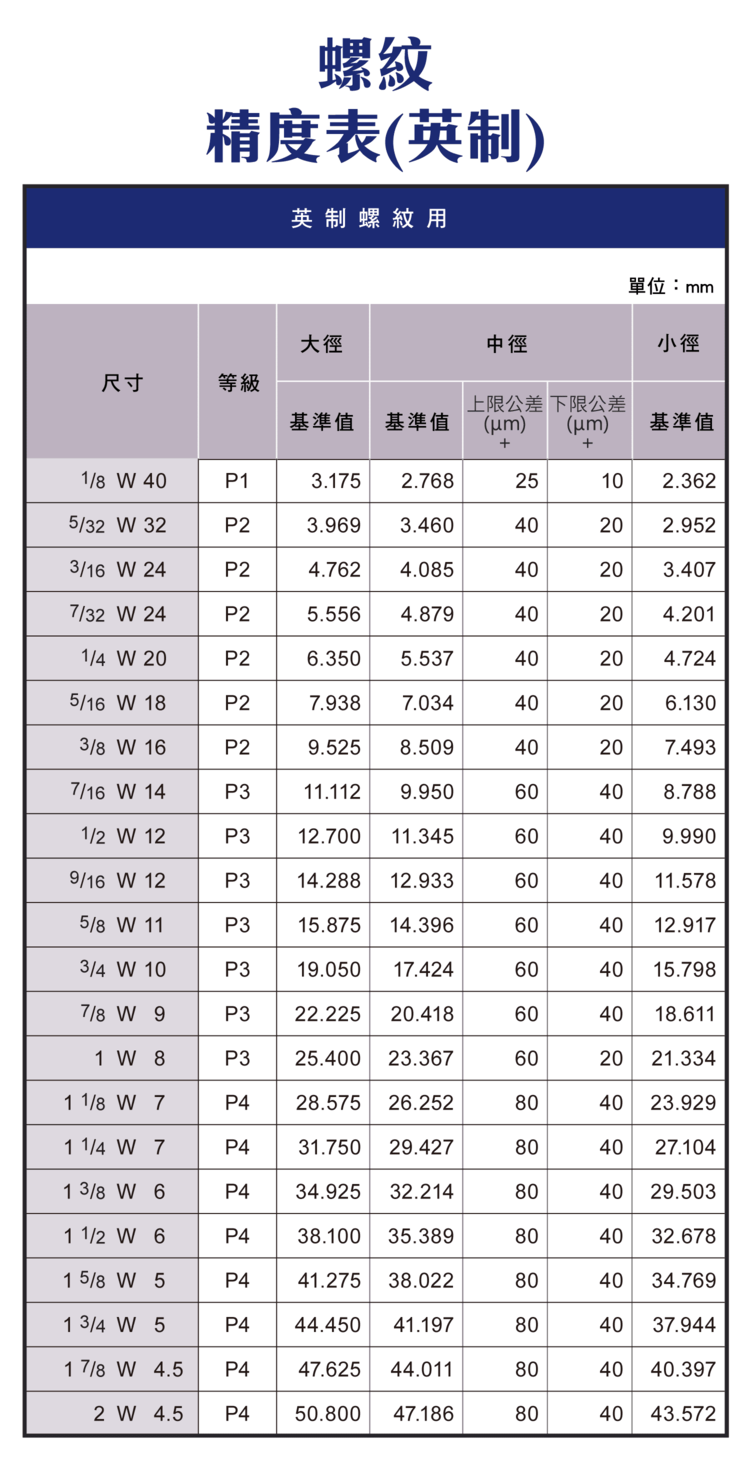
The imperial thread chart controls thread sizes (major/pitch/minor), defines tolerance ranges (µm) and secures part interchangeability, widely used in CNC machining, assembly, pipe sealing, and the electrical and automotive industries. The pitch diameter is the most critical size for fit accuracy and tightness.
2. Common Imperial / Pipe Thread Standards
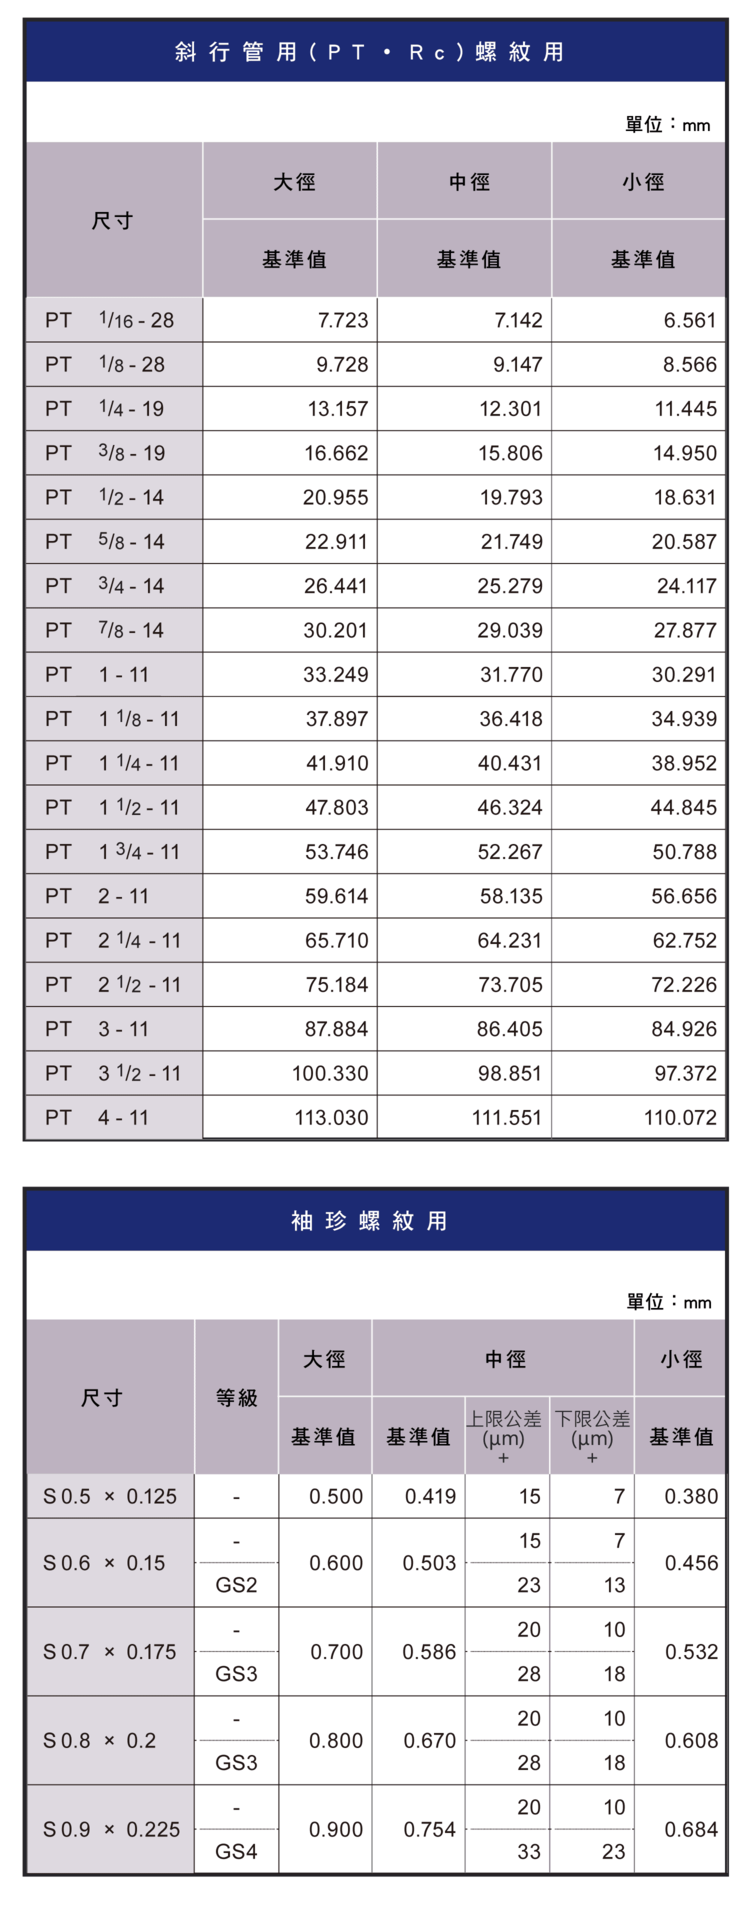
| Standard | Form / angle | Main use |
|---|---|---|
| BSW (Whitworth) | 55° rounded | Traditional British standard; legacy machinery |
| UNC / UNF (Unified) | 60° V | US coarse/fine; general machinery |
| PF / G (parallel pipe) | 55° pipe (parallel) | Pipe connection and sealing (parallel) |
| PT / R (taper pipe) | 55° pipe (taper) | Pipe sealing (taper, interference seal) |
| Pg | Electrical conduit thread | Conduit and fittings |
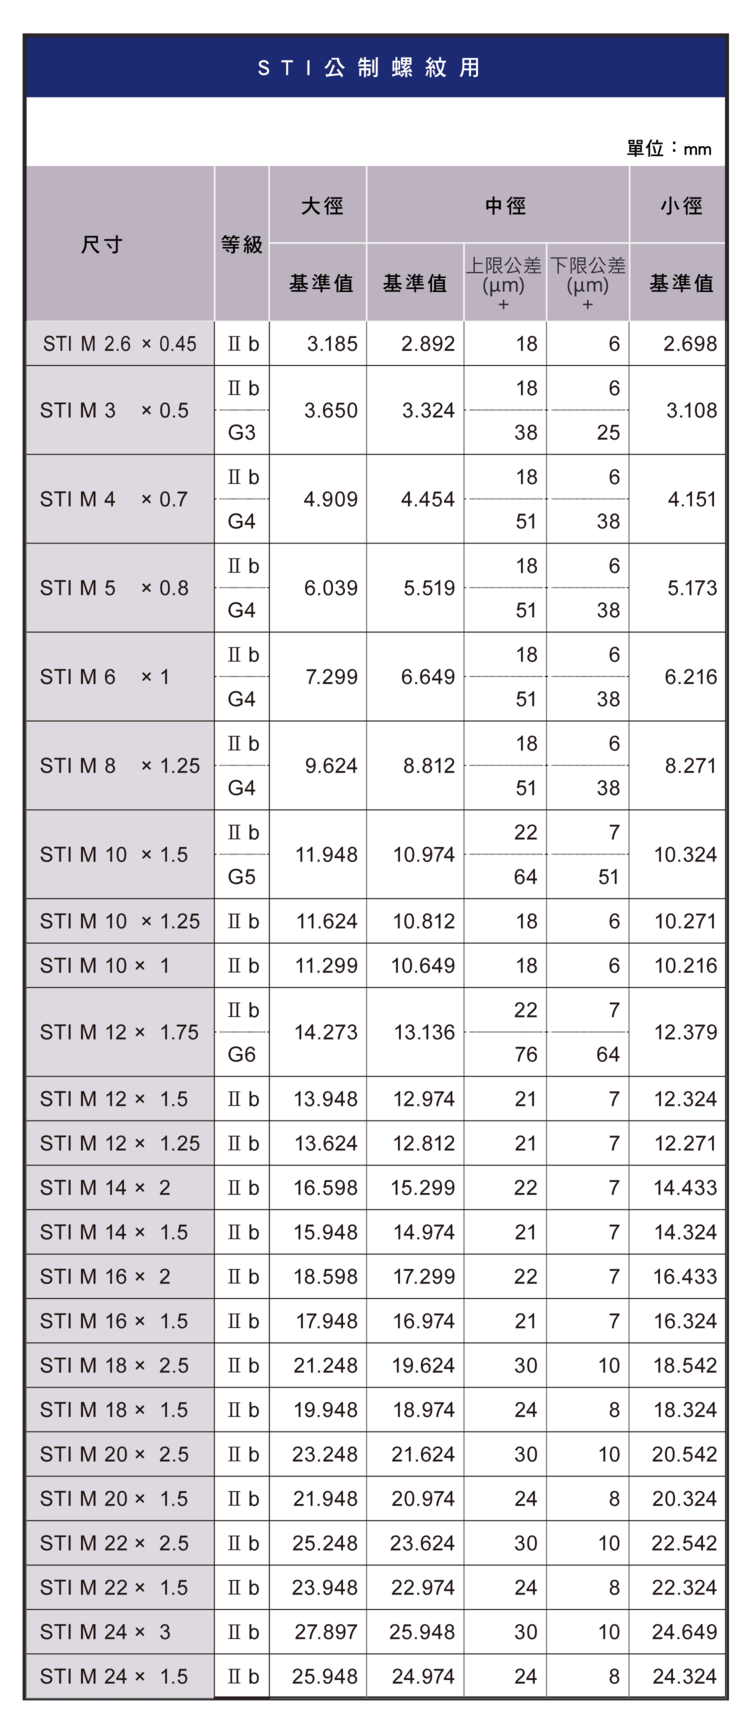
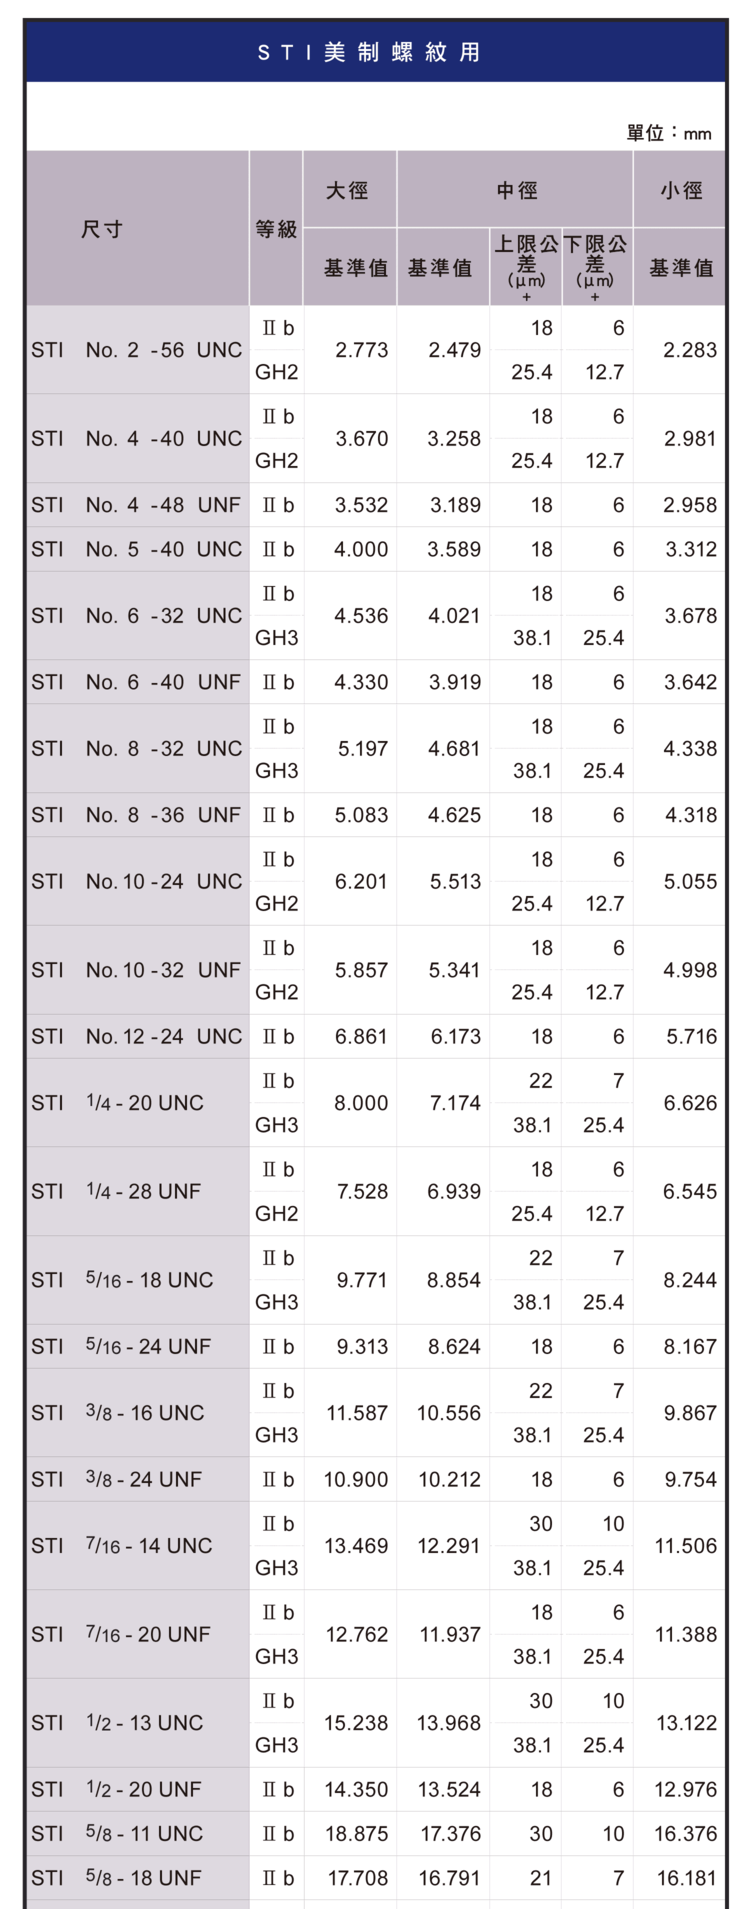
| STI | Insert thread (oversize internal) | Thread inserts; repair or reinforce holes |
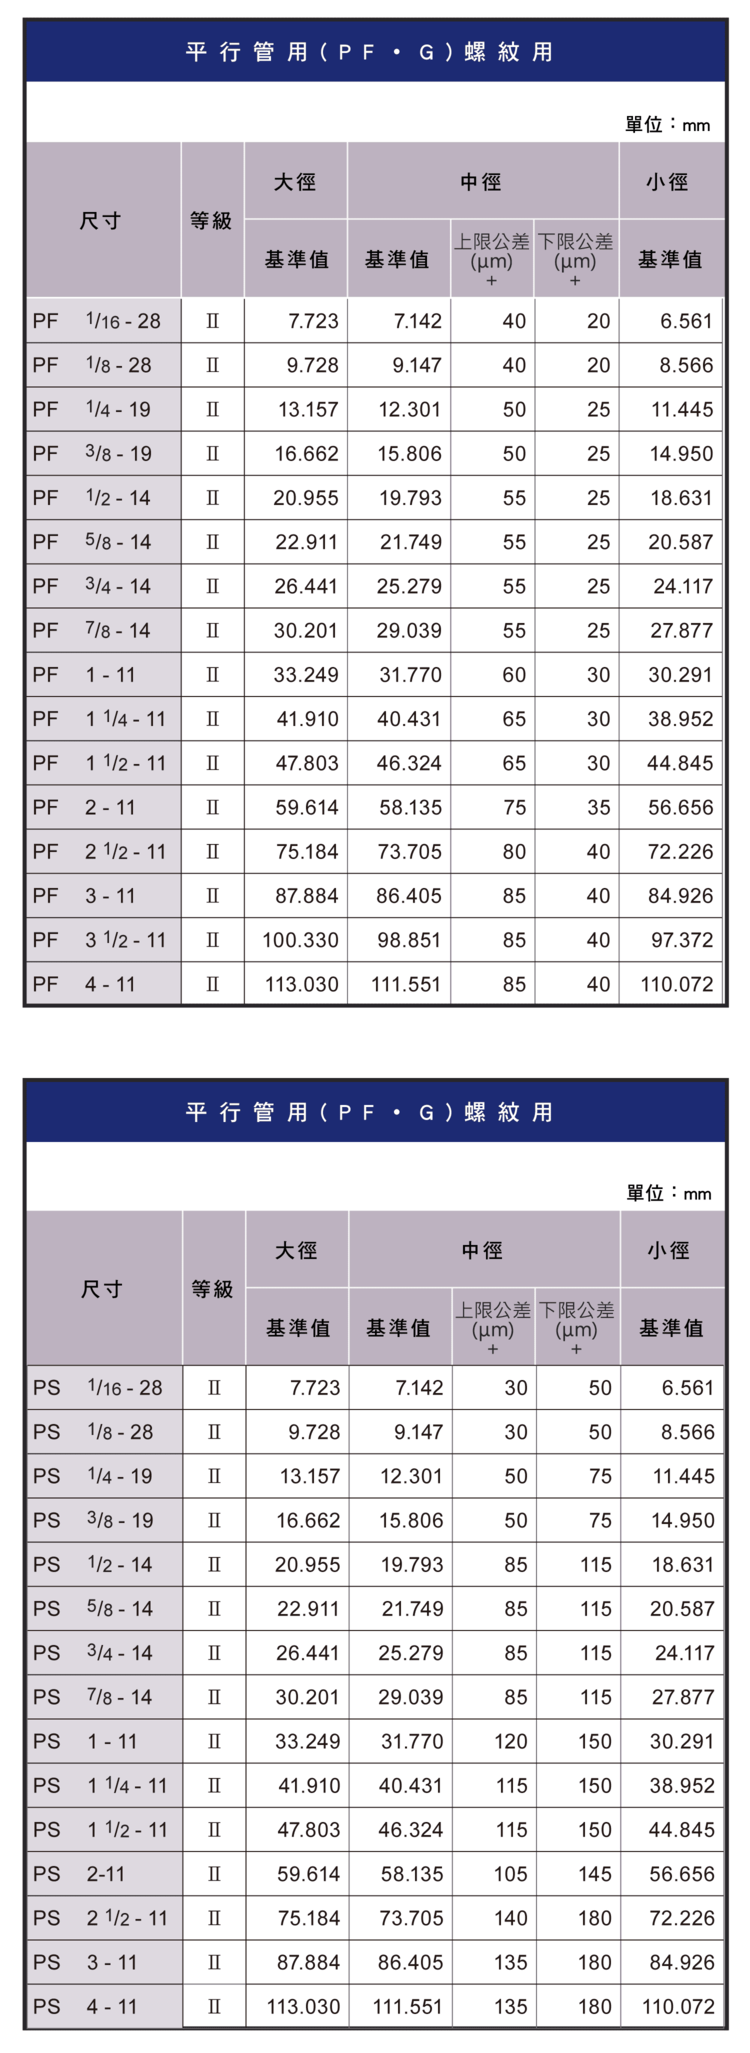
※ For each standard's full major/pitch/minor diameters and tolerances, refer to the original chart images below.
3. The Three Diameters
| Diameter | Description |
|---|---|
| Major | Largest thread diameter |
| Pitch | Most critical size for fit |
| Minor | Root diameter; close to the pilot-hole size |
4. P-Class Precision Grades
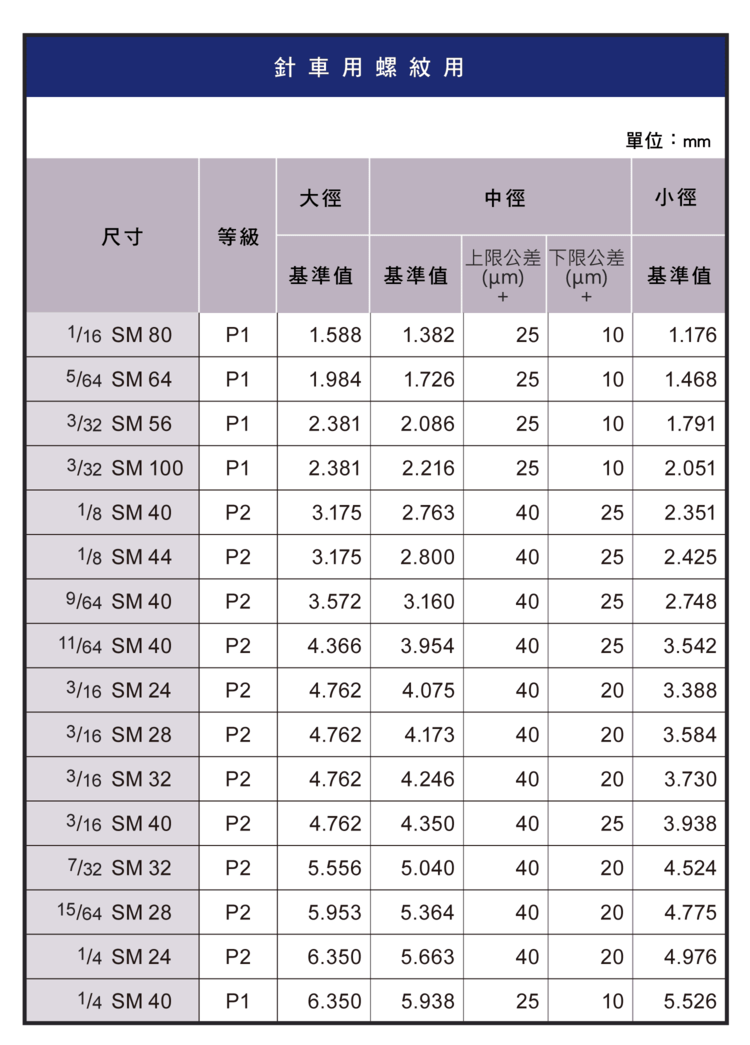
Of the tables on this page, only the Whitworth (W) table and the sewing-machine (SM) table use P1–P4; the BSW table has no grade, and the pipe-thread (PF/G, PT/R) and STI tables use other grade codes (such as II, IIb, G4–G6 or GH3).
| Grade | Zone position |
|---|---|
| P1 | Lowest: smallest thread, tightest fit |
| P2 | One step up |
| P3 | Another step up |
| P4 | Highest: largest thread, loosest fit |
Trend: a higher number moves the zone up and loosens the fit; the width of each grade is set by diameter and pitch, not by the number. In the Whitworth table the P4 rows (1 1/8 in and up) are 40 μm wide because large, coarse threads fall into a wider tolerance type; for how the types are set, see Tap Thread Tolerance Guide.
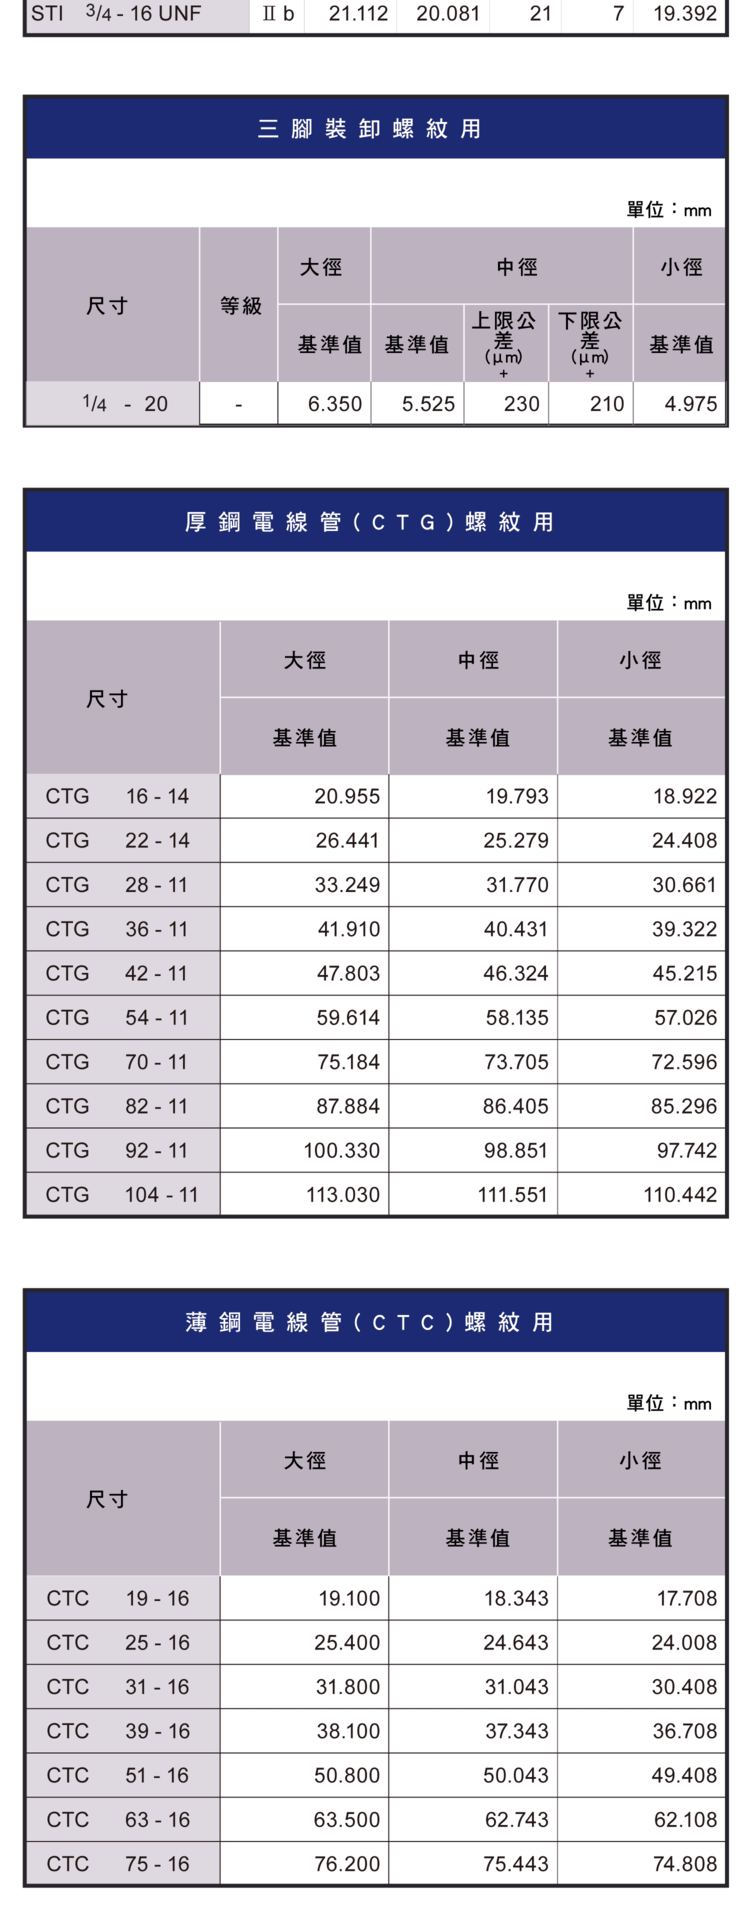
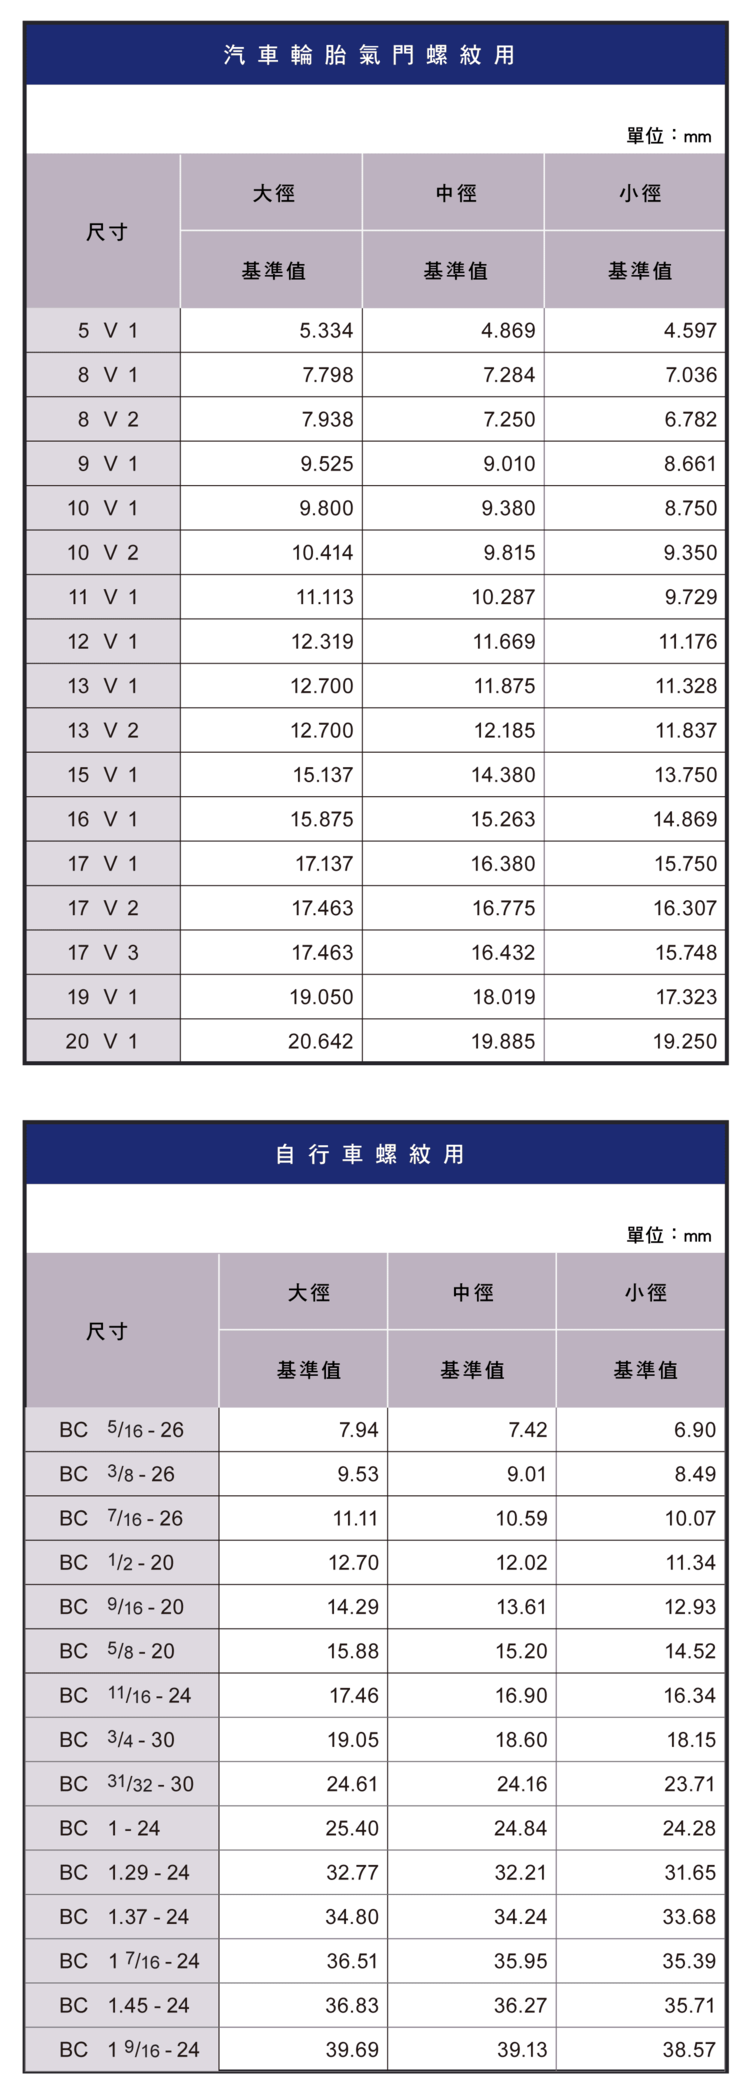
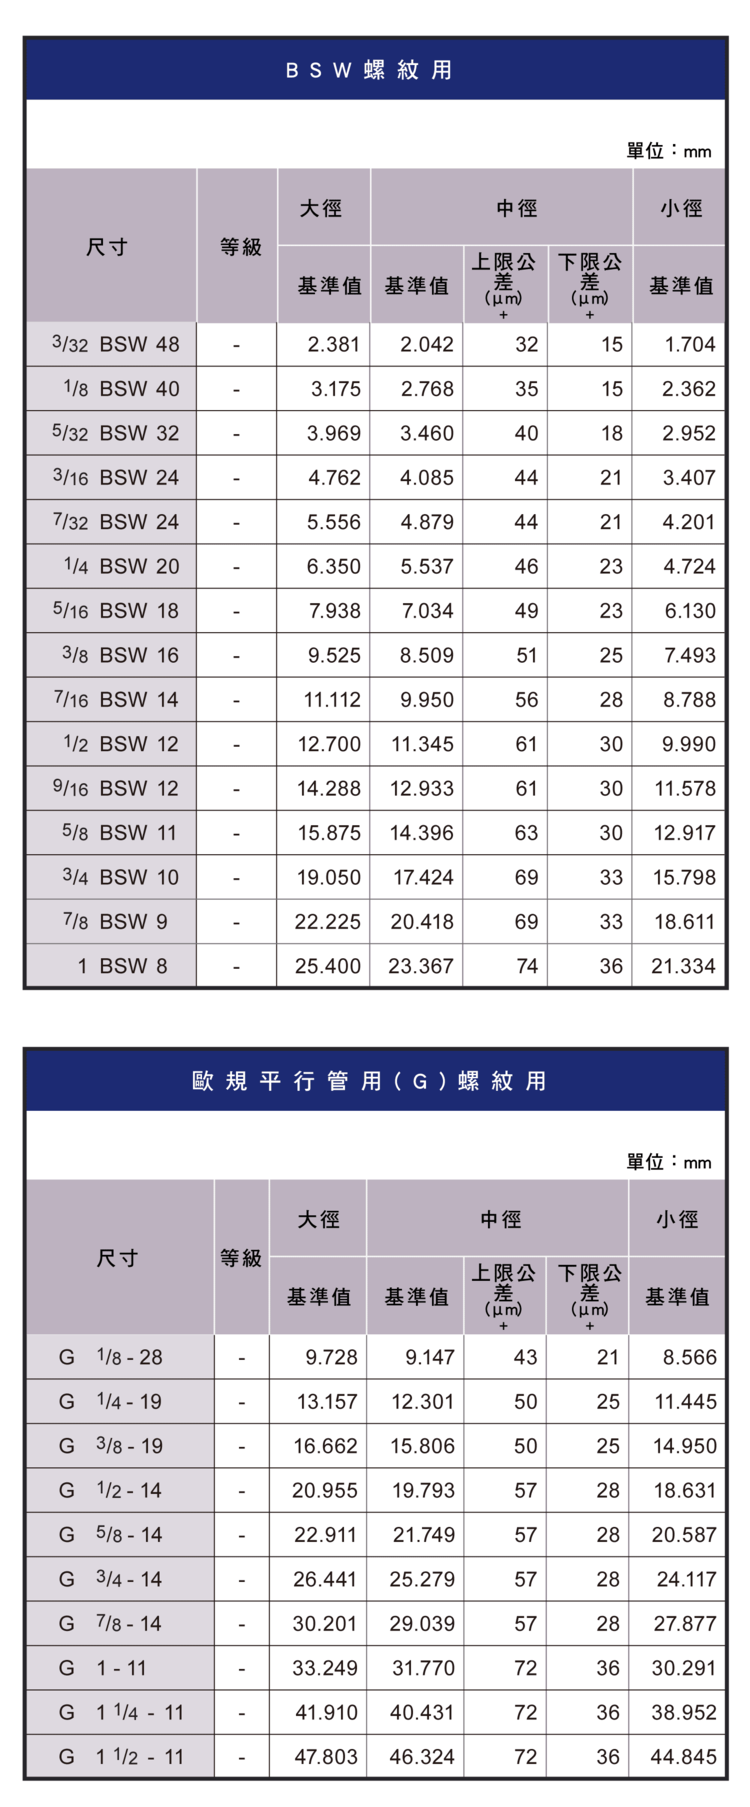
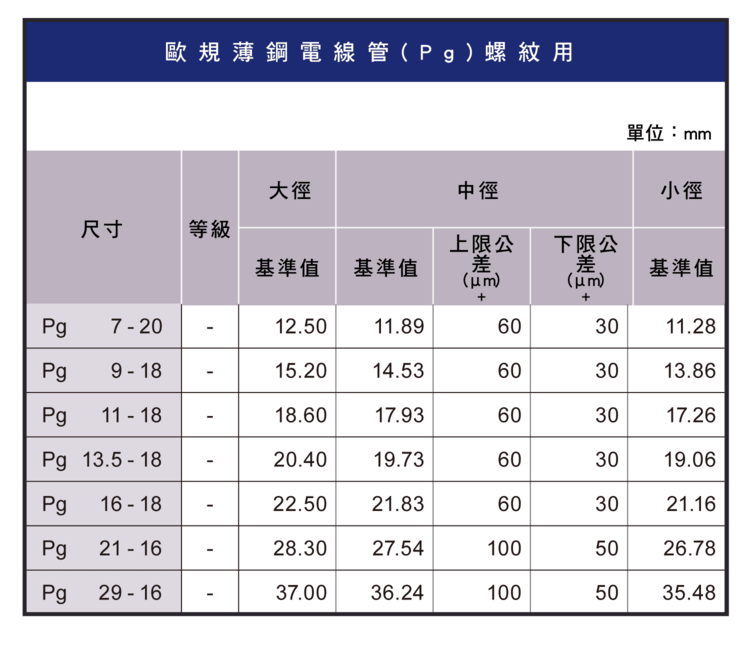
※ Full size and tolerance charts per standard above; values per the original tables.
5. Selection Tips
General machinery and structural parts mostly use UNC/UNF; pipe sealing chooses parallel (PF/G) or taper (PT/R); conduit systems use Pg; hole repair or reinforcement uses STI inserts. Pilot holes still follow each standard's minor diameter and pitch.
For metric and unified standards see the Metric Thread Tolerance Chart and Unified Thread Tolerance Chart; for pipe taps see the Pipe Tap Guide; for internal-thread tolerance see the Tap Thread Tolerance Guide.
FAQ
Q: BSW (Whitworth) vs UNC?
BSW is the British Whitworth standard with a 55° angle and rounded crest/root; UNC is the US unified thread with a 60° V form. Their forms and sizes differ and are not interchangeable — confirm the standard before use or inspection.
Q: Parallel (PF/G) or taper (PT/R) pipe thread?
Parallel pipe threads (PF/G) seal with a gasket or O-ring, good for removable fittings; taper pipe threads (PT/R) self-seal by flank interference, usually with sealing tape, for gas/liquid-tight piping.
Q: How to read P1–P4?
P-class grades the tap pitch diameter: a higher number moves the tolerance zone up, cutting a larger thread with a looser fit; the zone width is set by diameter and pitch, not by the number. On this page only the Whitworth (W) and sewing-machine (SM) tables use P grades.
Q: What is an STI thread?
STI is an oversize internal thread for fitting thread inserts, used to repair stripped holes or reinforce threads in soft materials like aluminium and magnesium. Its pilot hole differs from a standard thread and follows the STI spec.
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.
Published: 2026-03-23 | Last updated: 2026-10-31