
Unified Thread Tolerance Chart|UNC/UNF/UNEF with 2B & GH
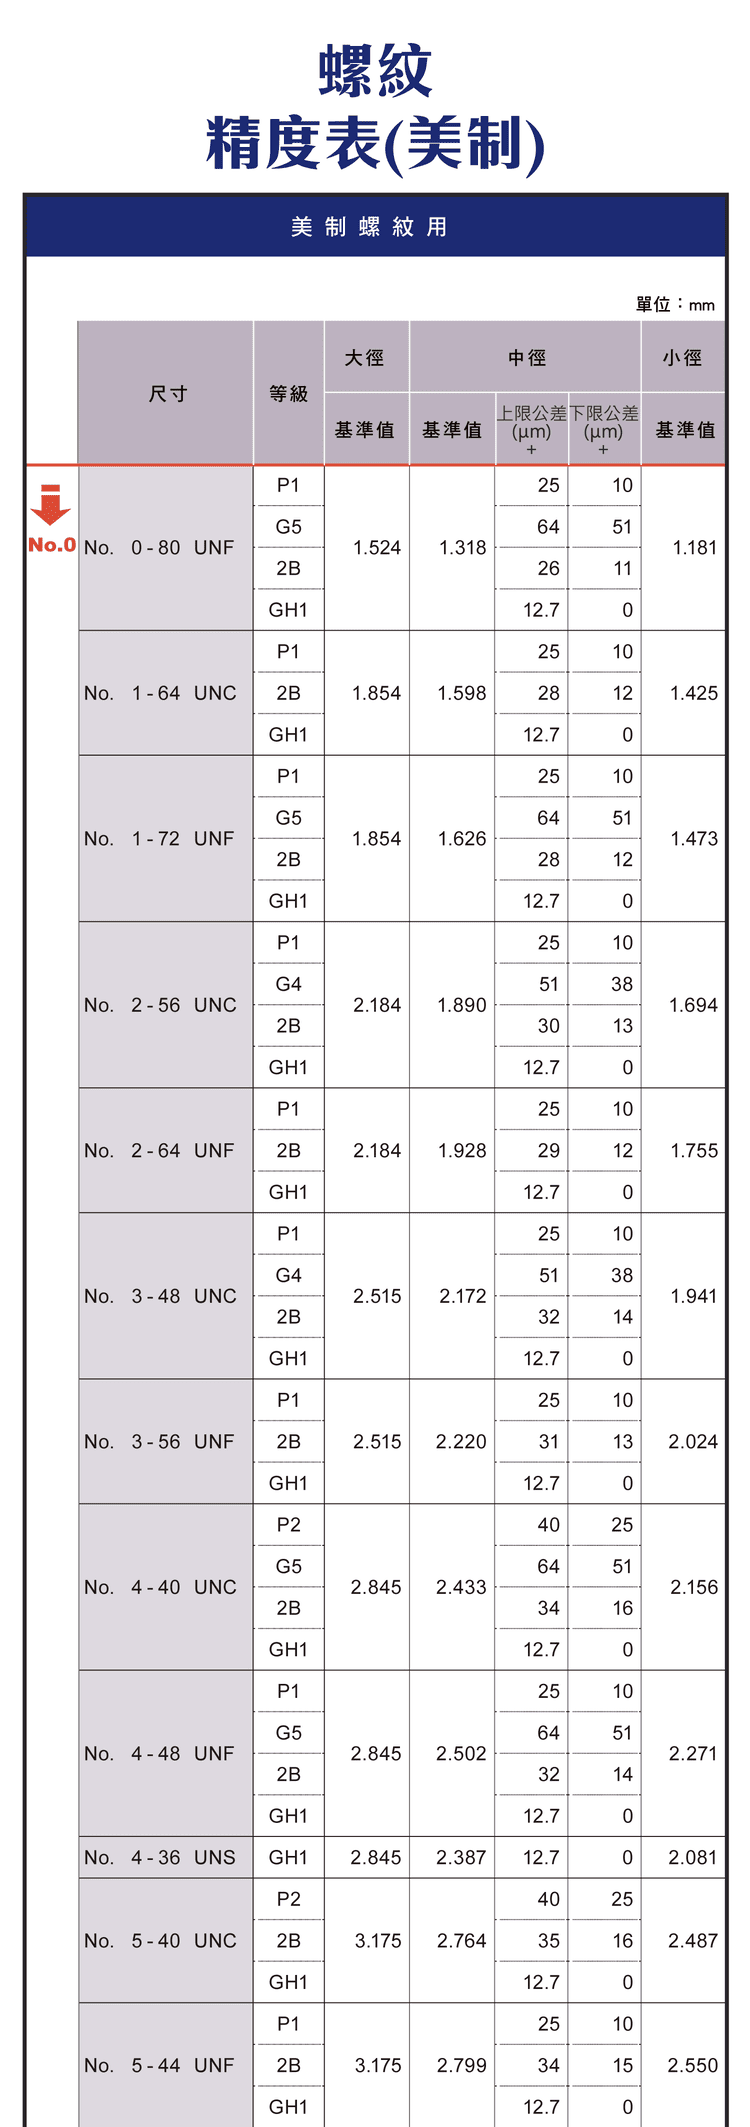
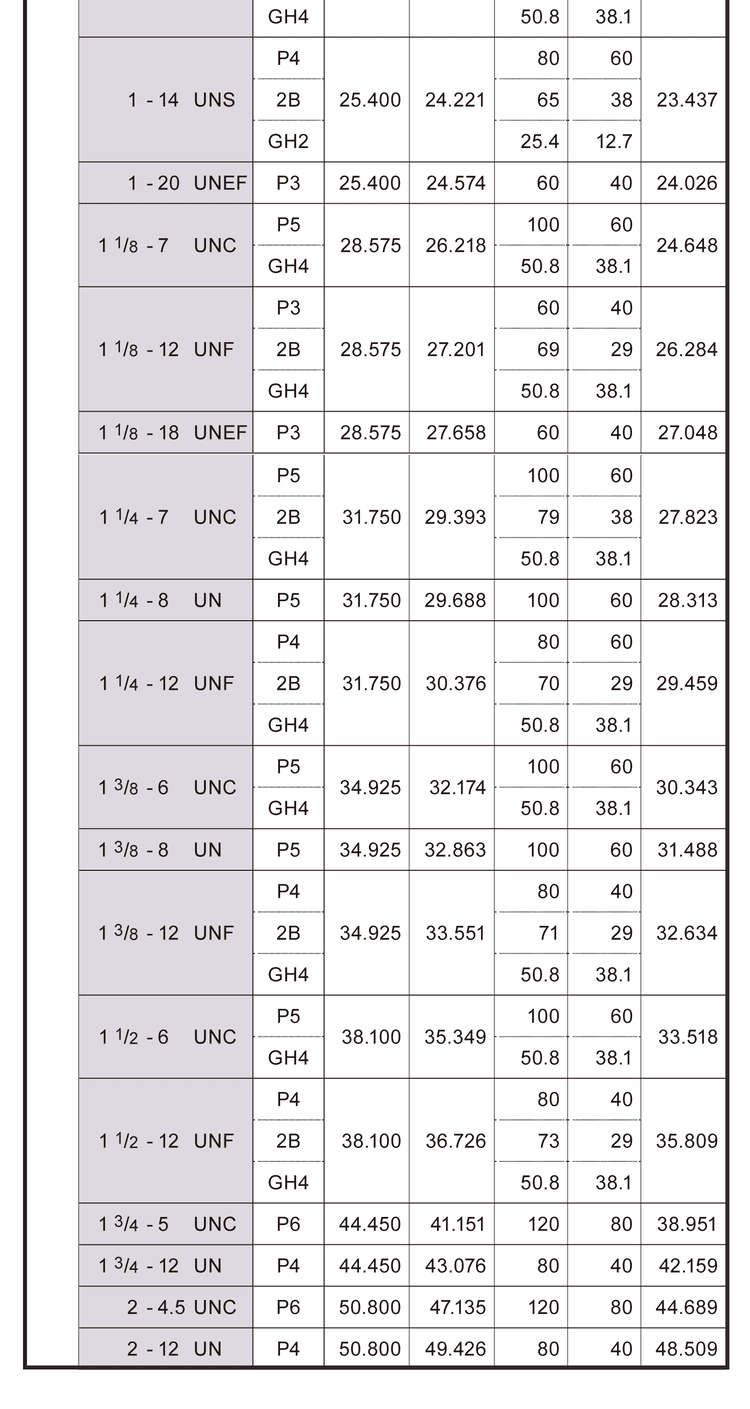
The Unified (US) thread chart (UNC / UNF / UNEF / UNS) gives full size data from No.0 up to 2 inches and above — major, pitch and minor diameters — with tolerance grades such as 1A/2A/3A, 2B and GH. Use it for tap-drill (pilot-hole) selection, thread-fit design and quality inspection, improving CNC accuracy and assembly stability across machinery, aerospace and automotive parts.
1. Types of Unified Thread
| Type | Traits and use |
|---|---|
| UNC (coarse) | High strength, damage-resistant; general machinery and structural parts |
| UNF (fine) | Higher locking accuracy; precision parts |
| UNEF (extra fine) | High precision and high clamping force |
| UNS (special) | Special pitch, custom applications |
2. Basic Sizes for Common UNC Threads
The table gives basic sizes for common UNC threads (pitch dia = major − 0.6495÷TPI) with common tap drills. For the full UNC/UNF/UNEF set and all tolerance grades, refer to the original chart images below.
| Size | TPI | Major(in) | Pitch dia(in) | Tap drill |
|---|---|---|---|---|
| 1/4-20 | 20 | 0.2500 | 0.2175 | #7 (~5.1mm) |
| 5/16-18 | 18 | 0.3125 | 0.2764 | F (~6.5mm) |
| 3/8-16 | 16 | 0.3750 | 0.3344 | 5/16" (~7.9mm) |
| 1/2-13 | 13 | 0.5000 | 0.4500 | 27/64" (~10.7mm) |
※ UNC basic-size example; tap drills are common references — adjust for material and tap type. See the Unified Thread Tap Drill Chart.
3. Tolerance Grades
| Grade | Description |
|---|---|
| External thread classes (1A/2A/3A) | Unified inch thread (ASME B1.1) external tolerance classes; a higher number means a tighter tolerance, 3A being the most precise |
| 2B (internal standard) | Most common internal-thread tolerance; standard fit |
| GH (GH1–GH3) | Tap pitch-dia compensation; higher = larger thread |
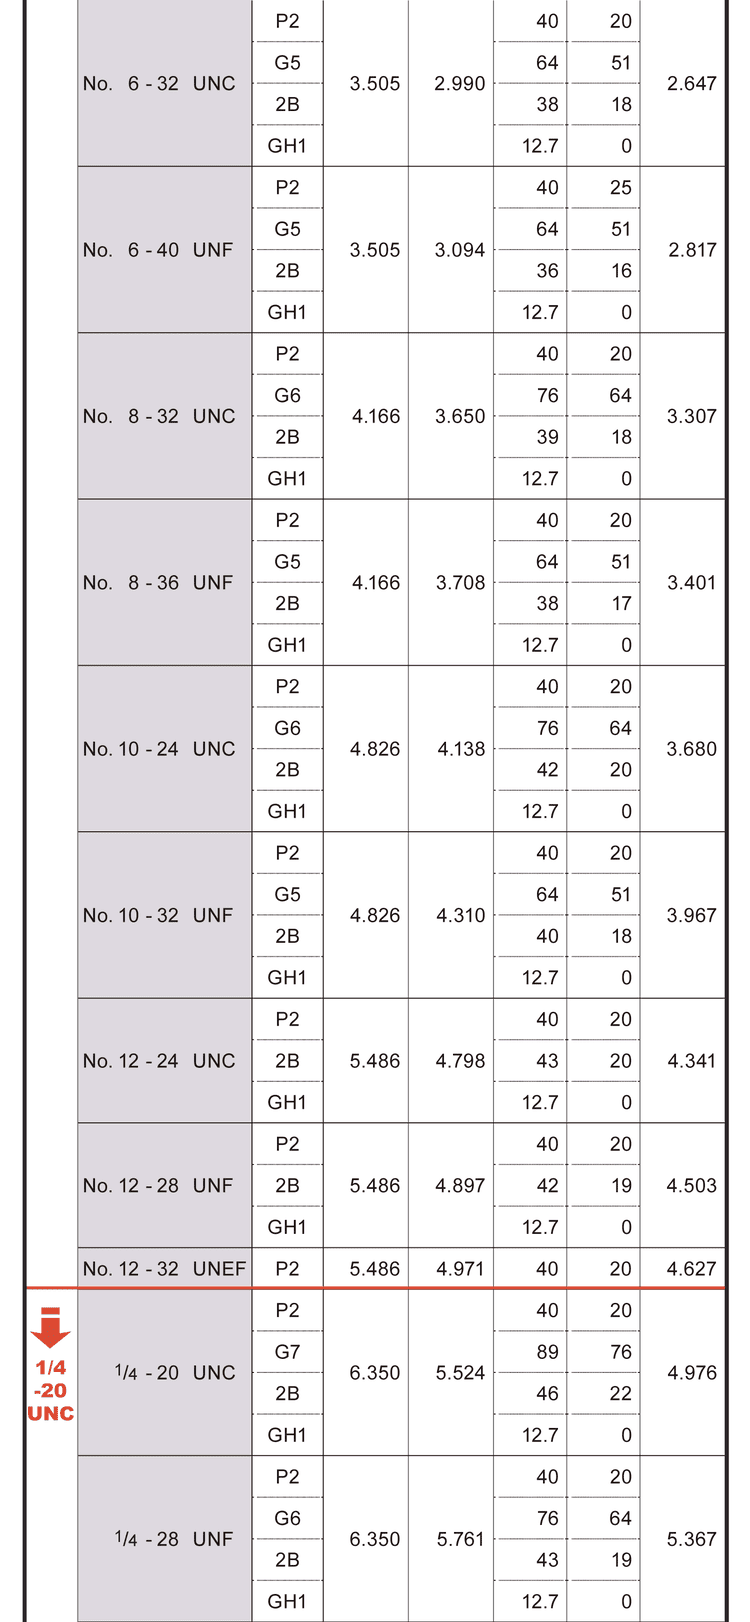
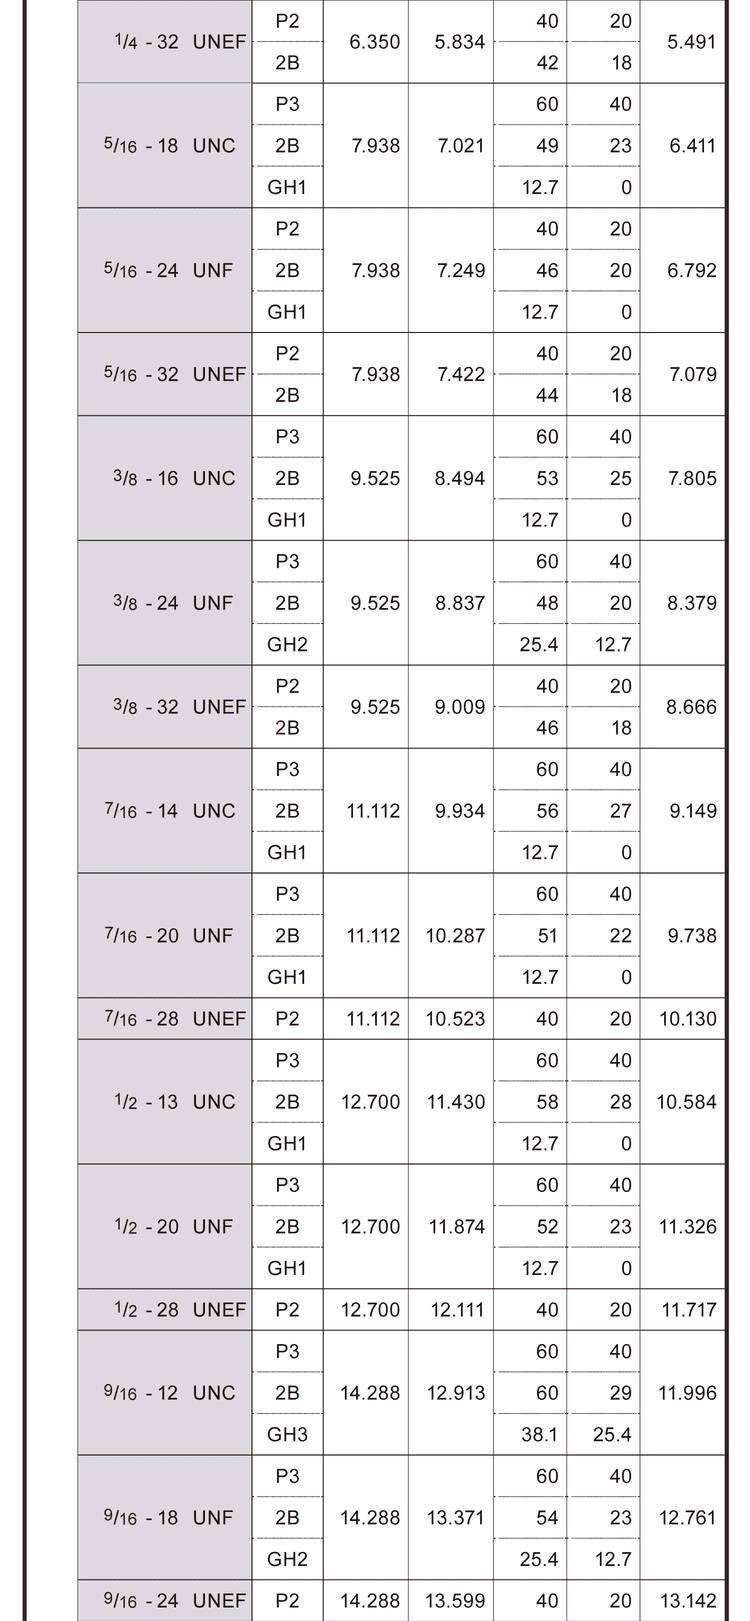
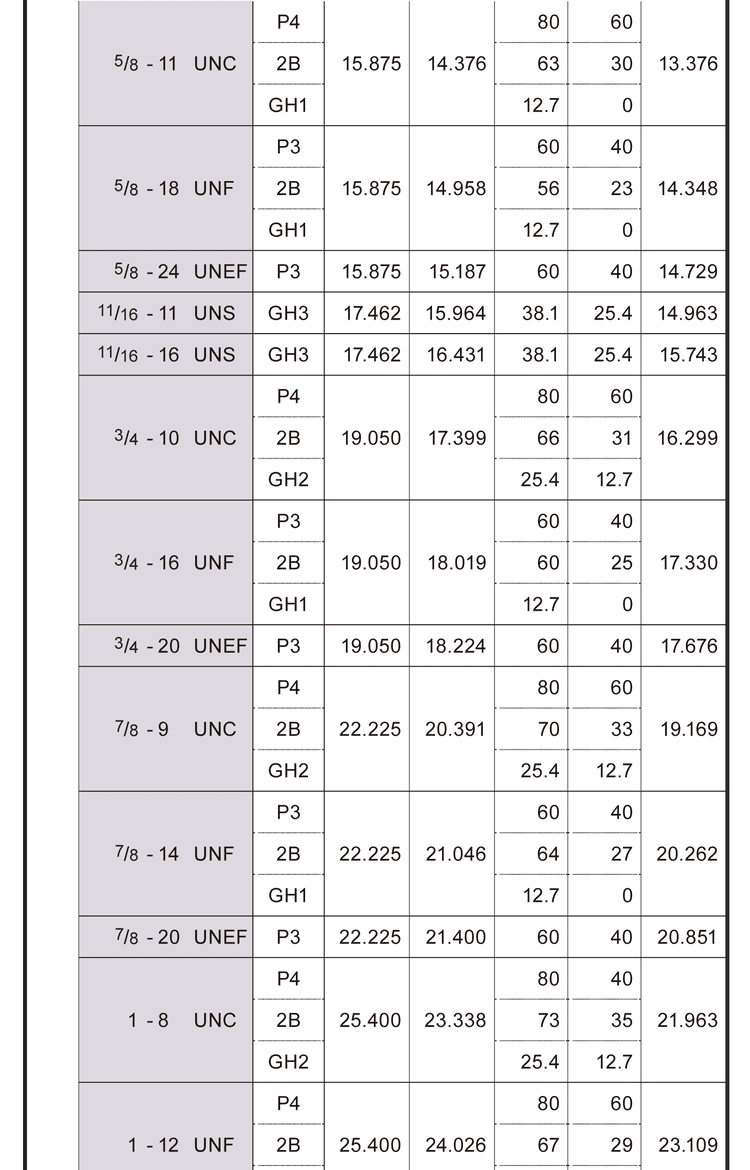
※ Full UNC/UNF/UNEF size and tolerance charts above; values per the original tables.
4. How to Use the Chart
| Step | Action |
|---|---|
| ① Pick thread size | e.g. 1/4-20 UNC, 1/2-13 UNC |
| ② Confirm TPI | Threads per inch sets the pitch |
| ③ Read pitch & minor dia | Used to work out the pilot hole |
| ④ Pick tolerance grade | Choose 2B or a higher-precision grade |
5. Applications
CNC machining sets pilot-hole size accurately and lowers tool wear; aerospace and automotive value reliable thread fit with anti-loosening and high strength; QC quickly judges whether thread sizes pass.
For pilot holes see the Unified Thread Tap Drill Chart; for internal-thread tolerance and fit see the Tap Thread Tolerance Guide; for metric and imperial standards see the Metric Thread Tolerance Chart and Imperial Thread Tolerance Chart.
FAQ
Q: UNC vs UNF?
UNC is coarse with fewer threads per inch — high strength and damage resistance for general structural parts; UNF is fine with more TPI — higher locking accuracy for precision parts and anti-loosening.
Q: What is grade 2B?
2B is the most common US internal-thread tolerance — a standard fit (1B looser, 3B tighter). Most tapped parts default to 2B unless special precision or fit is required.
Q: What does GH mean?
GH (Ground High) is the tap's pitch-diameter compensation limit; a higher number gives a larger cut thread. Match the GH grade to the required internal-thread tolerance (e.g. 2B) for a correct fit.
Q: How do I set the pilot hole for Unified threads?
Use the recommended drill for the size (e.g. #7 for 1/4-20, 27/64" for 1/2-13), then adjust for material. See the Unified tap-drill chart for exact values.
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.
Published: 2026-03-23 | Last updated: 2026-07-25









