
Internal Thread Machining Guide: ISO/UNC/NPT Depth & Passes
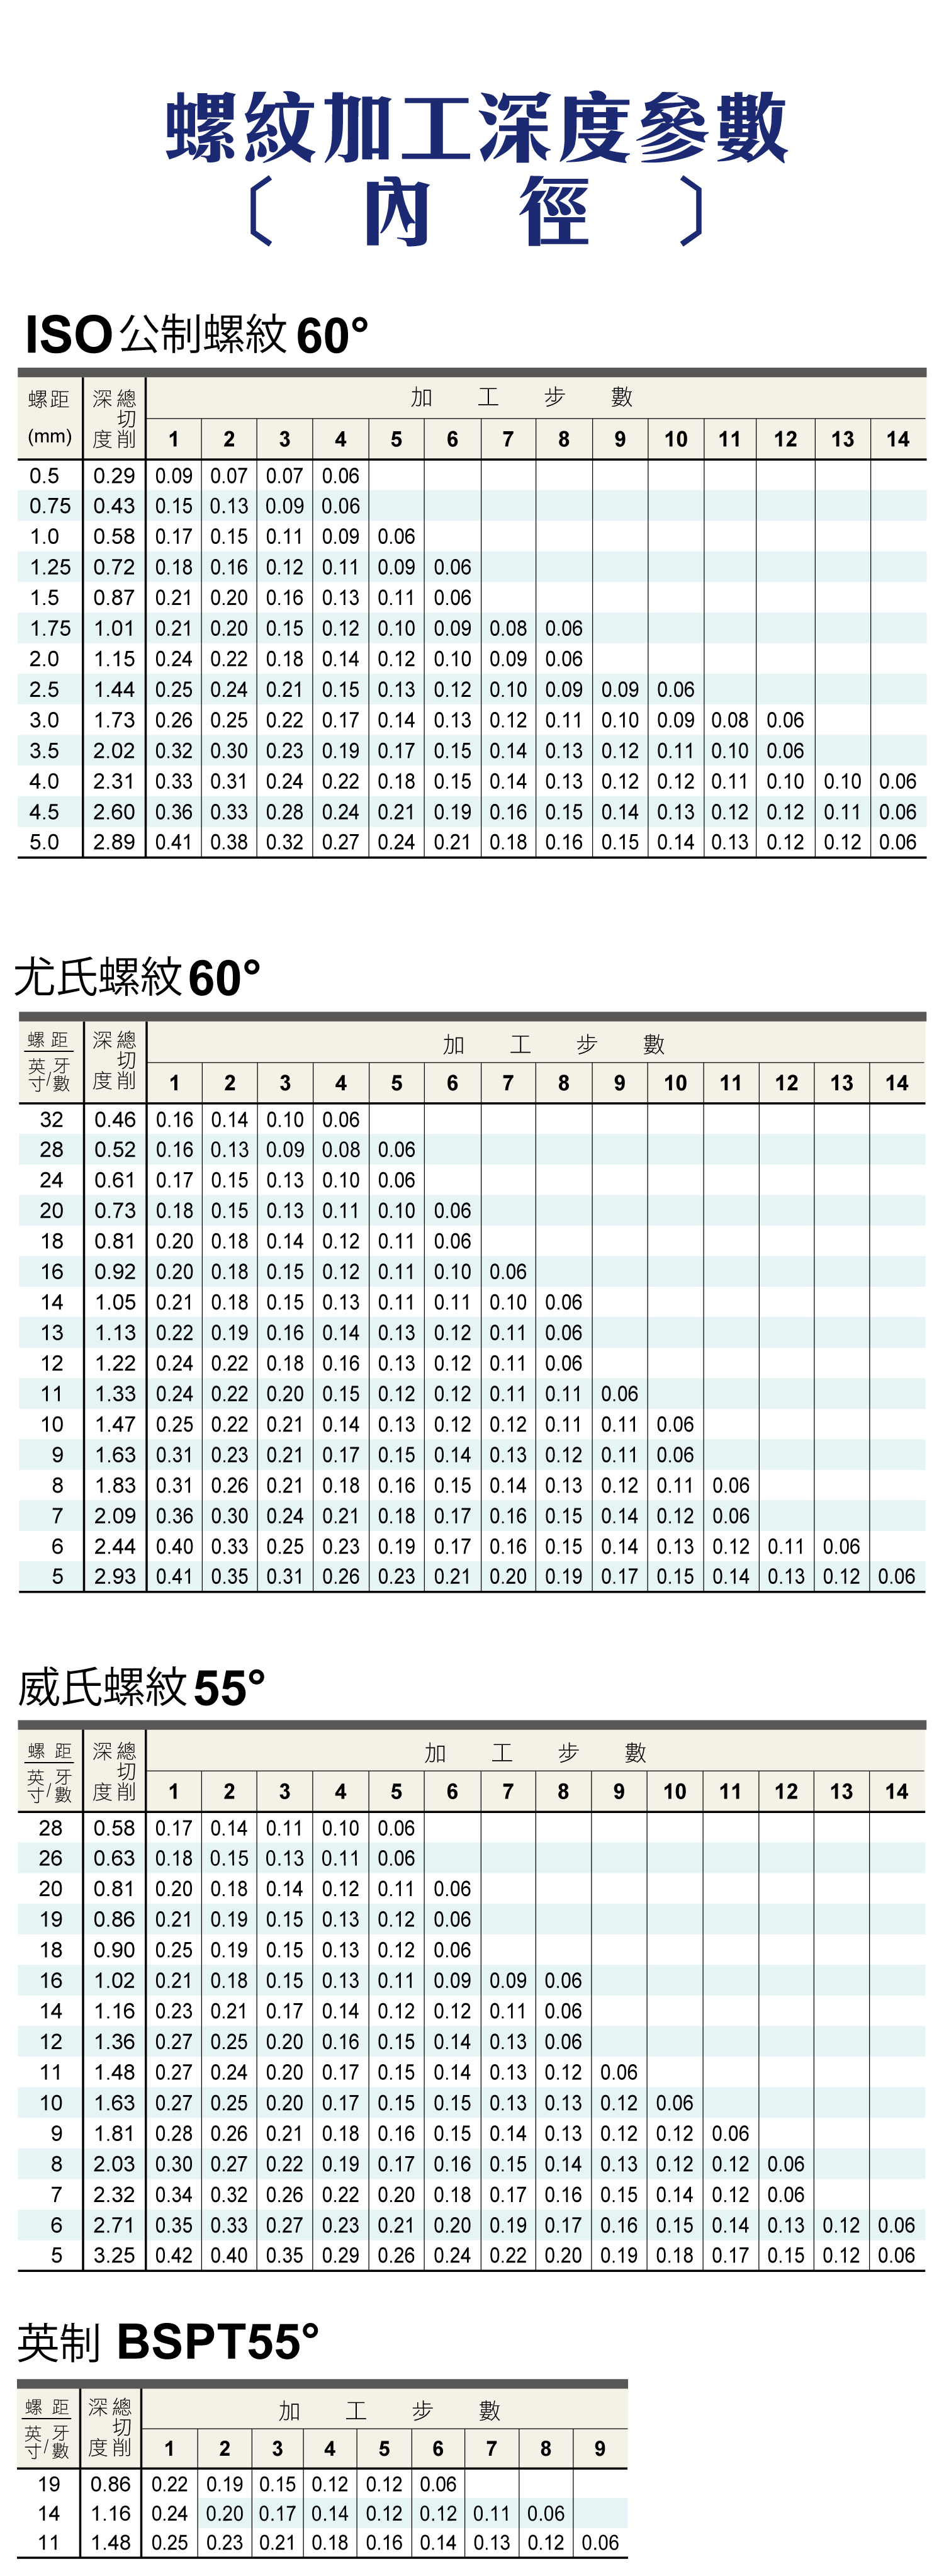
Internal thread machining parameters drive thread quality and tool life. Different standards (ISO, metric, UNC, BSPT, NPT) need different cutting depths and pass counts. This guide covers recommended depth distribution for internal-bore threading to lower breakage risk, improve thread-form accuracy and optimize efficiency. In practice, use a multi-pass strategy that distributes depth step by step for stable machining and dimensional accuracy.
1. What Are Internal Thread Parameters
Internal thread parameters are the depth distribution per pass and the total pass count, which drive thread accuracy (form completeness), tool life (avoiding chipping), stability (avoiding jamming) and surface roughness. They apply to CNC internal thread turning and thread milling; a tap forms the thread in a single pass, so there is no per-pass depth to distribute.
| Parameter | Effect |
|---|---|
| Depth distribution per pass | Thread accuracy (form), stability |
| Total pass count | Tool life (chipping), surface roughness |
2. Common Standards and Angle Differences
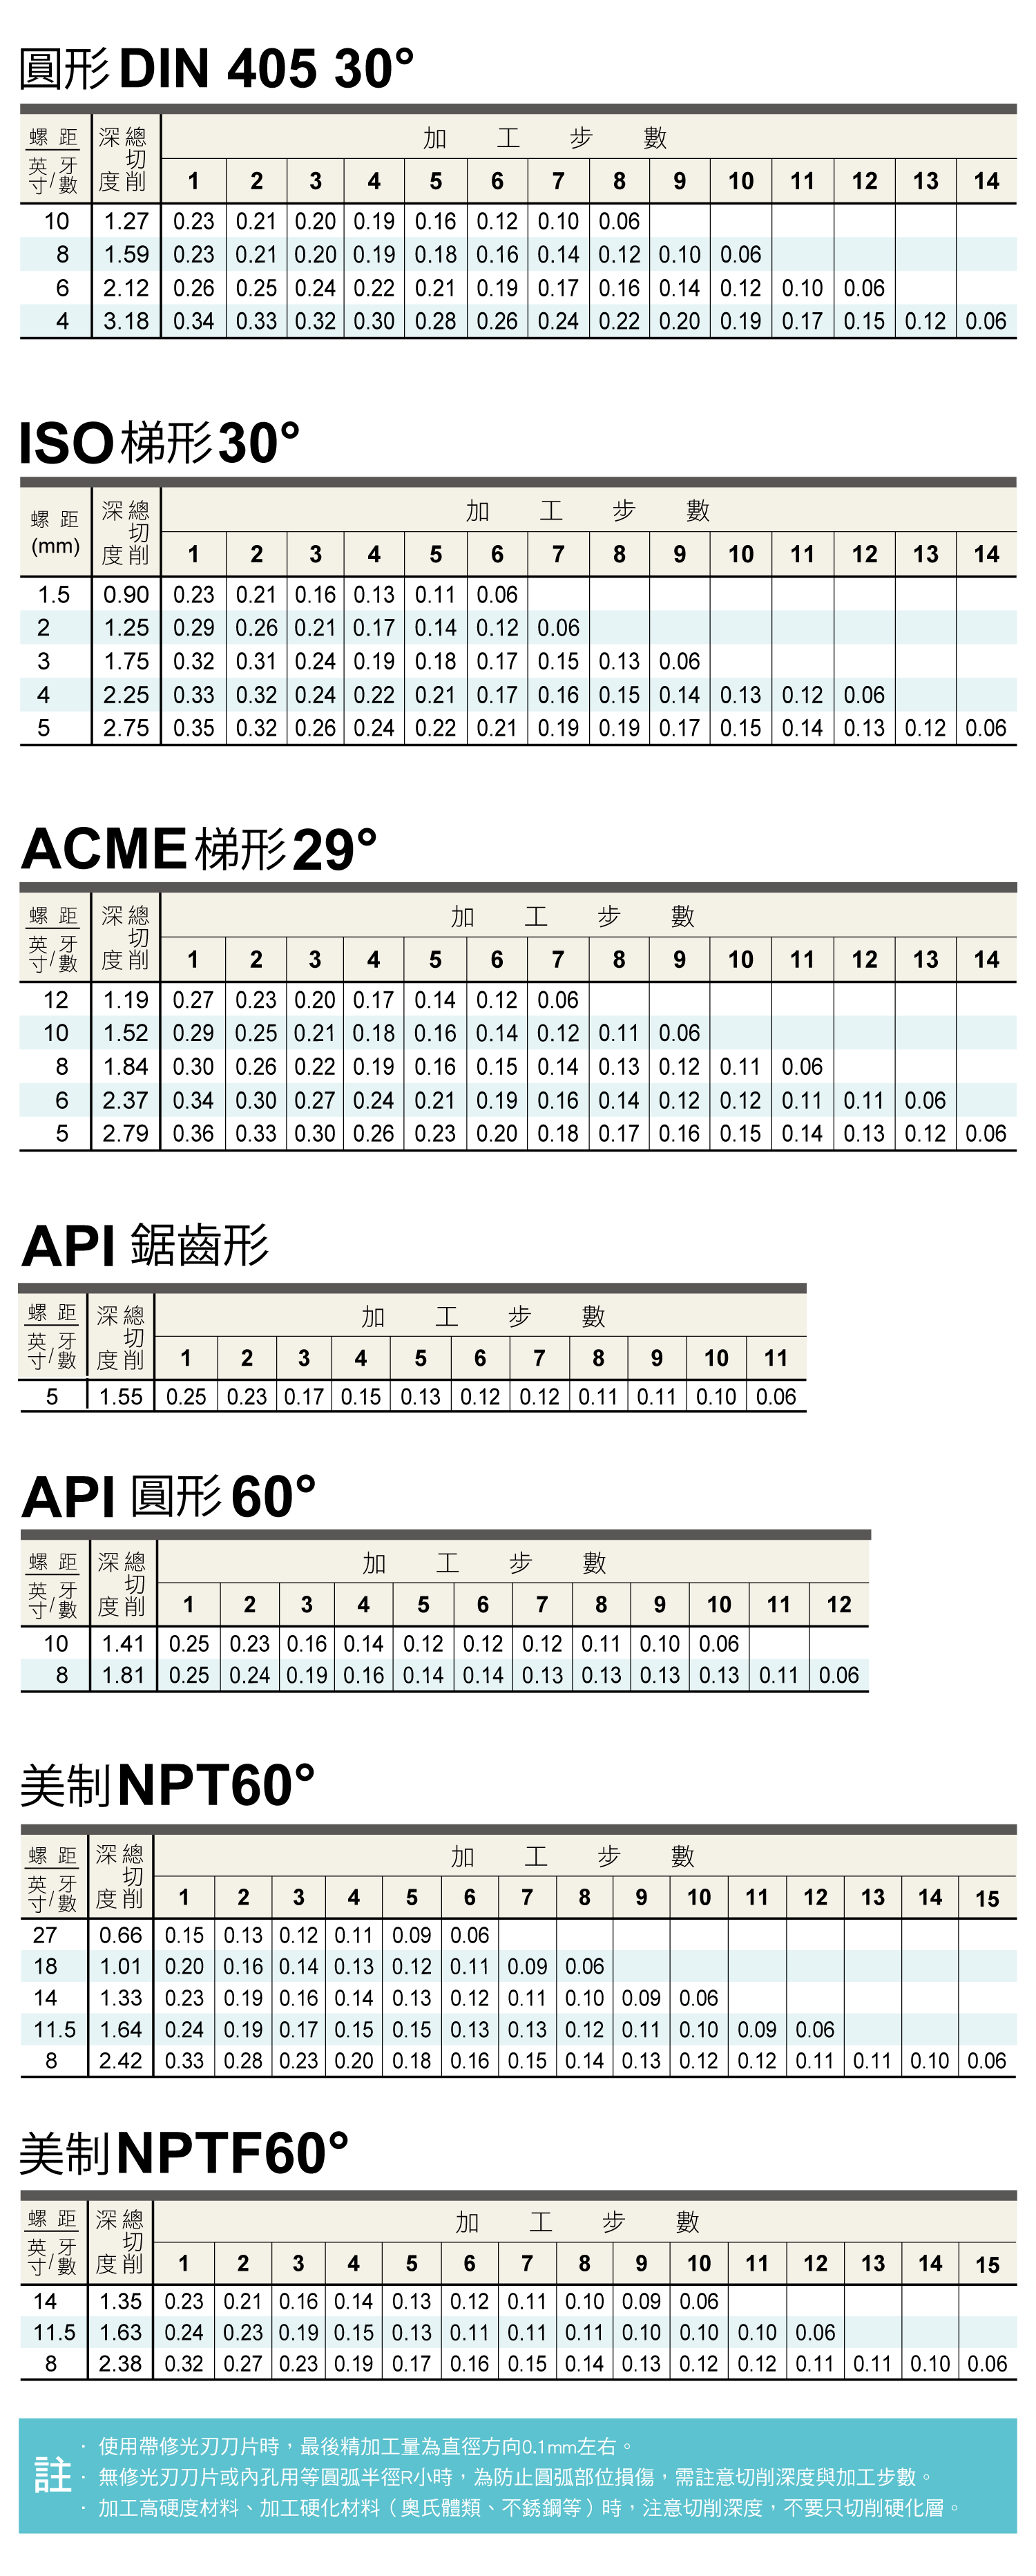
For the flank angles and uses of each thread standard, the full comparison table is in the Thread Profile Guide. For internal-bore machining, three things matter: for ISO metric and UNC / UNF the pass count follows the pitch (see section 3); BSPT / NPT taper pipe threads must hold their seal, so cut more conservatively; trapezoidal threads (Tr, ACME) remove a lot of material and need multi-pass layering.
3. Pass Count and Depth Logic
Use a degressive strategy: the first passes remove more material, the middle cuts steadily, and the last passes keep a small finish, lowering breakage risk and improving thread-form completeness.
| Stage | Distribution | Typical ratio (reference) |
|---|---|---|
| Pass 1 | Remove material fast (deeper) | ≈ 20–30% |
| Pass 2–5 | Step down, steady cutting | Converge gradually |
| Final 2 passes | Finish and correct (~0.06 mm) | Fixed small cut |
These ratios are a reference strategy; actual depth and pass count depend on pitch, material and tool — see the Turning Machining Formulas.
4. Internal-Bore Practical Points
| Point | Note |
|---|---|
| Final finish | Last pass ≈ 0.06 mm to ensure thread form |
| Avoid bottom interference | Watch tools without a wiper; prevent hitting the bore bottom |
| Hard materials | Stainless, hardened steel: lower depth, add passes |
| Small-diameter threads | Low tool strength; add more passes |
| Planning passes | Coarser pitch, more passes; an internal thread is shallower, so do not reuse the total infeed from the External Thread Machining Guide |
| Equal depth per pass | Only for pitch 1.5 mm (16 TPI) or finer; use degressive infeed for coarser pitches |
| Switching to flank infeed | Feeding along one flank gives chips twice as thick as radial infeed at the same radial depth, so re-plan the depth per pass |
5. Tapping vs Thread Milling (Internal)
Internal threads can be tapped or thread-milled, differing in forming, risk and use:
| Method | Trait | Best for |
|---|---|---|
| Tapping | Single-pass forming, fast but higher risk | General volume internal threads |
| Thread milling | Multi-pass, high accuracy, flexible | High-value parts, large or hard materials |
For external (OD) thread parameters, see the External Thread Machining Guide; for thread-form comparison, see the Thread Profile Guide.
FAQ
Q: How many passes for an internal thread?
It depends on pitch, material and thread type; coarser pitches need more passes. An internal thread is shallower than an external one, so take the pass count and depth per pass from the insert maker's internal-thread infeed table. Hard materials and small diameters need more passes. Use degressive infeed, deep-to-shallow, keeping a ~0.06 mm finish pass.
Q: Why does internal-bore work break tools easily?
Bore space is limited and evacuation is hard; the tool has long overhang and lower rigidity, so one deep cut or unmanaged bottom interference can jam or break it. Use multi-pass degressive cutting, lower per-pass depth, watch bottom clearance on wiperless tools, and ensure evacuation and cooling.
Q: What to watch for stainless or hardened internal threads?
For hard materials, lower the depth and add passes to reduce load and chipping risk, with coolant and a steady feed. Small-diameter threads have weak tools, so add even more passes. Look up actual speeds by material in the formulas guide.
Q: Tapping or thread milling?
Tapping forms in one pass and is fast, good for general volume internal threads but with higher breakage risk; thread milling is multi-pass with high accuracy and flexibility, good for high-value parts, large diameters or hard materials. Choose by volume, accuracy and material.
Last updated: 2026-10-12
For the full reading guides on this topic, see Thread Machining: A Complete Reading Guide and Tool Life and Wear: A Complete Reading Guide.









