
External Thread Machining Guide: ISO/UNC/NPT Depth & Passes
External thread machining parameters control the cutting depth in thread turning or thread milling. Different standards (ISO, metric, UNC, BSPT, NPT, ACME) need suitable pass counts and depth distribution. This guide covers cutting depth and a degressive-infeed strategy for external threads to lower tool wear, avoid chatter and chipping, and improve thread surface quality and accuracy.
1. What Are External Thread Parameters
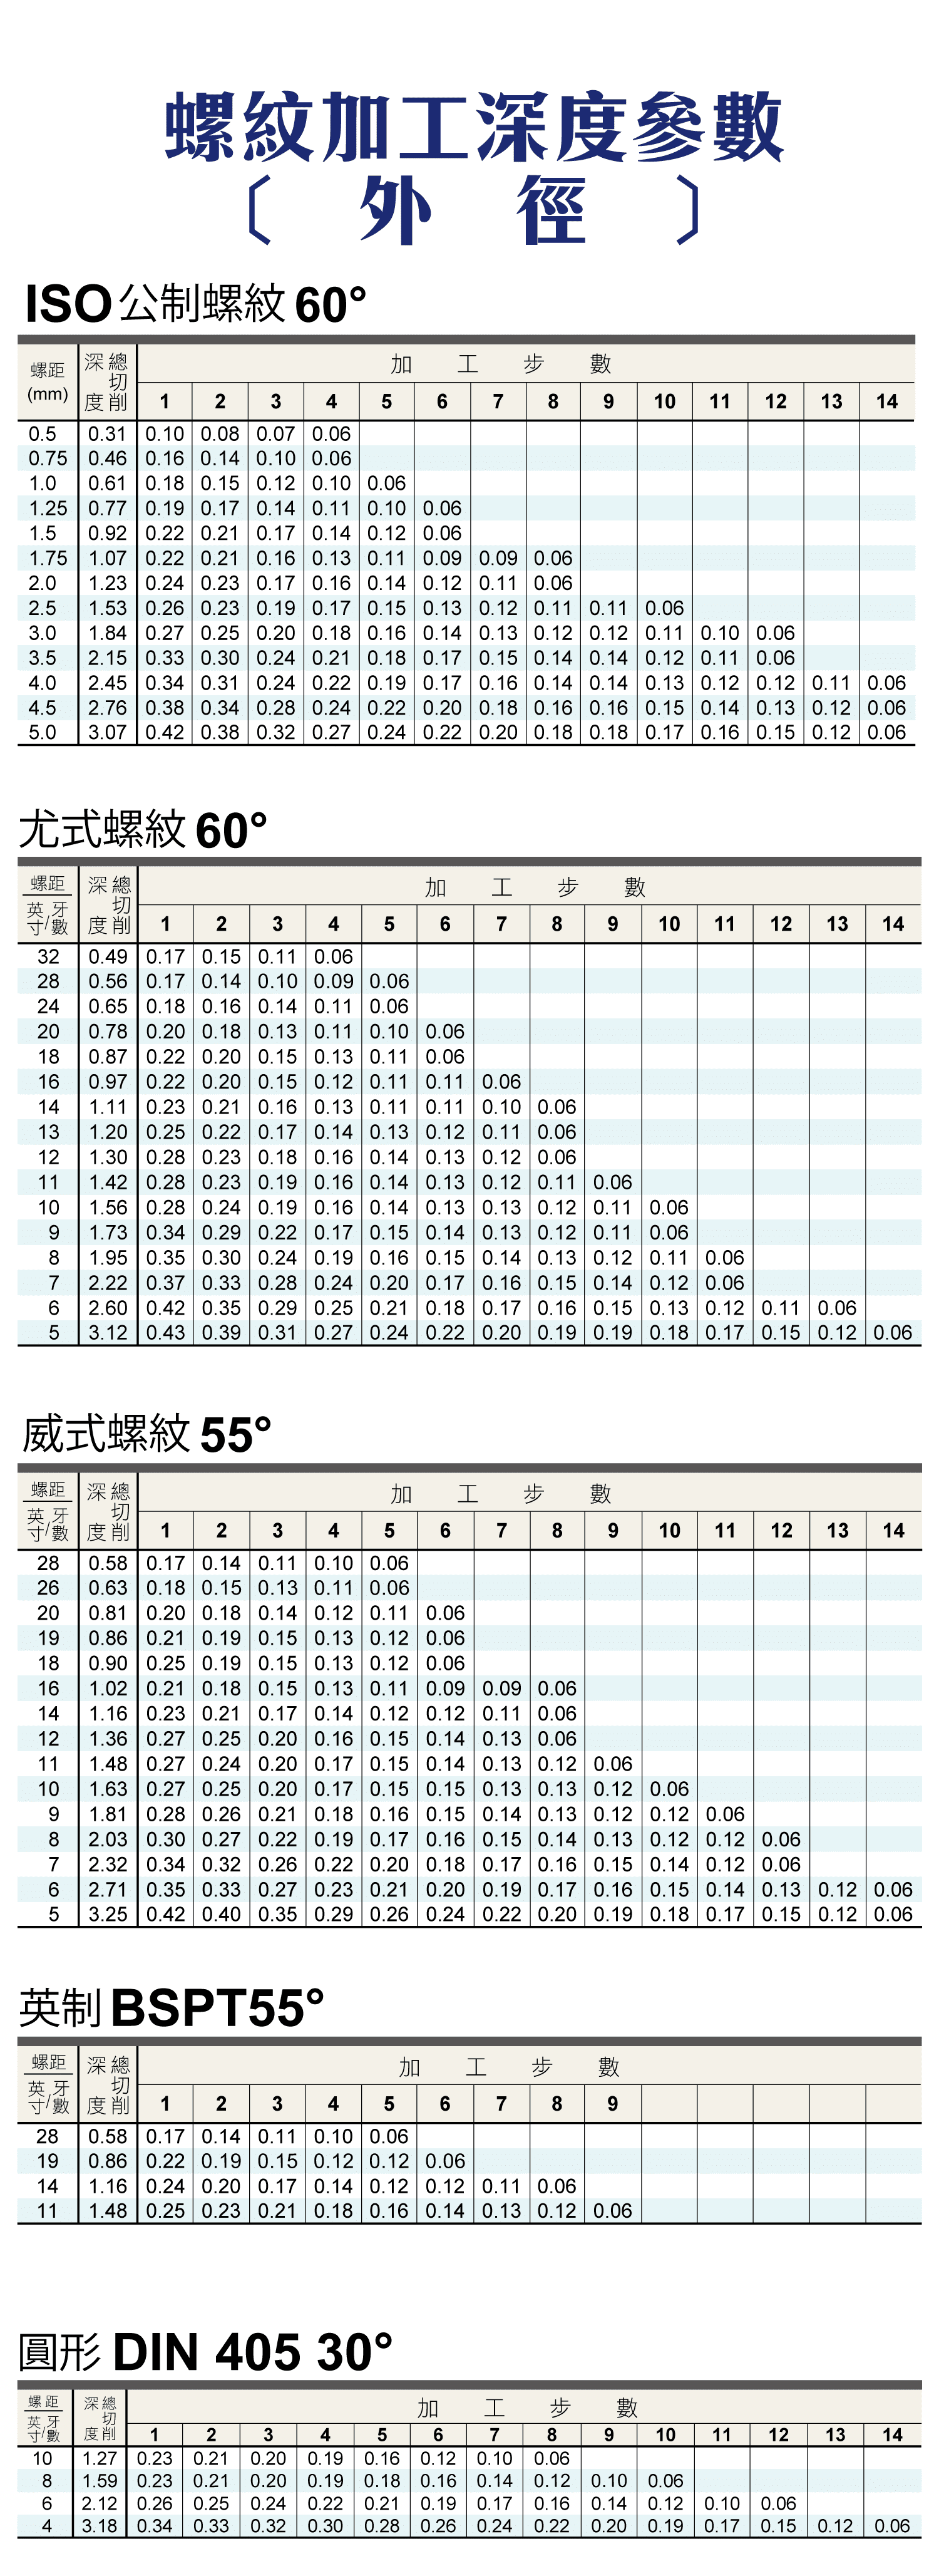
External thread parameters are the depth per pass and the number of passes, used mainly in CNC thread turning, thread milling and pre-rolling control.
2. Common Thread Types and Applications
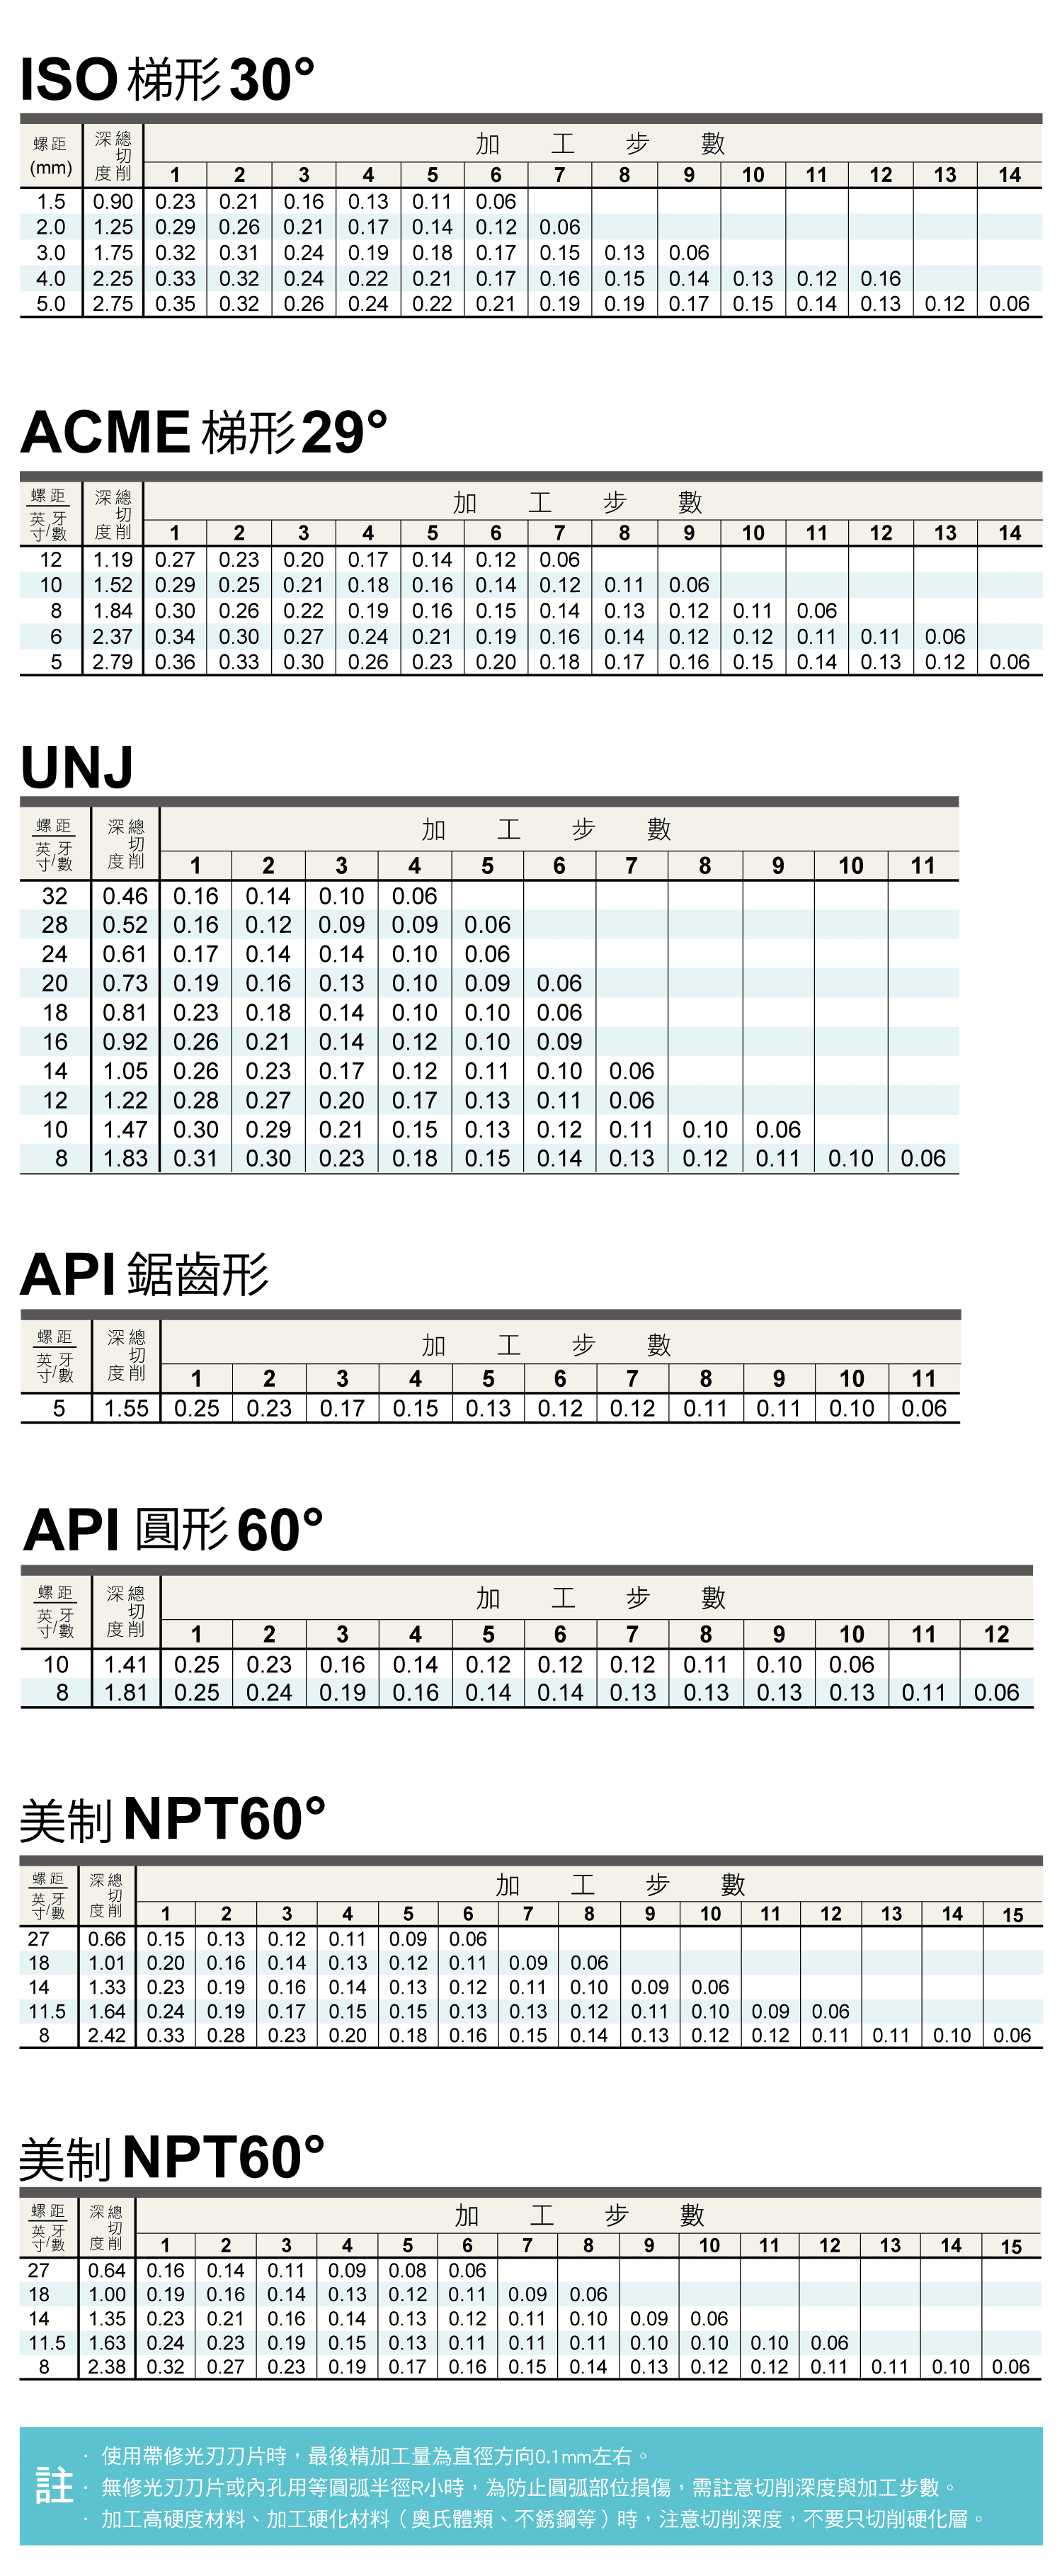
For the flank angles and uses of each thread standard, the full comparison table is in the Thread Profile Guide. For external threading, three things matter: for ISO metric the pass count follows the pitch (see the table in section 3); BSPT and NPT / NPTF taper pipe threads must seal, so cut conservatively and control depth precisely to avoid thin threads; ACME trapezoidal threads remove a lot of material and need multi-pass layering.
3. External Infeed Strategy (Degressive)
External threads are best cut with degressive infeed: remove more material in the first passes, reduce step by step, and finish with a light pass to limit tool load, chatter and chipping. The tables below are one set of starting values by pitch, with thread depth taken as 0.65P (allowing for the tool nose radius).
| Pitch (mm) | 1.0 | 1.5 | 2 | 2.5 | 3 | 3.5 | 4 |
|---|---|---|---|---|---|---|---|
| Thread depth (radius) | 0.649 | 0.974 | 1.299 | 1.624 | 1.949 | 2.273 | 2.598 |
| Pass 1 | 0.7 | 0.8 | 0.9 | 1.0 | 1.2 | 1.5 | 1.5 |
| Pass 2 | 0.4 | 0.6 | 0.6 | 0.7 | 0.7 | 0.7 | 0.8 |
| Pass 3 | 0.2 | 0.4 | 0.6 | 0.6 | 0.6 | 0.6 | 0.6 |
| Pass 4 | — | 0.16 | 0.4 | 0.4 | 0.4 | 0.6 | 0.6 |
| Pass 5 | — | — | 0.1 | 0.4 | 0.4 | 0.4 | 0.4 |
| Pass 6 | — | — | — | 0.15 | 0.4 | 0.4 | 0.4 |
| Pass 7 | — | — | — | — | 0.2 | 0.2 | 0.4 |
| Pass 8 | — | — | — | — | — | 0.15 | 0.3 |
| Pass 9 | — | — | — | — | — | — | 0.2 |
| TPI | 24 | 18 | 16 | 14 | 12 | 10 | 8 |
|---|---|---|---|---|---|---|---|
| Thread depth (radius) | 0.698 | 0.904 | 1.016 | 1.162 | 1.355 | 1.626 | 2.033 |
| Pass 1 | 0.8 | 0.8 | 0.8 | 0.8 | 0.9 | 1.0 | 1.2 |
| Pass 2 | 0.4 | 0.6 | 0.6 | 0.6 | 0.6 | 0.7 | 0.7 |
| Pass 3 | 0.16 | 0.3 | 0.5 | 0.5 | 0.6 | 0.6 | 0.6 |
| Pass 4 | — | 0.11 | 0.14 | 0.3 | 0.4 | 0.4 | 0.5 |
| Pass 5 | — | — | — | 0.13 | 0.21 | 0.4 | 0.5 |
| Pass 6 | — | — | — | — | — | 0.16 | 0.4 |
| Pass 7 | — | — | — | — | — | — | 0.17 |
Infeed per pass is a diameter value (the X-axis step per pass in the program), so the actual radial depth is half the table value, and the passes add up to about twice the thread depth. These are starting values; insert makers’ infeed tables are usually finer (for example, pitch 1.5 mm in 6 passes totalling 0.94 mm radially, per the Sandvik technical handbook). Follow the catalogue of the insert you use; for the formula see CNC Thread Cutting Depth Guide, and for parameter calculations see Turning Machining Formulas.
4. Practical Points
| Point | Note |
|---|---|
| Final finish pass | ~0.06 mm suggested, improves finish and thread form |
| Avoid chatter | External work chatters more; reduce the last few passes' cut |
| Hard materials | SUS, titanium: cut depth 30–50% lower, more passes |
| Large-diameter threads | High load; add passes to avoid tool breakage |
5. CNC Thread Turning vs Thread Milling (External)
External threads can be turned or milled, each with trade-offs in stability, accuracy and use:
| Item | Thread turning | Thread milling |
|---|---|---|
| Method | Single-point forming | Multi-pass milling |
| Stability | Lower | High |
| Accuracy | Medium | High |
| Best for | Volume production | High-value parts |
6. Machining Notes
Don't skip the finish pass; small-diameter threads need more passes; watch bottom interference with tools lacking a wiper; avoid one deep cut in hard materials; and use coolant with a steady feed. For tolerance-grade selection, see the External Thread Tolerance Guide.
FAQ
Q: How many passes for an external thread?
It depends on pitch: with the starting values in section 3, metric pitch 1.0 takes about 3 passes, 1.5 about 4, 2.0 about 5, 3.0 about 7 and 4.0 about 9; hard materials and large diameters need more. Use degressive infeed, deep-to-shallow, and keep a small finish pass.
Q: What is degressive infeed?
Degressive infeed reduces each pass's cut step by step: passes 1–2 cut deeper to remove most material, the middle steps down, later passes converge, and the last 1–2 finish at about 0.06 mm. It spreads tool load, avoids chatter and chipping, and improves thread form.
Q: What to watch when threading stainless or titanium?
For hard materials (SUS, titanium), lower the cut depth by 30–50% and add passes to reduce load and chipping risk, with coolant and a steady feed. Look up actual speeds by material in the formulas guide.
Q: Thread turning or thread milling?
Thread turning is single-point forming, efficient for volume production but medium in stability and accuracy; thread milling is multi-pass with high stability and accuracy, good for high-value parts, large diameters or hard materials. Choose by volume and accuracy needs.
Last updated: 2026-10-12
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.









