
Thread Profile Guide: 60° V, 55° Whitworth, Trapezoidal & Round
The thread profile is a core geometric element in mechanical connection and transmission design, directly affecting strength, sealing, friction and load capacity. Common profiles include the 60° V (ISO / UN), 55° Whitworth, trapezoidal (Tr / ACME) and round thread, each with its own standard for angle and crest/root radius. Choosing the right profile improves accuracy, extends life and ensures structural reliability.
1. Thread Profile Basics
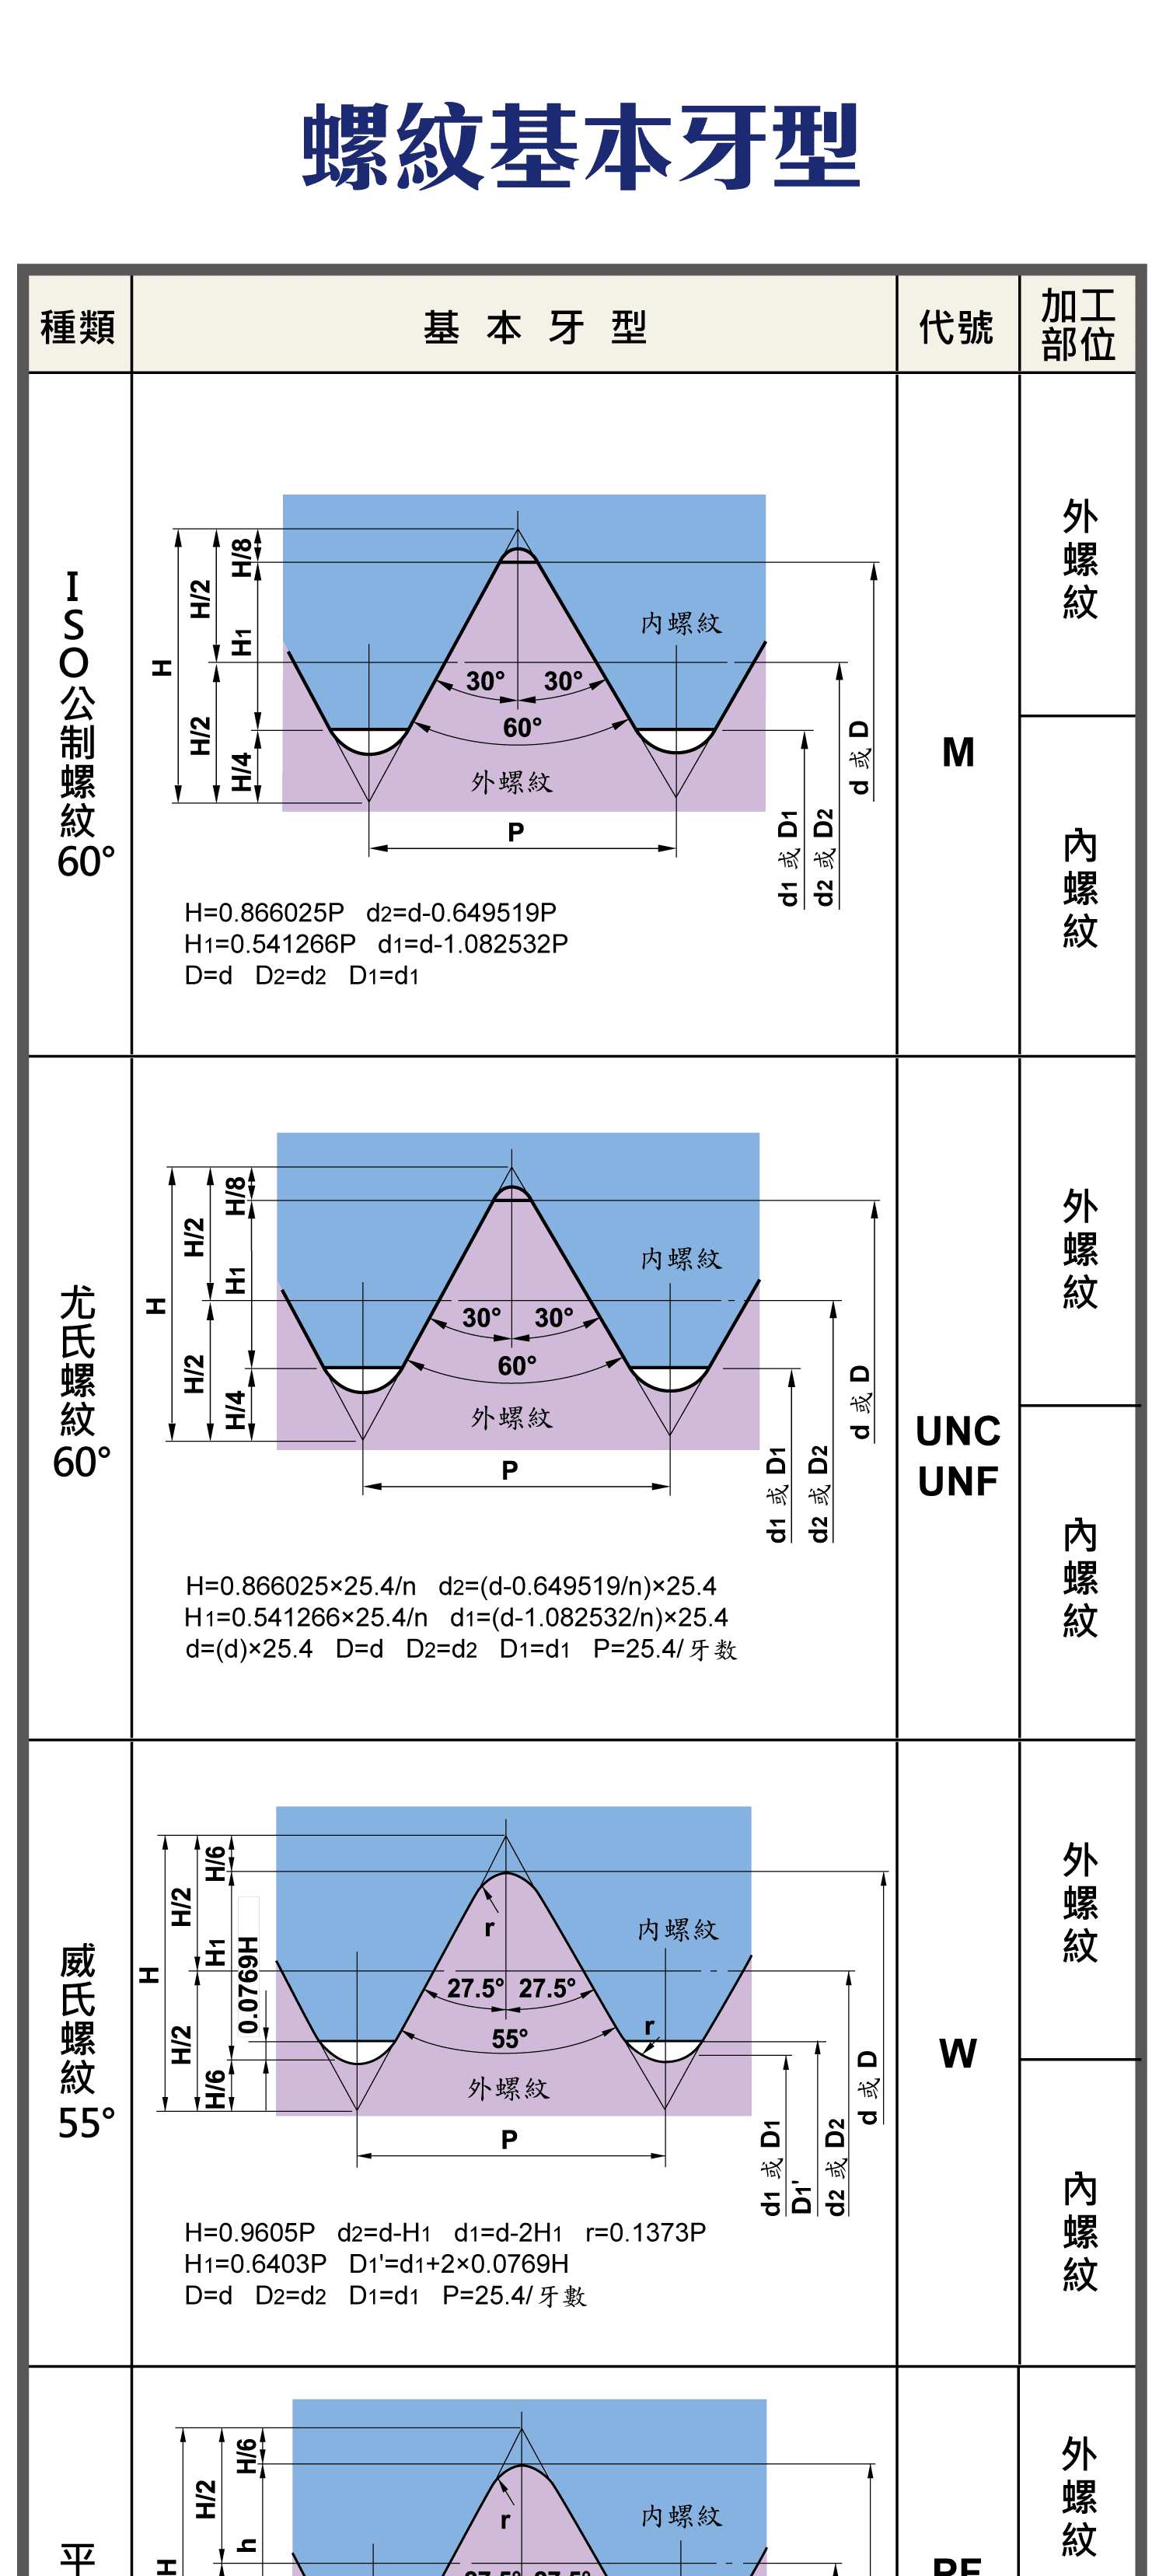
The thread profile is the cross-sectional shape of the thread. Its core parameters are the thread angle, pitch (P), height (H), and the crest and root radius.
2. Common Thread Profiles
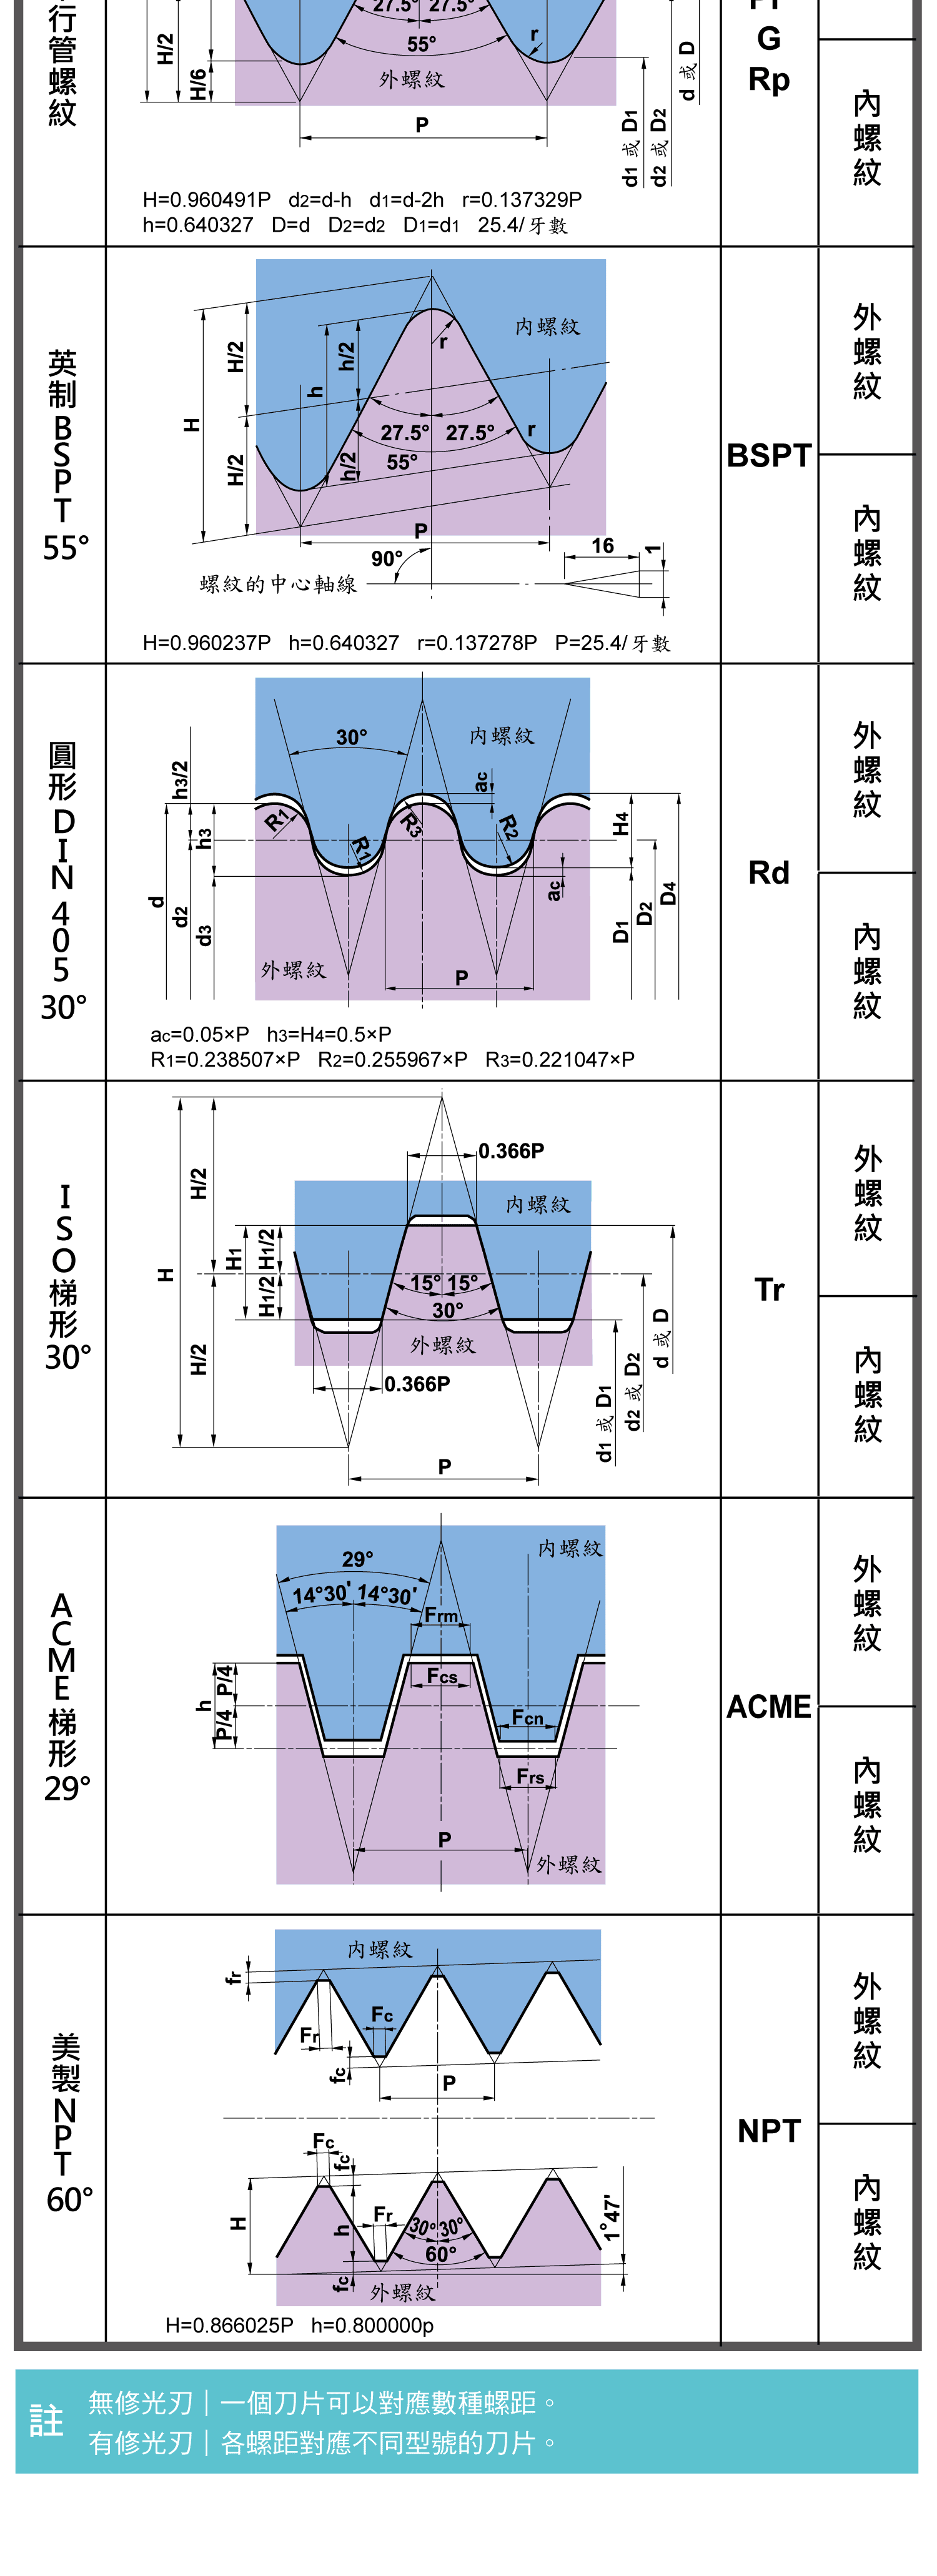
By angle and use, common profiles fall into four groups:
| Profile | Angle | Advantages | Application |
|---|---|---|---|
| 60° V (ISO / UN) | 60° (30°+30°) | Versatile, easy to cut, stable accuracy | Machine structures, bolts & nuts |
| 55° Whitworth | 55° (27.5°+27.5°), rounded crest/root | Lower stress concentration, better fatigue | Inch equipment, pipe connections |
| Trapezoidal (Tr / ACME) | 30° (ISO Tr) or 29° (ACME), flat crest | High load capacity, for transmission | Lead screws, mechanical drives |
| Round thread | Rounded profile | Impact resistant, resists chip clogging | Food equipment, fire equipment |
3. Internal vs External Thread
The same profile differs slightly between internal and external threads; the two must be designed together to ensure clearance fit, sealing and matched strength.
| Type | Location | Profile trait |
|---|---|---|
| External | Cut on the shaft outside | Root must carry a radius; minor diameter cut deeper than the internal minor |
| Internal | Cut inside the bore | Crest at the minor diameter is flat and leaves the external root radius clear |
Taking ISO metric threads as the example, internal and external threads share the same 60° basic profile. The external minor diameter is cut about 0.144P deeper than the internal minor diameter — exactly the root radius. The external root needs that radius so it does not crack from a sharp corner under fatigue, and the internal crest must not fill it, or the two would interfere at the root.
4. Profile Geometry Keys
Angle, radius and pitch are the three keys: the angle shapes how load is carried and the use case (the 60° V is versatile; smaller-angle forms such as trapezoidal/ACME use a large symmetric contact face for transmission and load); crest/root radii lower stress concentration and extend life; a larger pitch moves faster, a smaller one positions more precisely.
| Parameter | Effect |
|---|---|
| Thread angle | Larger → strength; smaller → transmission efficiency |
| Radius design | Lowers stress concentration, extends life |
| Pitch | Large → fast move; small → precise positioning |
5. Selection and Comparison
Select by need: high accuracy → ISO / UN; high strength → Whitworth (rounded); transmission → trapezoidal / ACME; harsh environments → round thread. For machining parameters, see the External Thread Machining Guide and Internal Thread Machining Guide; for a full type overview, see the Thread Types Guide. Whether a threading insert has a wiper is a design choice of the insert, not part of the profile; for how to choose, see Choosing a Thread Turning Insert.
| Type | Angle | Trait | Use |
|---|---|---|---|
| ISO / UN | 60° | General | Screws |
| Whitworth | 55° | Fatigue-resistant | Pipe fittings |
| Tr / ACME | 30° / 29° | Transmission | Screws/lead screws |
| Round | Curved | Impact resistant | Food equipment |
6. Sizing Trapezoidal and ACME Threads
Trapezoidal Tr and ACME threads both have a basic thread height of half the pitch P, so pitch and minor diameters come straight from the nominal diameter and pitch:
| Item | Trapezoidal Tr (metric) | ACME (inch) |
|---|---|---|
| Thread angle | 30° (half-angle 15°) | 29° (half-angle 14.5°) |
| Basic thread height | 0.5P | 0.5P |
| Pitch diameter | nominal − 0.5P | nominal − 0.5P |
| Minor diameter (basic) | nominal − P | nominal − P |
| Clearance | Clearance ac at both major and minor diameter, none at the pitch diameter | Allowance added to the thread depth, from a table by pitch |
Example: for Tr20×4 the pitch diameter = 20 − 0.5×4 = 18 mm and the basic minor diameter = 20 − 4 = 16 mm; the actual external minor diameter is a further 2 × ac smaller, with ac taken from a table by pitch. Tolerance classes recommended by ISO 2903: 7H, 8H, 9H for internal and 7e, 8e, 8c, 9c for external threads.
The two differ by only 1°, but one is metric and the other inch, with different clearance rules, so neither the tools nor the gauges are interchangeable. For grinding trapezoidal tools see How to Regrind Thread Turning Tools.
FAQ
Q: 60° V vs 55° Whitworth — what's the difference?
The 60° V (ISO/UN) has a larger angle, high versatility, easy machining and stable accuracy — the most common structural thread; the 55° Whitworth has rounded crest and root, lowering stress concentration for good fatigue resistance, common in inch equipment and pipe connections.
Q: Which profile for transmission?
Use a trapezoidal thread (ISO Tr 30° or ACME 29°) with a flat crest and high load capacity, suited to lead screws and mechanical drives. The smaller angle helps transmission efficiency, and its symmetric large contact face provides high load capacity for lead screws and drives.
Q: Are internal and external profiles the same?
The basic profile is the same — 60° for ISO metric. The difference is at the root: the external thread carries a root radius and its minor diameter is cut about 0.144P deeper than the internal minor diameter, while the internal crest at the minor diameter is flat and leaves that radius clear. Standards such as Whitworth and UNJ/MJ aerospace threads set their own root-radius rules, so follow the standard in use.
Q: What's the benefit of crest/root radii?
Crest and root radii lower stress concentration, improving fatigue resistance and life — especially important for connections under alternating loads. Whitworth and aerospace UNJ both use rounded roots to boost fatigue strength.
Last updated: 2026-10-12
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.









