
Thread Milling Guide: Helical Feed, Selection & Conditions
Tap it, or thread-mill it? This guide helps you decide: whether the hole is blind, whether the thread is on the large side, how well the material cuts, how much one broken tool costs you, and whether a single cutter needs to cover several sizes. How thread milling differs from tapping, what to weigh when selecting, and reference cutting conditions are all here.
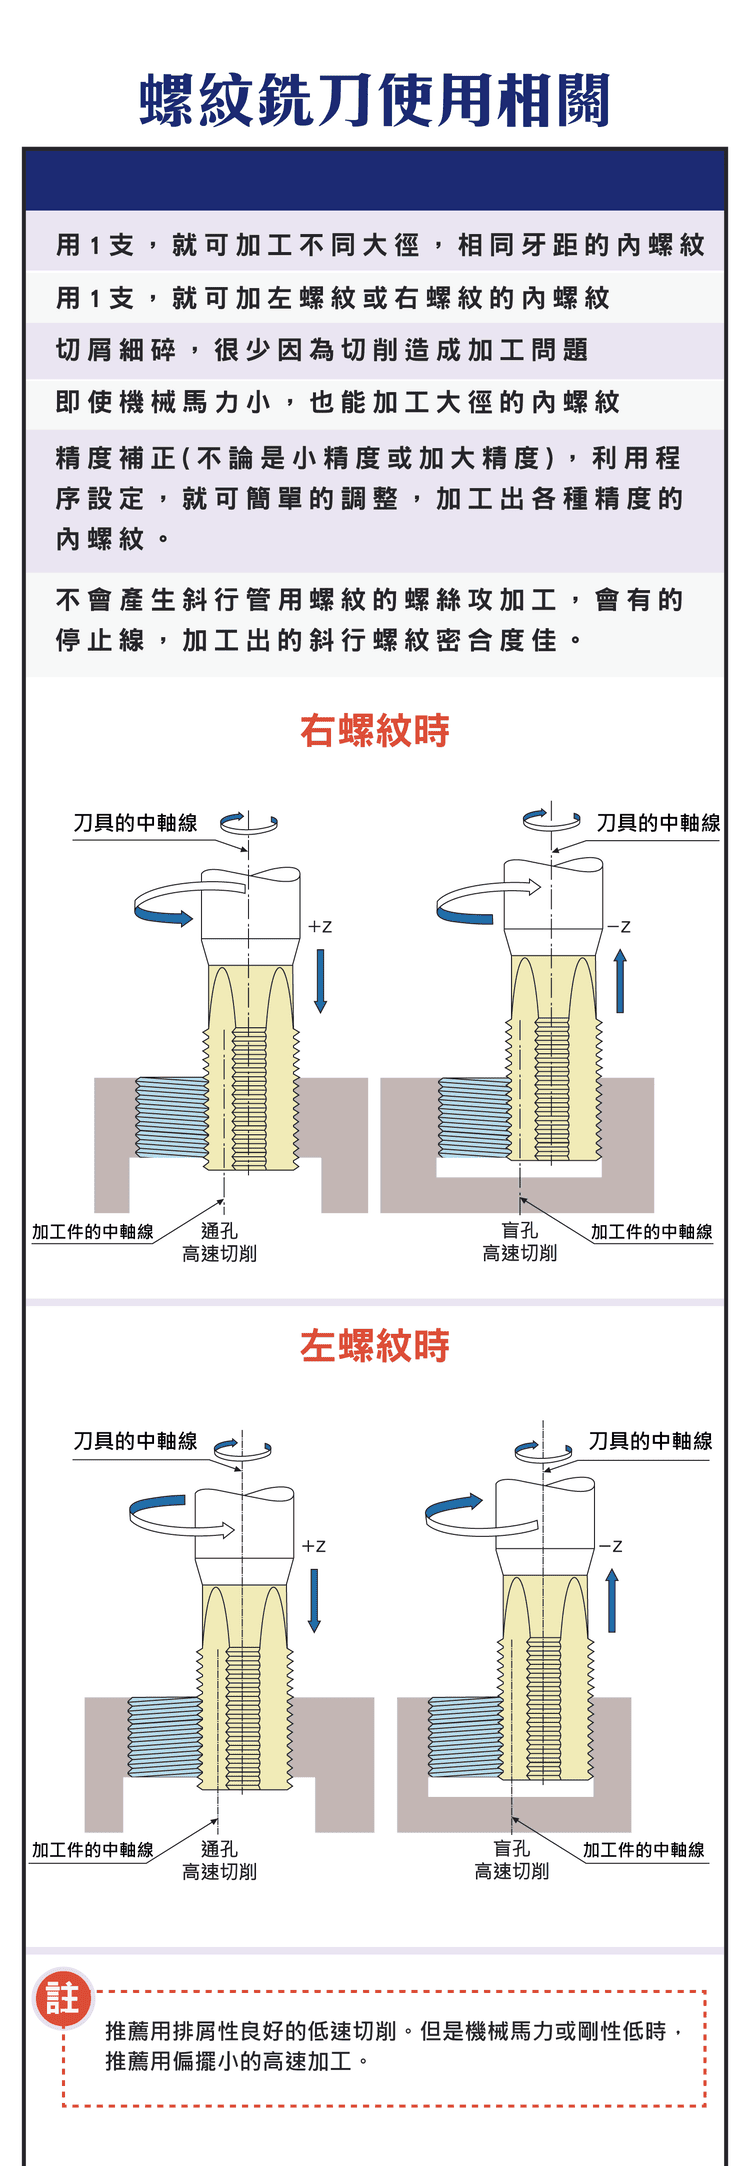
1. Core Advantages
| Advantage | Description |
|---|---|
| One tool, many diameters | Same cutter makes several diameters (same pitch) |
| Left or right hand | The CNC program sets direction; one tool cuts both |
| Small chips | Less clogging, steadier evacuation |
| Large diameters on low power | Progressive cutting suits low-power machines on big diameters |
| Program compensation | Thread accuracy adjustable via radius offset |
| No stop line | Helical feed leaves no stop line; tight fit, stable surface |
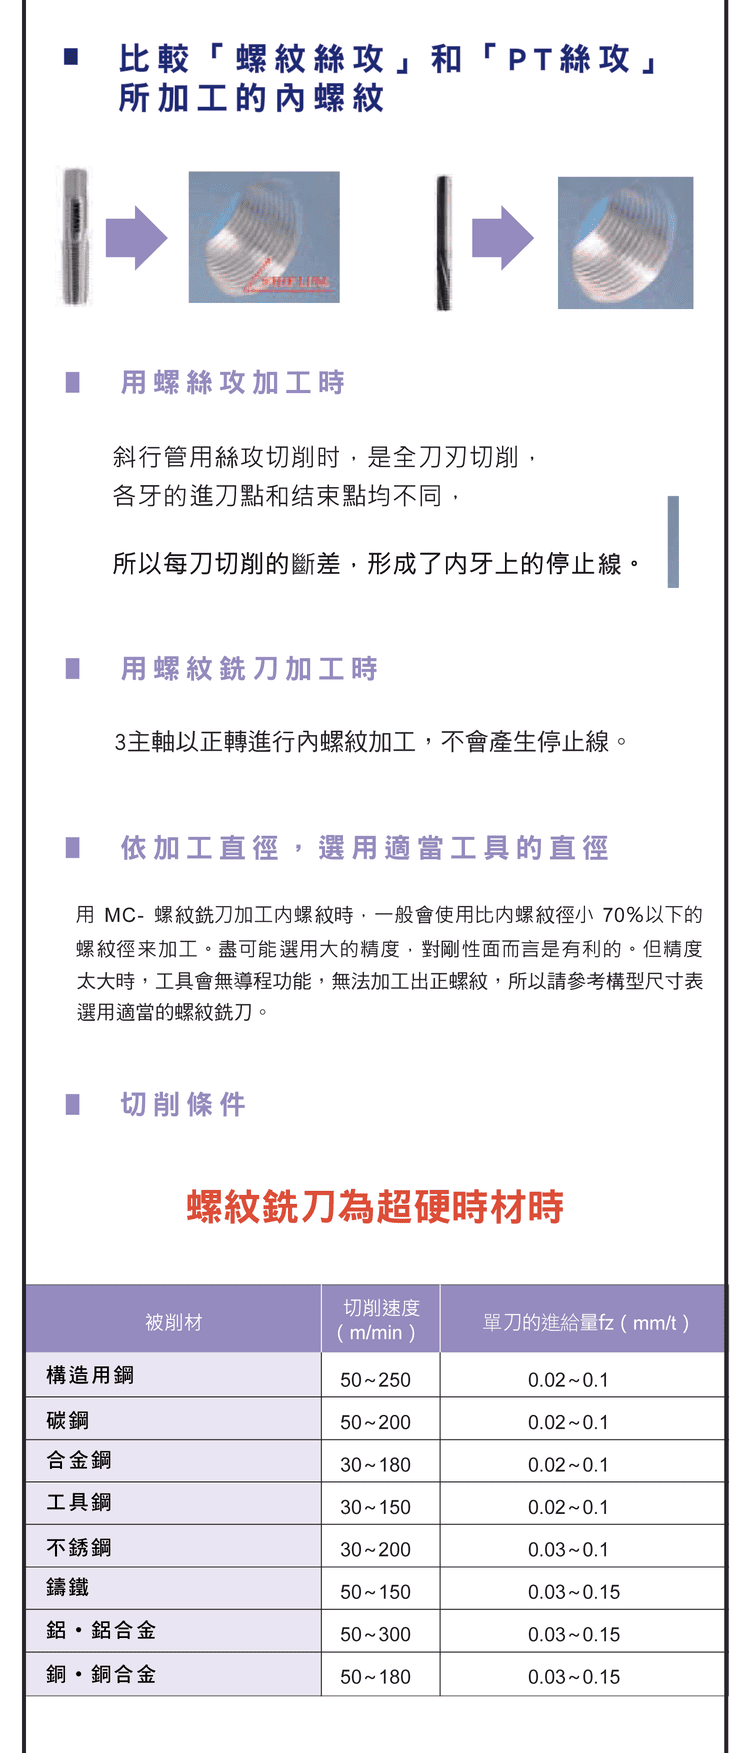
2. Thread Milling vs Tapping
| Item | Tap | Thread mill |
|---|---|---|
| Cutting | Full-edge contact | Helical feed, progressive |
| Stop line | Prone to internal stop line | None |
| Breakage risk | Higher | Lower, more stable |
| Best for | Fast work, standard threads | Precision, high-value parts, big diameters |
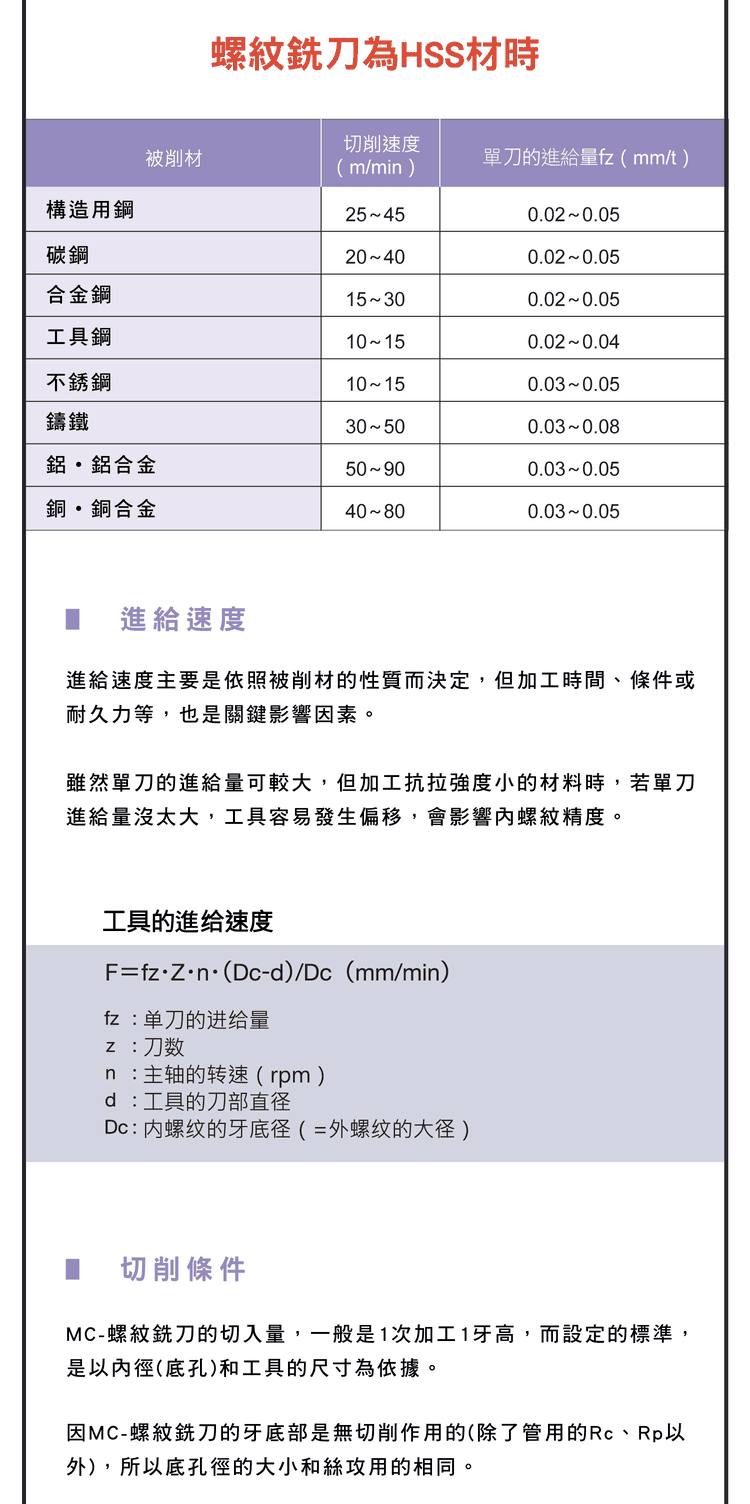
3. Hand of Thread and Tool Selection
Right-hand threads turn clockwise, left-hand counter-clockwise, with opposite feed, all set by the CNC program — one tool cuts both. Tool-diameter rule:
| Rule | Description |
|---|---|
| Tool dia < 70% of thread dia | Raises rigidity, keeps cutting space, avoids interference |
| Tool dia too large | Cannot form a complete thread |
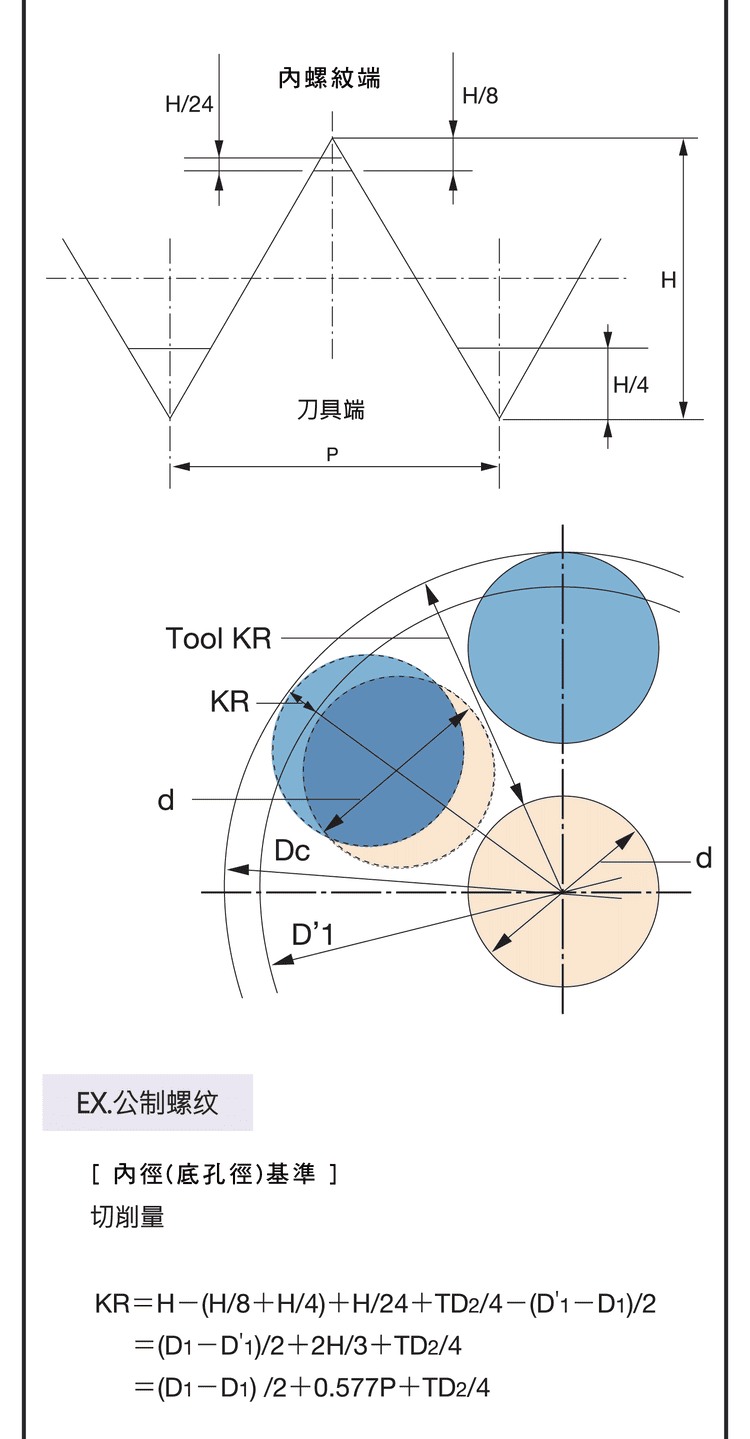
4. Cutting Conditions (Reference)
Reference cutting-speed ranges for a carbide thread mill; follow the tool maker's catalog for actual values:
| Material | Cutting speed (ref., m/min) |
|---|---|
| Structural steel | about 50–250 |
| Carbon steel | about 50–200 |
| Alloy steel | about 30–180 |
| Stainless | about 30–200 |
| Cast iron | about 50–150 |
| Aluminium alloy | about 50–300 |
Feed per tooth about 0.02–0.15 mm/t (reference); carbide runs at roughly 3-6 times the HSS speed (i.e. HSS is about 1/3 to 1/6 of carbide).
※ These are thread-mill reference values — follow the tool maker's catalog, material and machine; do not apply directly.
5. Selection Advice
Thread mills suit precision, high-value parts, large diameters, deep holes or hard materials where a broken tap is hard to remove, and cases needing left/right flexibility; for standard-thread production where speed matters, a tap is still faster. Confirm pitch, thread diameter and hand, then choose by the diameter rule and material.
For forms and codes see the Thread Designation Chart and Standard Thread Form Guide; for the tool overview see the Thread Tool Chart; for sizes see the Thread Size Chart.
6. When the Thread Comes Out Wrong: What to Check First
In thread milling one symptom often has several causes. Check the most likely ones in the table first (per the EMUGE thread-milling troubleshooting chart):
| Symptom | Check and adjust |
|---|---|
| Chatter, poor finish | Stiffen workholding and machine, shorten overhang, use a higher helix tool; then fine-tune speed and feed per tooth |
| Fast wear | Lower cutting speed, raise feed per tooth, add a coating (TiN, TiCN), switch to climb milling |
| Chipping | Lower feed per tooth, add rigidity, add a coating, switch to climb milling |
| Tapered thread, gauge tighter deeper in (drill-thread-mill tool) | Lower feed per tooth, check the helix angle |
| Marks at the entry (drill-thread-mill tool) | Stiffen the workpiece and tool setup |
Two general rules: lack of rigidity has to be ruled out for every symptom; climb milling helps only with wear and chipping, not with chatter or finish. So with a poor finish, do not jump to changing the speed — if holding and overhang are not fixed, it comes back whatever the speed.
FAQ
Q: Thread mill or tap?
For high precision, big diameters, left/right flexibility, or where a broken tap is hard to remove, choose a thread mill; for standard-thread production focused on speed and cost, a tap is faster and cheaper. Decide by precision, diameter and production type.
Q: Why can one thread mill make several diameters?
Thread milling traces the thread by CNC helical interpolation: the pitch comes from the cutter's tooth form and the diameter from the program path. As long as the pitch matches, one tool can mill internal threads of different diameters.
Q: How big should the tool be?
Keep the tool diameter below 70% of the thread diameter to preserve cutting space, avoid interference and raise rigidity. Too large can't form a full thread; too small lacks rigidity and takes longer.
Q: What is an internal stop line?
When a tap reverses out, the flank often leaves a joining mark (stop line) that affects fit and appearance. Thread milling forms with continuous helical feed and leaves no stop line, so the thread is smoother and tighter.
Last updated: 2026-10-12
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.









