
Thread Tool Chart: Taps, Dies & International Standards
This guide organizes thread-tool specifications — straight-flute taps, spiral-flute taps, machine taps, dies and related cutting tools — mapped to JIS, ISO, ANSI, BS and DIN standards. Classifying the tools and their specs helps you quickly pick the right tapping tool and method for CNC machining, tapping processes and mechanical design, a key basis for efficiency and accuracy.
1. Taps (Internal-Thread Tools)
| Tap type | Traits and use |
|---|---|
| Straight-flute tap | Metric coarse/fine, imperial, parallel pipe; versatile, hand or machine tapping |
| Spiral-flute tap | Good chip evacuation, lifts chips out; suits blind holes |
| Spiral-point tap | Good lead-in, pushes chips forward; suits through holes |
| Machine tap | For high-speed work; common on CNC |
| Long-shank tap | For deep holes; improves stability |
| Bent-handle / collet tap | Bent-handle for manual low speed; collet for specific sizes or repair |
| Pipe-thread tap | Taper/parallel pipe; dry-seal taps for NPT/NPTF, sealing-focused |
2. Dies (External-Thread Tools)
| Die type | Description |
|---|---|
| Round die (metric) | Metric coarse/fine, adjustable or fixed |
| US die | UNC/UNF, adjustable and fixed types |
| Hex die | For quickly re-chasing external threads |
※ Dies cut external threads and are one category in this chart; internal threads use taps.
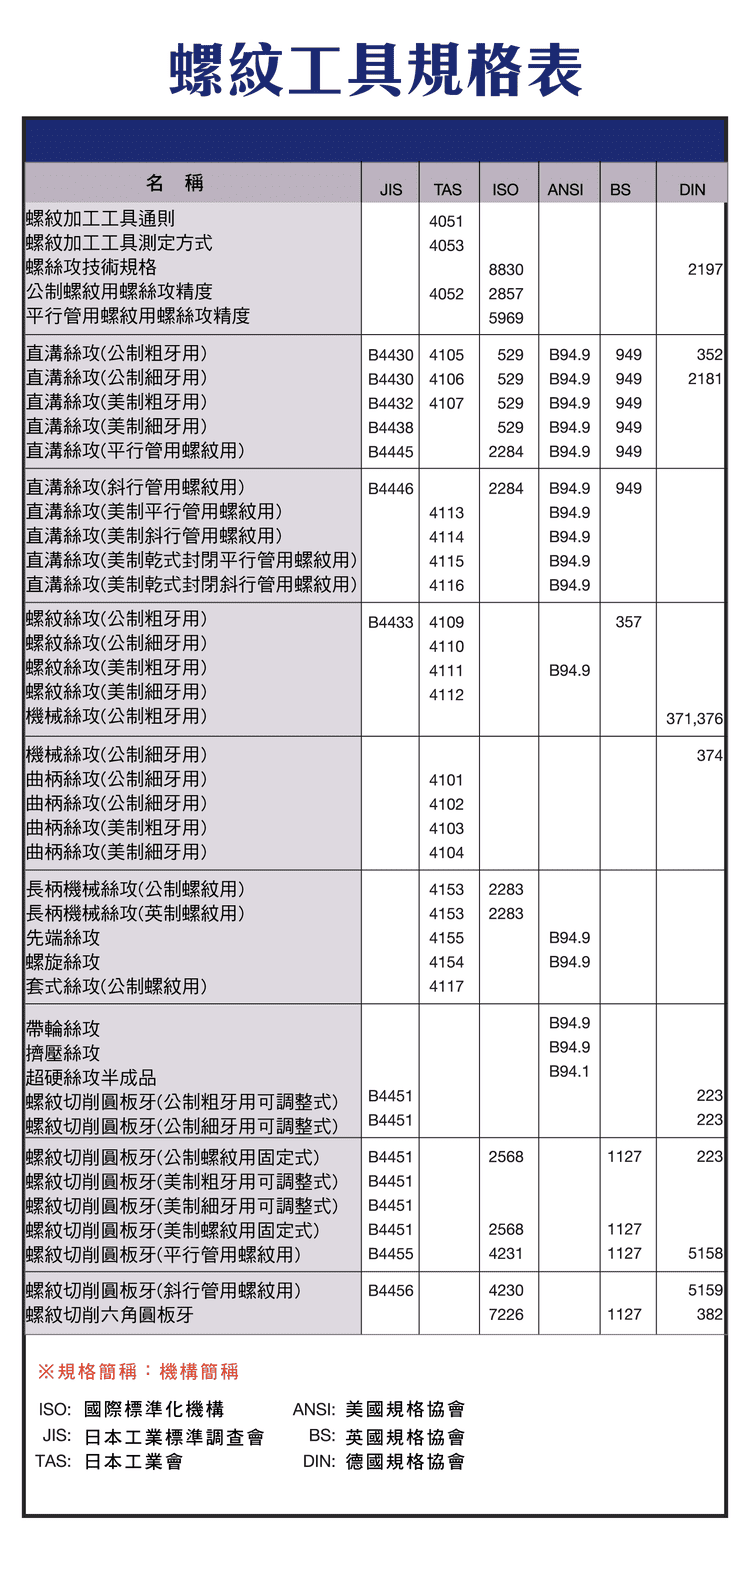
3. International Standards
| Standard | Body |
|---|---|
| ISO | International Organization for Standardization |
| JIS | Japanese Industrial Standards |
| ANSI | American National Standards Institute |
| BS | British Standards |
| DIN | German standards |
Use for cross-border comparison, tool-selection basis and standard alignment.
4. How to Choose a Tap: Follow This Order
Do not start from the product list; narrow it down step by step in the order below, and each step has its own guide.
| Step | Ask first | Which way to go |
|---|---|---|
| 1 | Workpiece material and hardness | Aluminium, copper and austenitic stainless can take form taps; cast iron needs a cutting tap. See Cutting Tap vs Forming Tap (Roll Tap) |
| 2 | Through or blind hole | Blind holes take spiral-flute taps; through holes take spiral-point or straight-flute taps. See Spiral Point Tap Guide |
| 3 | Thread accuracy | Pick the P grade for the fit; for shrinking material or plating, go oversize. See Tap Thread Tolerance Guide |
| 4 | Machine feed and holder | With synchronised feed use a rigid or synchronised holder; without it, use a floating holder and slow down. See Tool Holders for Tapping |
| 5 | Cutting speed | General-purpose taps at normal speed, high-speed taps for high-speed work. See Tap Cutting Speed Guide |
| 6 | Other conditions | Non-water-soluble oil with oxide-treated taps; titanium-coated taps for mass production. See Tap Surface Treatment Guide |
Then match the product: pipe taps (NPT/PT) for sealed piping, see Pipe Tap Guide; dies for external threads; for carbide versus HSS see Carbide Tap Guide; for codes and standards see Thread Designation Chart.
FAQ
Q: Straight-flute, spiral-flute or spiral-point tap?
Straight-flute is versatile for hand or machine; blind holes use spiral-flute (chips lift out); through holes use spiral-point (chips push forward). Choosing by hole type and chip direction best avoids breakage and torn threads.
Q: Machine tap vs hand tap?
Machine taps are designed for machine/CNC high-speed tapping with geometry and coating for continuous work; hand taps (e.g. bent-handle) are for low-speed manual use, field repair or small runs. Their parameters and holding differ.
Q: Difference between a die and a tap?
A tap cuts internal threads (inside a hole); a die cuts external threads (onto a rod). They are the internal/external counterparts — choose by whether you're making an internal or external thread.
Q: Why cross-reference ISO/JIS/ANSI/DIN?
Different national standards define thread and tool sizes, tolerances and codes slightly differently. Cross-referencing during cross-border purchasing or machining keeps tool and workpiece specs consistent and avoids incompatibility or assembly issues.
For the full reading guide on this topic, see Thread Machining: A Complete Reading Guide.
Published: 2026-03-24 | Last updated: 2026-10-31









