
Turning Troubleshooting Guide | Tool Wear, Accuracy and Surface Issues
When a turning job goes wrong, identify the symptom before changing anything: one symptom can have several causes, each with a different fix. This guide routes wear, chips, dig-in, ripples and taper, grooving, threading and surface finish to their dedicated guides, then gives a check order for the two most common problems, chatter and drifting size, starting with the cheapest and quickest checks.
1. Why Not Just Swap the Insert
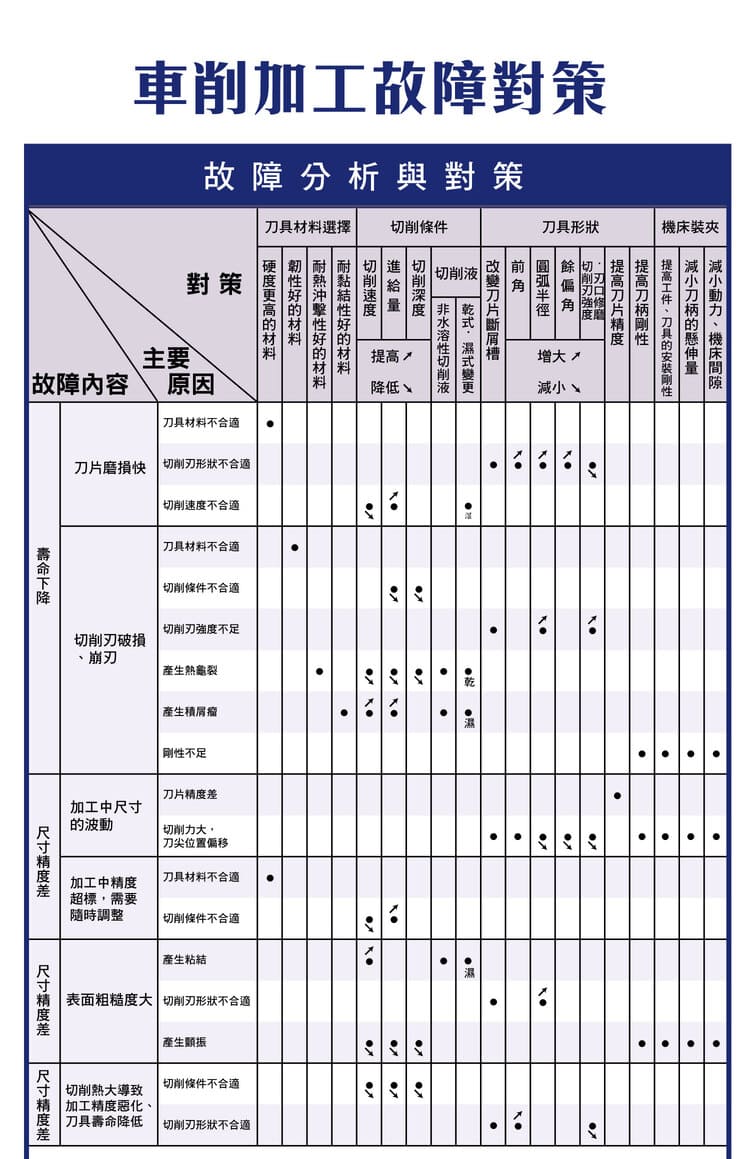
The usual first reaction to a turning problem is to try a new insert. A maker’s troubleshooting matrix, however, sorts remedies into four groups — tool material, cutting conditions, tool geometry and machine/clamping — and one symptom often has several causes whose remedies point in opposite directions. Take fast insert wear: a wrong grade calls for a harder grade; a wrong edge shape calls for a different chipbreaker, a larger rake angle or nose radius; a wrong cutting speed calls for lowering the speed while raising the feed. Identify the cause first, then decide which group to adjust.
2. Find the Right Guide by Symptom
The table routes each symptom to its dedicated guide; chatter and drifting size are covered in sections 3 and 4 of this guide.
| Symptom | Where to look |
|---|---|
| Fast insert wear, chipping, built-up edge | Tool Wear Guide: Chipping, BUE & Thermal Crack Solutions |
| Long chips tangling, or chips too fine | Turning Chip Control Guide: Chip Breaker & Cutting Conditions |
| Tool suddenly digs into the part | How to Prevent Tool Dig-In on a Lathe: Leadscrew Backlash, Quadrant Changes and Lead Angle Choice |
| Regular ripples, taper, uneven pitch | Lathe Accuracy and Troubleshooting: Taper, Ripples and Uneven Pitch Point to the Machine |
| Parting or grooving problems | Parting and Grooving Troubleshooting: Wear, Surface, Chip Breaking and Vibration |
| Poor threads | Thread Machining Troubleshooting Guide: CNC Turning Fixes |
| Cannot reach the target roughness | Surface Finish: A Complete Reading Guide |
| Chatter marks | Section 3 of this guide |
| Size drifts larger or smaller | Section 4 of this guide |
3. How to Cure Chatter
Chatter has no single-knob fix: in the maker’s matrix it is the only symptom that calls for lowering speed, feed and depth together while raising rigidity across the board. Start with the cheapest, quickest checks:
| Order | What to check and change |
|---|---|
| 1. Overhang and clamping | Shorten the overhang and use a thicker shank; for bores use a damped or carbide bar, and lengthen the clamping length if it is short |
| 2. Tool height | Check the tip height against the part centre; for OD work it may sit slightly above centre against vibration, but facing needs it exactly on centre |
| 3. Nose radius | If it is too large, go one size smaller |
| 4. Entering angle | For vibration from high radial force, use a holder with an entering angle close to 90°, i.e. a lead angle close to 0° |
| 5. Edge and chipbreaker | Use a sharper, positive-rake chipbreaker or a thin-coated/uncoated insert; if flank wear is high, use a more wear-resistant grade or lower the speed |
| 6. Cutting conditions | Lower speed, feed and depth together; but if the depth is so small that the cutting force is unstable, increase it slightly |
Lowering the parameters without fixing overhang and clamping usually lets the chatter come back. For cross-process diagnosis see the Vibration and Chatter: A Complete Reading Guide.
4. When Size Drifts Larger or Smaller
First tell a slow drift from a sudden jump. Studies cite thermal error as 40–70% of a machine tool’s total error and the main source of part error, and acceptance rules require temperature-related accuracy to be measured only after the machine has warmed up and stabilised — a cold machine and a warm one will not cut the same size.
| What you see | Check first |
|---|---|
| Size keeps drifting after start-up, or differs between morning and afternoon | Thermal deformation: warm the machine up until stable before setting and cutting; abnormal spindle-bearing heat needs the machine checked |
| Size creeps in one direction as parts accumulate | Insert wear: measure flank wear and index the edge when it is due |
| An occasional sudden jump | Tool position shift or loose clamping: check insert and holder locking and workholding |
For checking the machine and tracing thermal problems see Checking a CNC Lathe's Accuracy and Tracing Its Faults: 18 Tests and the Outside-In Rule. For a bore that keeps coming out larger or smaller, see Boring on the Lathe: Setting Tool Angles and Why the Bore Grows or Shrinks.
5. Fuzzy Surfaces and Burrs
| Symptom | Cause | Remedy |
|---|---|---|
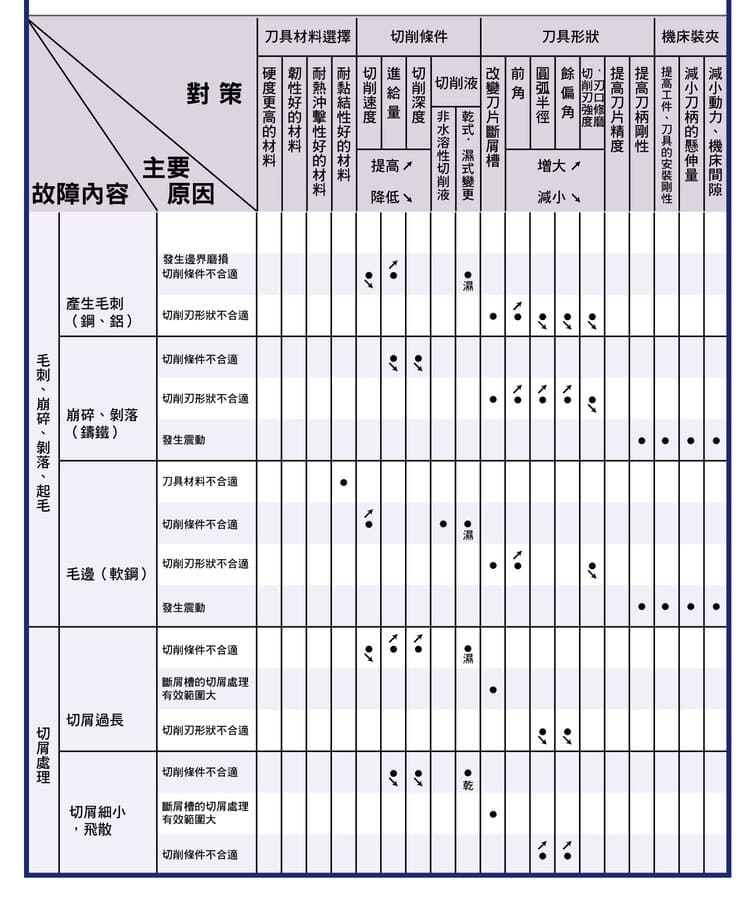
| Fuzzy, torn surface | Chips hit the machined face | Use a chipbreaker that steers chips away; reduce the depth |
| Fuzzy, torn surface | Notch wear on the edge | Use a grade with better oxidation-wear resistance (e.g. cermet); lower the speed |
| Rough surface with clear feed marks | High feed with a small nose radius | Use a wiper insert or a larger nose radius, or lower the feed |
| Burr at the end of the cut | Edge not sharp enough | Use a sharp edge (PVD-coated or ground) |
| Notch wear or chipping at the depth line | — | Use a holder with a smaller entering angle and exit the part on a chamfer or radius |
For measuring and comparing roughness see the Surface Roughness Chart by Process.
FAQ
Where should I start when a turning job goes wrong?
Identify the symptom, then the cause: one symptom can come from the grade, the geometry or the cutting conditions, each with a different fix. Wear and chipping go to the tool wear guide, chips to chip control, and regular ripples or taper to machine accuracy first; follow sections 3 and 4 of this guide for chatter and drifting size.
What do I do about chatter marks on OD turning?
Start with the cheapest checks: shorten the overhang and check tool height, then go one size smaller on the nose radius and use a holder with an entering angle close to 90°; only then lower speed, feed and depth together. Lowering the parameters without fixing rigidity usually lets the chatter return.
Why is the size different in the morning and the afternoon?
Usually thermal deformation: studies cite thermal error as 40–70% of a machine tool’s total error. Let the machine warm up until stable before setting and cutting; if the size instead creeps in one direction as parts accumulate, check insert wear first.
Inserts wear too fast — should I just change the grade?
Not necessarily. The maker’s matrix splits fast insert wear into three causes: a wrong grade needs a harder grade; a wrong edge shape needs a different chipbreaker or a larger rake angle or nose radius; a wrong cutting speed needs a lower speed together with a higher feed. Find out which one applies before acting.
For the full reading guide on this topic, see Surface Finish: A Complete Reading Guide.
For the full reading guide on this topic, see Turning: The Complete Guide.
Published: 2026-03-25 | Last updated: 2026-10-22









