
Drill Flute Length vs Rigidity: Choosing the Best Flute
How long a flute should the drill have? This guide helps you decide: measure the hole depth first, then work out how much allowance chip evacuation needs, and take the shortest one that will still do the job. How flute length relates to rigidity, how that runs through into vibration, wear and hole accuracy, and the rules for flute design are all here, so you can set the spec yourself.
For the length-class breakdown (stub, standard, long) and depth-to-diameter ratios, see Jobber, Stub and Taper Length Drill Bits.
1. Flute Length vs Rigidity
| Flute length | Rigidity and effect |
|---|---|
| Longer | Lower rigidity, prone to vibration/runout, unstable cut |
| Shorter | Higher rigidity, stable cut, longer life |
2. Flute Length vs Tool Life
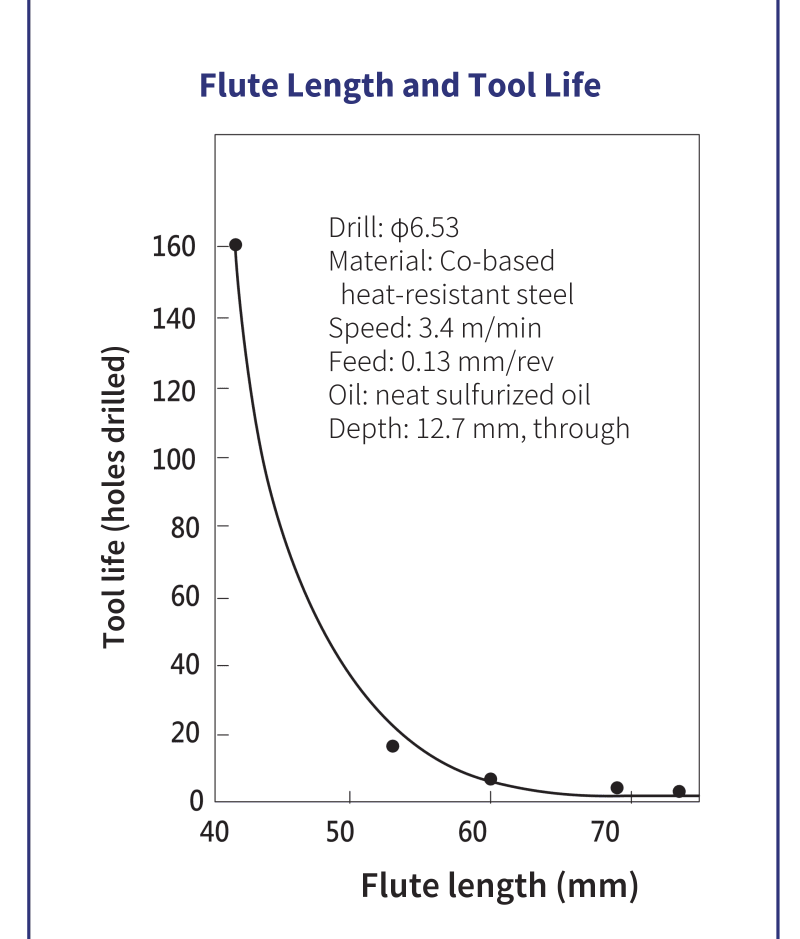
A longer flute lowers rigidity and destabilizes the cut, shortening tool life. The following are manufacturer example test conditions:
| Item | Condition (mfr. example) |
|---|---|
| Drill | φ6.53 |
| Material | Cobalt-based heat-resistant steel |
| Cutting speed | approx. 3.4 m/min |
| Feed | approx. 0.13 mm/rev |
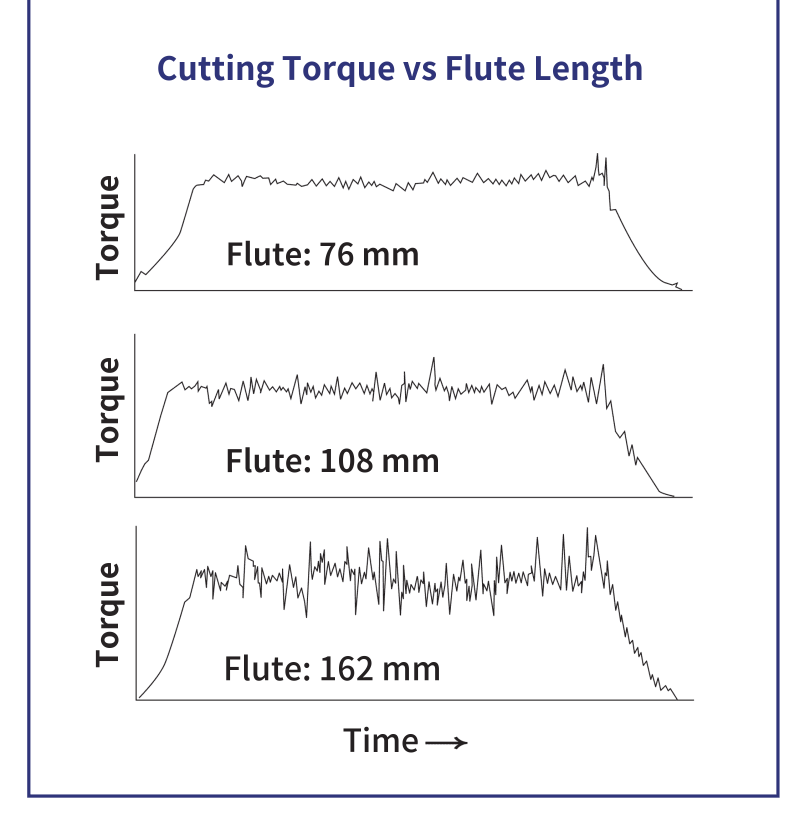
Result: the number of holes drilled falls steeply as flute length grows — about 160 holes at roughly 42 mm of flute, and almost none beyond 70 mm. A second manufacturer chart on the same page compares cutting torque at 76, 108 and 162 mm of flute (no test conditions are given for it): the longer the flute, the more the torque fluctuates (chart below). This is a manufacturer example under specific conditions, not a general specification, but the direction holds: keep the flute only as long as the job needs.
3. Flute Design and Evacuation Allowance
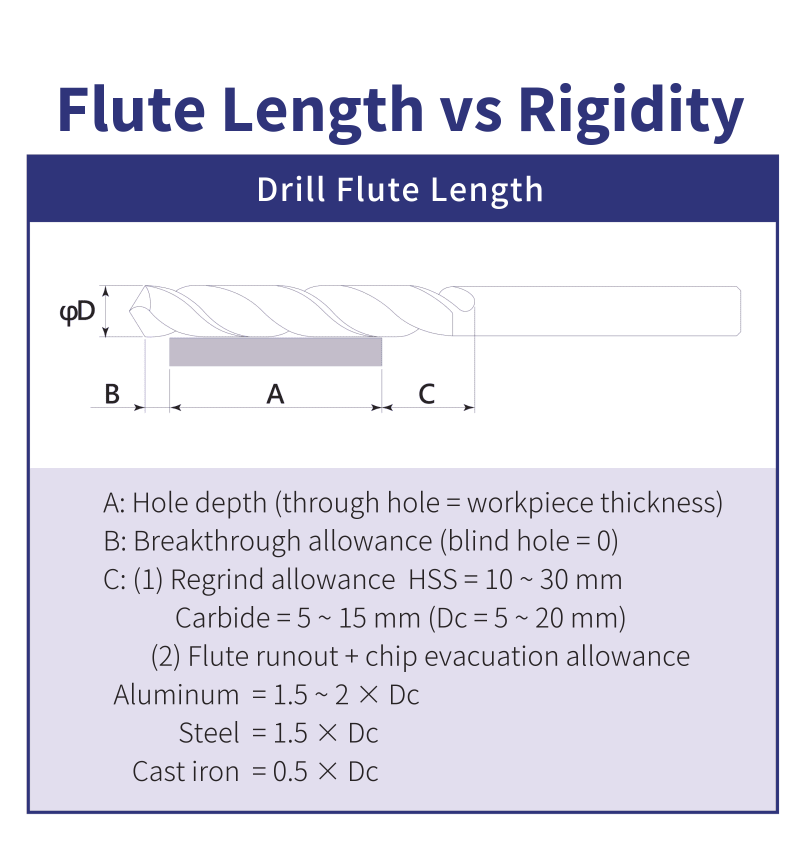
Effective flute length = A + B + C. A is the hole depth (the workpiece thickness for a through hole); B is the breakthrough allowance that lets the point fully exit a through hole, zero for a blind hole; C is the regrind allowance plus the evacuation allowance. Regrind allowance depends on drill material: about 10–30 mm for HSS and about 5–15 mm for carbide (at 5–20 mm diameter). Common evacuation-allowance guidance by material:
| Material | Evacuation allowance (ref.) |
|---|---|
| Aluminum | approx. 1.5–2 × Dc |
| Steel | approx. 1.5 × Dc |
| Cast iron | approx. 0.5 × Dc |
4. Material Hardness vs Life
The harder the material, the lower the cutting speed must be to keep the same tool life. What is easy to miss is that one steel grade still varies in hardness within its allowed range, and that variation alone can split tool life. In one manufacturer test (φ16 HSS drill in SK7, 60 mm through hole), the harder batch (HB 222–225) drilled clearly fewer holes at the same feed than the softer batch (HB 200–210). When life suddenly drops after a new batch of material, check its hardness first, and leave margin in the conditions rather than setting them from the nominal hardness alone. For setting conditions, see the Drilling Parameters Guide.
5. Optimization Tips
| Tip | Note |
|---|---|
| Shortest usable flute | Prefer it, allowing for depth and evacuation |
| Avoid over-length | Long drills vibrate, hurting accuracy and life |
| Deep-hole pairing | Use rigid tools and proper conditions, or an internal-coolant deep-hole drill |
For deep-hole evacuation and guiding design, see the Deep Hole Drill Guide.
6. Common Mistakes
Common mistakes: over-choosing long-flute drills, ignoring evacuation space, and disregarding tool rigidity — all amplify vibration and runout and lower both accuracy and tool life.
FAQ
Q: Is a longer flute always better?
No. A longer flute lowers rigidity and is prone to vibration and runout, hurting accuracy and life. Choose the shortest effective flute that still fits the hole depth and evacuation allowance.
Q: How do I size the flute length?
Effective flute = hole depth + breakthrough allowance (through holes only) + regrind allowance + evacuation allowance. Evacuation reference: aluminum ~1.5–2×Dc, steel ~1.5×Dc, cast iron ~0.5×Dc.
Q: Do deep holes require long-flute drills?
Deep holes need enough flute, but long flutes lack rigidity. Prefer a rigid internal-coolant deep-hole drill and locate with a pilot drill to balance flute need and stability.
Q: Does harder material always shorten drill life?
Broadly yes: the harder the material, the lower the cutting speed needed for the same life. And even within one steel grade's allowed hardness range, a harder batch can last clearly less, so check hardness first when life drops after a material change.
For the full reading guides on this topic, see Tool Life and Wear: A Complete Reading Guide and Chip Control: A Complete Reading Guide.
This article is part of Drill Bits: The Complete Guide - Start From Depth-to-Diameter, Then Pick the Drill and Set the Conditions; that guide shows how the whole topic fits together.
Published: 2026-03-19 | Last updated: 2026-10-21









