
End Mill Length vs Deflection
An end mill's length and bending resistance directly affect machining stability and tool life. The longer the overhang, the more deflection rises—by a multiple—sharply reducing breakage life: doubling the length can increase deflection by 8×, greatly raising the fatigue-failure risk. Controlling length, improving rigidity and optimizing cutting conditions effectively reduces vibration and tool breakage.
The Length–Deflection Relationship
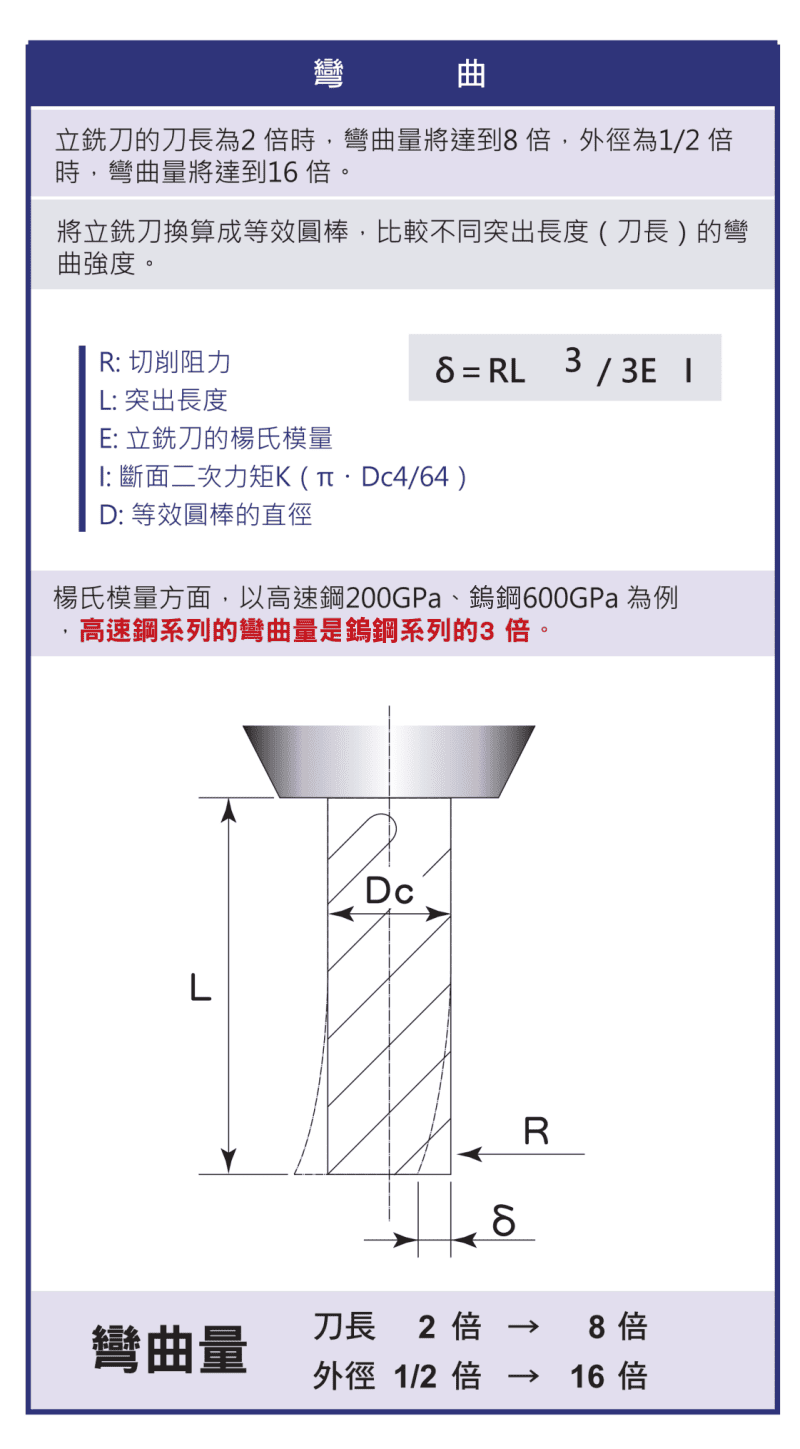
Modeling the end mill as an equivalent cylinder, deflection is:
δ = R × L³ ÷ (3EI)
| Item | Description |
|---|---|
| R | cutting resistance |
| L | tool overhang length |
| E | Young's modulus of the end mill |
| I | second moment of area (I = π × Dc⁴ ÷ 64, where Dc is the equivalent cylinder diameter) |
Key point: deflection is cubically proportional to length (L³).
Effect of Length on Deflection & Life
| Item |
|---|
| 2× length → about 8× deflection |
| Half the diameter → about 16× deflection |
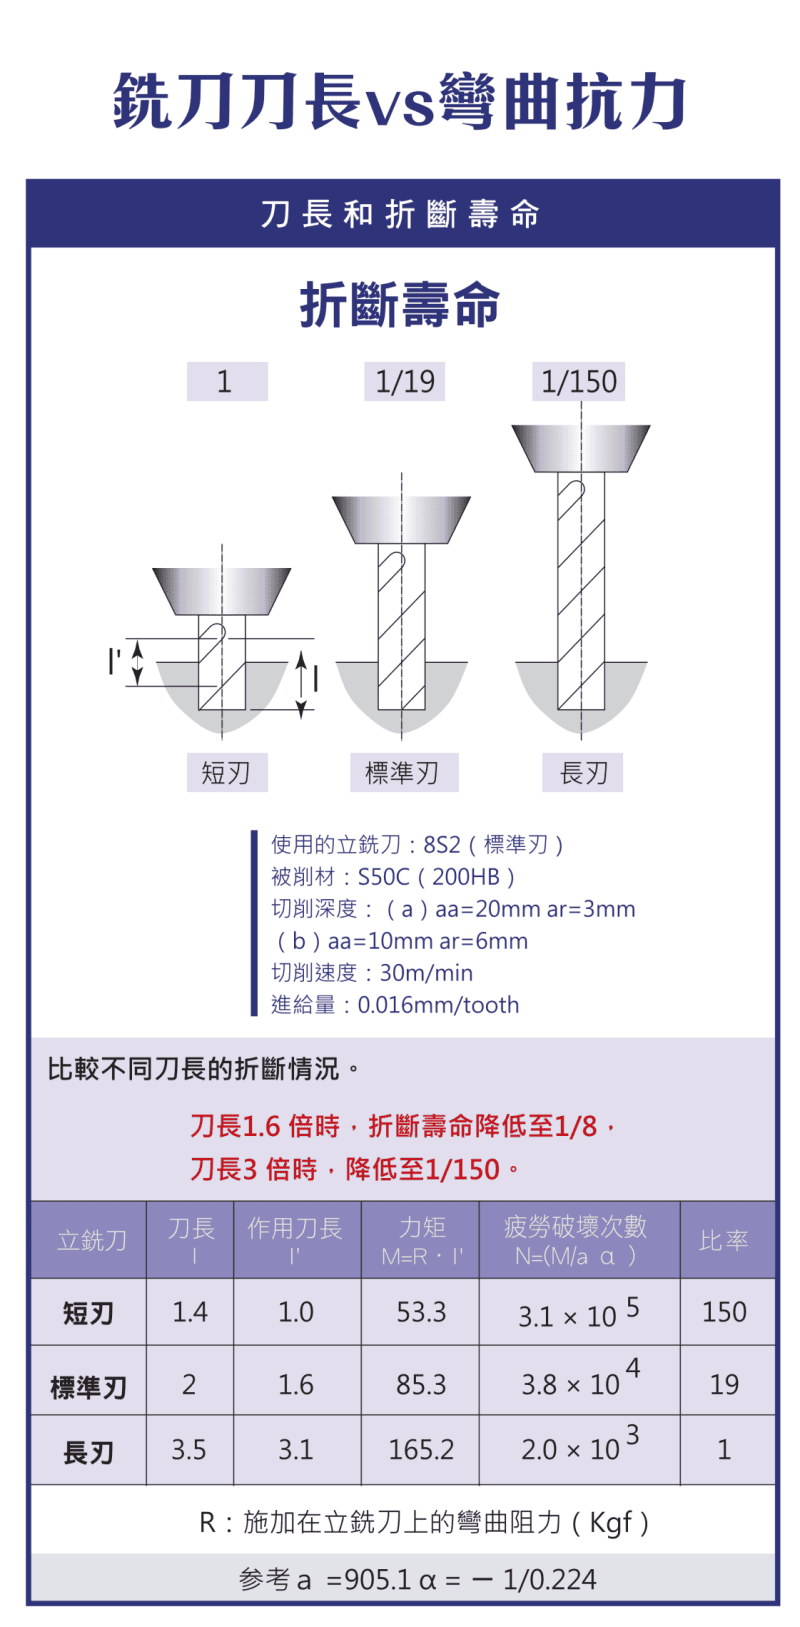
| Breakage life: 1.6× length → about 1/8; 3× length → about 1/150 |
Manufacturer test (end mill 8S2 standard flute, workpiece S50C 200HB, cutting speed 30 m/min, feed 0.016 mm/tooth), breakage-life comparison:
| End mill | Length I | Effective length I' | Moment M=R·I' | Fatigue cycles N | Ratio |
|---|---|---|---|---|---|
| Short flute | 1.4 | 1.0 | 53.3 | 3.1×10⁵ | 150 |
| Standard flute | 2 | 1.6 | 85.3 | 3.8×10⁴ | 19 |
| Long flute | 3.5 | 3.1 | 165.2 | 2.0×10³ | 1 |
Cutting Length & Fatigue Failure
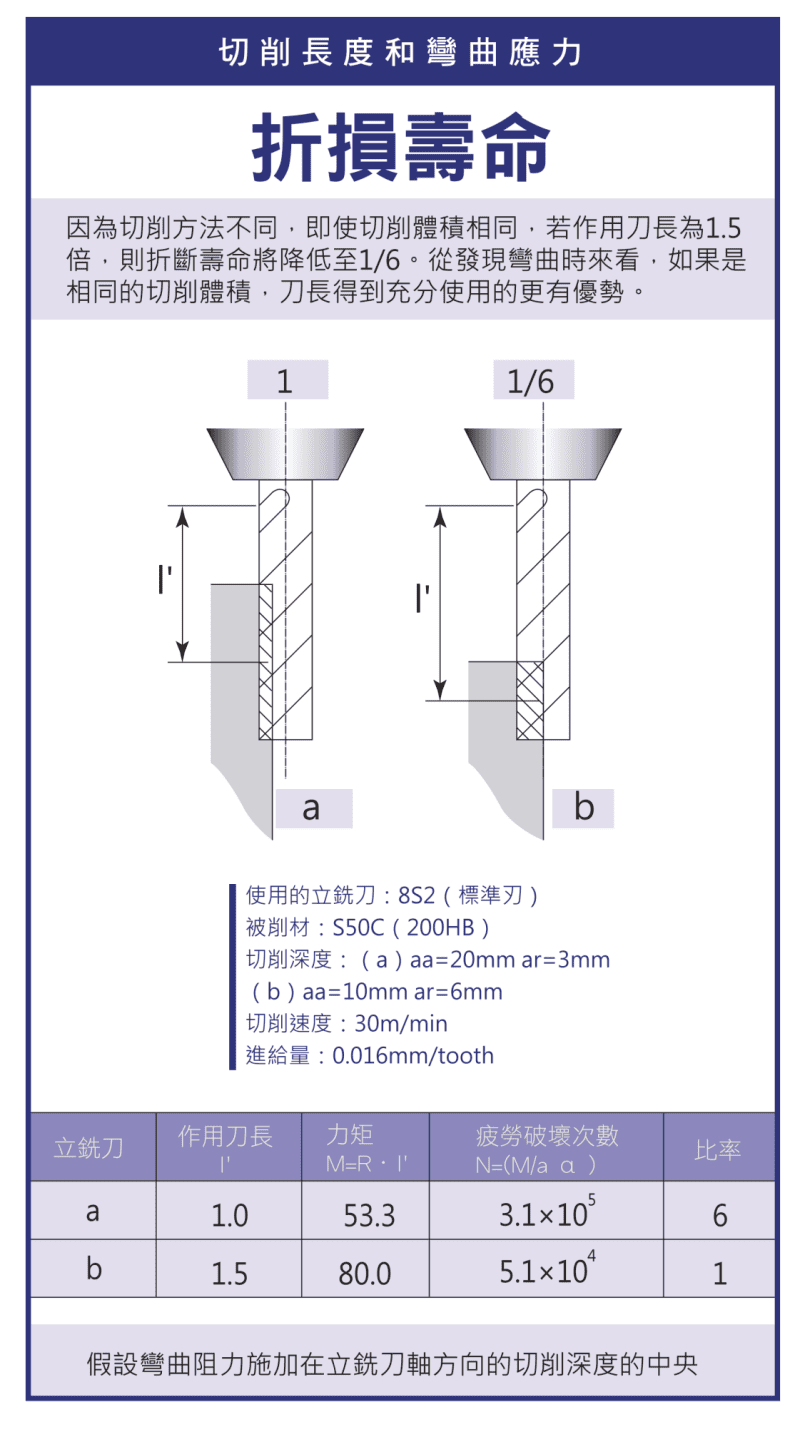
For the same cutting volume, a longer effective length raises bending stress and sharply lowers breakage life—e.g. a 1.5× effective length drops breakage life to about 1/6. In other words, for the same cutting volume, fully using the flute (shorter overhang) is advantageous.
| Case | Effective length I' | Moment M=R·I' | Fatigue cycles N | Ratio |
|---|---|---|---|---|
| a | 1.0 | 53.3 | 3.1×10⁵ | 6 |
| b | 1.5 | 80.0 | 5.1×10⁴ | 1 |
Extending Reach: Choosing a Long-Neck End Mill (Neck Length and Pencil Necks)
To reach deep with a small-diameter cutter, shops often use a long-neck end mill: the flute stays short and the reach comes from a reduced-diameter neck. Check these four things when choosing one.
| What to check | How to judge | Manufacturer example |
|---|---|---|
| Neck length | Take the shortest that still reaches the depth; rigidity falls much faster than the neck length grows | Same series: a 4 mm neck has 2.78 times the static rigidity of a 6 mm neck |
| Neck shape | At the same neck length, a pencil neck (a tapered neck narrowing toward the tip) is stiffer than a straight neck—do not judge by looks | A 0.9° pencil neck has 1.33 times the static rigidity of a straight neck of the same length |
| Length grade | Standard series often come in short, medium, long and extra-long reach; short is the strongest and stiffest, extra-long is for deep cavities and high shoulders | — |
| How to compare | Divide the two tools’ deflection indexes to get the rigidity ratio; compare only within one catalog, never across brands | — |
The two ratios come from deflection indexes in the MOLDINO catalog and show the order of magnitude; choose by the catalog you actually use. Whether the flute itself should have back taper is covered in Do You Need an End Mill With Back Taper: When It Pays and When It Is Wasted Money. For how to compare long-neck end mills from two brands side by side, see Comparing Cutting Tool Brands: Which Spec Fields Line Up, and Which Only Count Within One Catalog.
Effect of Material on Deflection
Young's modulus: HSS about 200 GPa, carbide about 600 GPa. Under the same conditions, HSS deflects about 3× as much as carbide—carbide is stiffer.
Tips for Machining Stability
| Item | Description |
|---|---|
| Tool selection | prefer a short tool length; increase tool diameter. |
| Cutting conditions | reduce cutting load; control depth of cut. |
| Equipment & holding | increase clamping rigidity; minimize tool overhang. |
The effective holding length at the collet end also affects deflection—see Collet Damage & Deformation.
Practical Length-Control Principles
| Item |
|---|
| Keep tool overhang as short as possible |
| Avoid excessively long overhang machining |
| Reduce parameters when machining with long tools |
FAQ
Why does a longer tool break more easily?
Deflection is cubically proportional to length (δ∝L³), so 2× length gives about 8× deflection; breakage life drops accordingly (1.6× length → about 1/8, 3× → about 1/150).
How much does diameter affect deflection?
Deflection is inversely proportional to the fourth power of diameter—halving the diameter gives about 16× deflection. Increasing tool diameter is one of the most effective ways to add rigidity.
Which is stiffer, HSS or carbide?
Carbide's Young's modulus is about 600 GPa vs HSS about 200 GPa; under the same conditions HSS deflects about 3× as much, so carbide is stiffer.
How do I reduce tool deflection and breakage?
Prefer a short tool length, increase tool diameter, improve clamping rigidity and minimize overhang; reduce cutting load and parameters when long-overhang machining is unavoidable.
This article is part of End Mills: The Complete Guide - Know the Cutter, Choose It, Set the Conditions; Toolpaths Are Another Line; that guide shows how the whole topic fits together.
Published: 2026-03-18 | Last updated: 2026-10-29









