
End Mill Selection Guide
An end mill's shape directly affects how it cuts and the resulting quality. Different types—square, corner-radius, ball nose and tapered end mills—suit slotting, surface machining, deep milling and counterboring respectively. Choosing the right shape improves chip evacuation, lowers cutting force and improves accuracy. This article focuses on choosing a cutter by machining operation; to first understand each type's construction and features, see End Mill Types and Features.
Matching End Mill Shape to Machining Operation
Different end mill shapes suit different operations. Common operations include slotting, side milling, corner R, deep milling, surface machining and counterboring. Choosing the right tool improves efficiency and stability. The table below summarizes the suitable tool and characteristics for each operation for quick reference.
| Operation | Suitable tool | Characteristics |
|---|---|---|
| Slotting, side milling | Square end mill | High cutting efficiency, ideal for right-angle and flat machining, well suited to general slotting and side milling |
| Corner R machining | Corner-radius end mill | Machines corner transitions, reduces stress concentration and improves part durability |
| Deep milling | Square end mill (roughing end mill as an extension) | Requires good chip-evacuation space and controlled length-to-diameter ratio to avoid vibration and tool breakage |
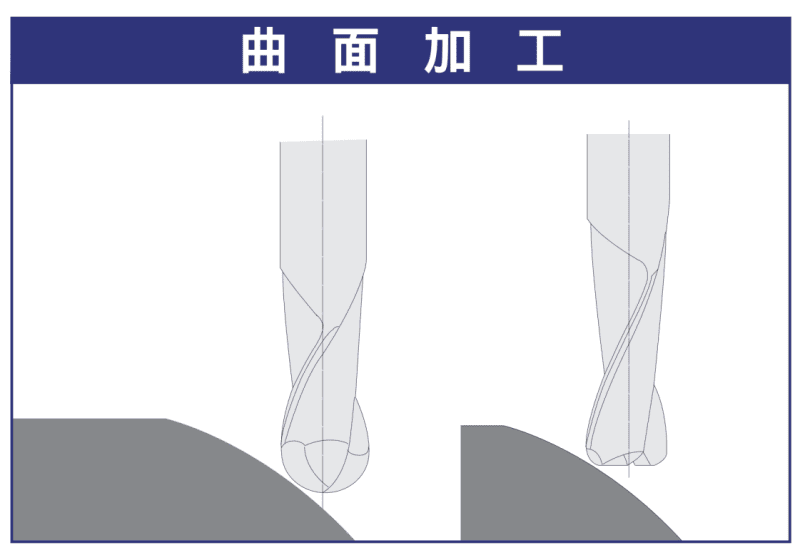
| Surface (curved) machining | Ball nose end mill | Suited to 3D surfaces and mold machining, enabling contour and profile milling with good surface quality |
| Counterbore machining | Tapered end mill, tapered ball nose end mill | Suited to draft slopes and tapered cavities; the tool’s taper forms the slope |
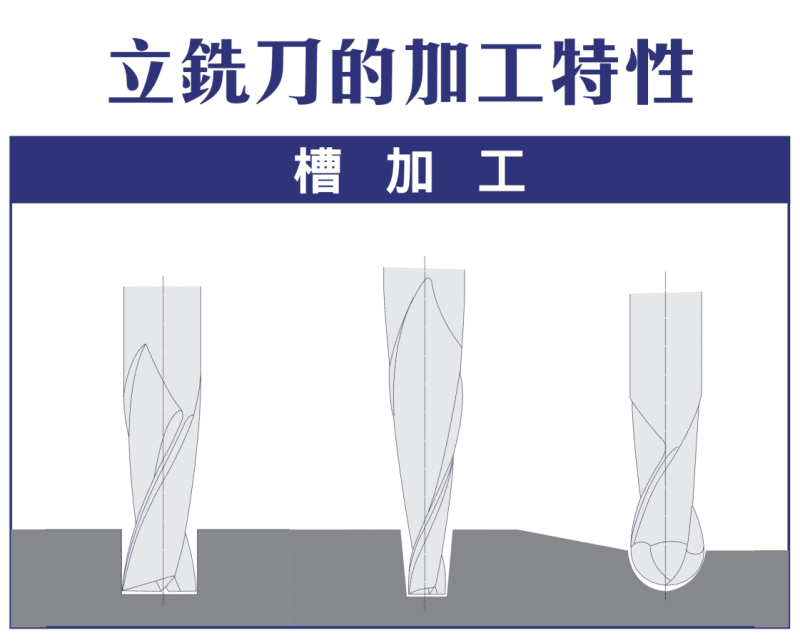
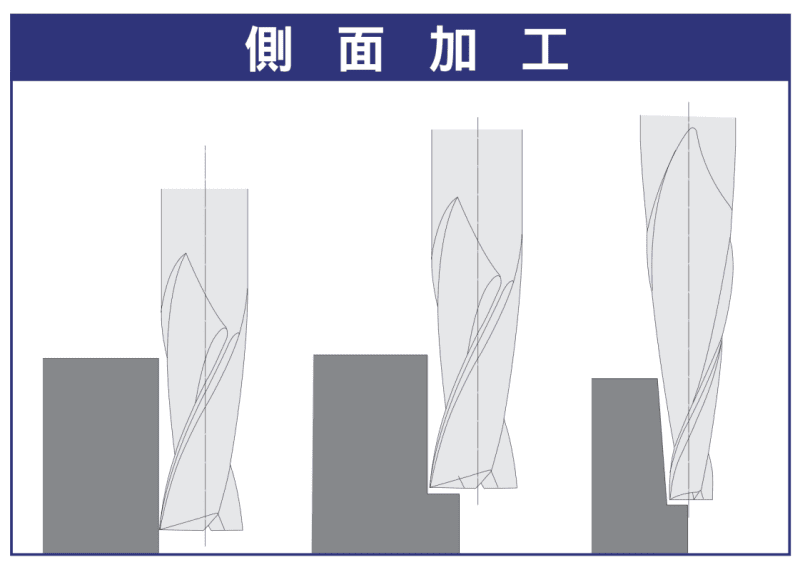
Slotting & Side Milling
What goes wrong with the wrong tool: slot with a ball nose or corner-radius tool and the floor meets the wall in a curve, so a part that needs a square fit will not go in; for a square corner and a flat floor, use a square end mill.
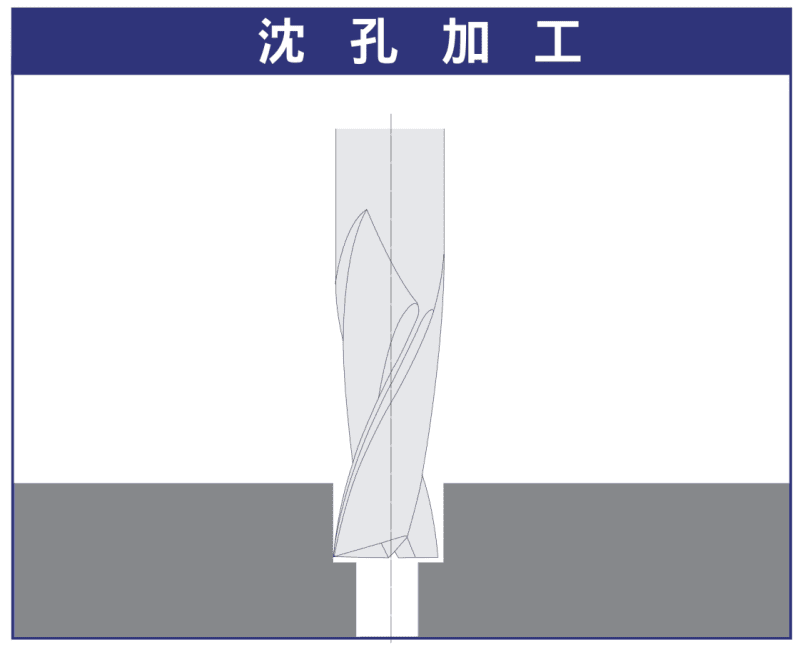
Opening a flat-bottomed counterbore at the mouth of an existing hole is also a square end mill job (see the figure below).
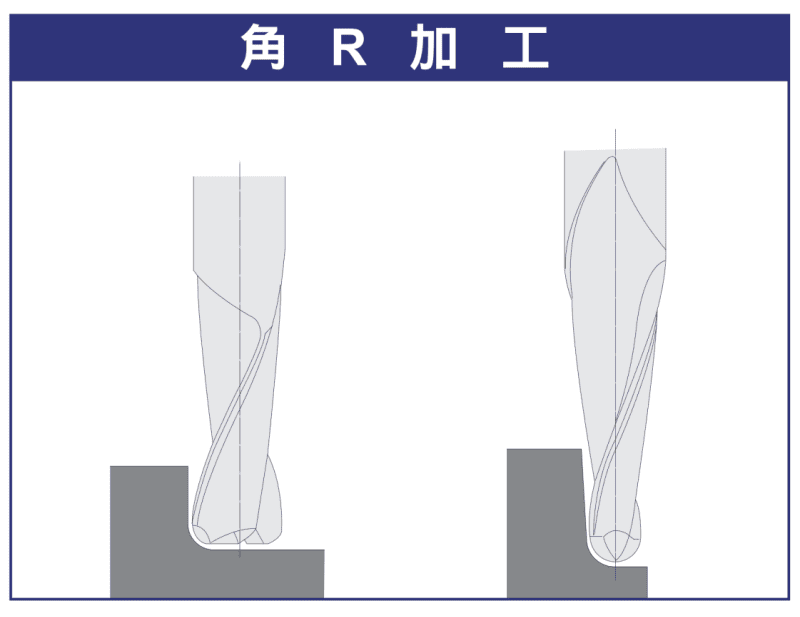
Corner R Machining
What goes wrong with the wrong tool: a square end mill leaves a sharp corner where a fillet is needed, and stress concentrates there under load; to leave a fillet use a corner-radius end mill—the fillet size follows the tool’s corner radius.
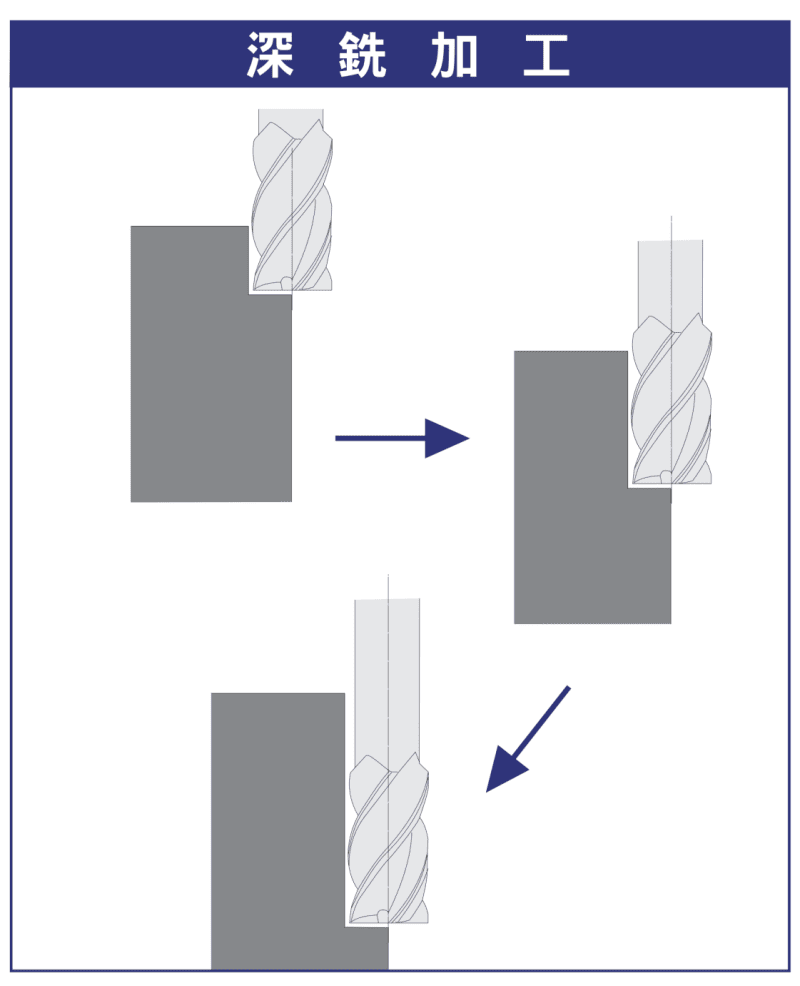
Deep Milling
What goes wrong with the wrong tool: stick the tool out too far to reach the bottom and the larger length-to-diameter ratio invites vibration, deflection and even breakage; for how overhang relates to deflection, see End Mill Length vs Deflection.
Surface (Curved) Machining
What goes wrong with the wrong tool: run a square end mill over a 3D surface and every pass leaves a step, so only a very fine stepover gets close to the surface; for setting ball-nose stepover and scallop height, see Ball-Nose Finishing: Scallop Height, Stepover, and Which Ball Size.
Draft-Angle Slope Machining
What goes wrong with the wrong tool: a straight tool can only approximate a draft slope with layer after layer of small steps; a tapered end mill forms the slope directly with the taper of its flank.
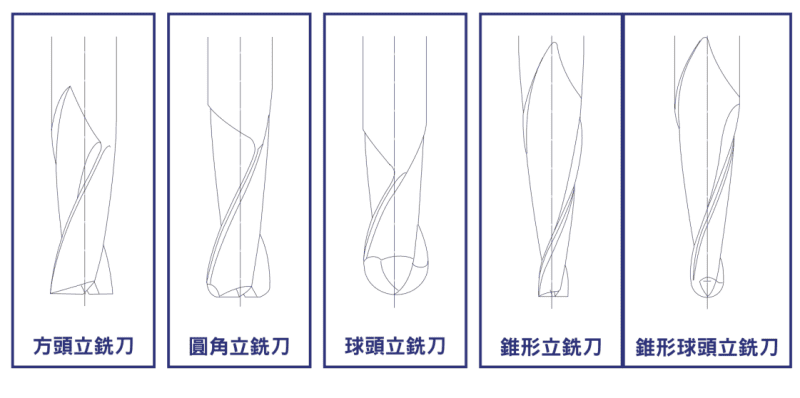
Tool Type & Application Summary
| Tool type | Main applications |
|---|---|
| Square end mill | Slotting, side milling |
| Corner-radius end mill | Corner R machining, added strength |
| Ball nose end mill | Surface machining, mold machining |
| Tapered end mill | Slope machining, draft angles |
| Tapered ball nose end mill | Compound surface machining |
How to Choose the Right End Mill Shape
| Selection basis | Condition | Recommended tool / design |
|---|---|---|
| By operation | Flat | Square end mill |
| Surface | Ball nose end mill | |
| Corner R | Corner-radius end mill | |
| Deep hole | High-rigidity tool | |
| By material | Aluminum | High helix angle tool |
| Steel | Standard or low helix angle | |
| By accuracy | Roughing | Roughing end mill |
| Finishing | Square or corner-radius end mill for flat faces and walls; ball nose for curved surfaces |
For each type's construction and characteristics (square, tapered, roughing, ball nose, corner-radius, heavy-cutting), see End Mill Types and Features.
FAQ
Which end mill should I use for slotting and side milling?
A square (flat) end mill—high cutting efficiency and ideal for right-angle and flat machining—is the first choice for general slotting and side milling.
Which tool is best for 3D surface / mold machining?
A ball nose end mill—it enables contour and profile milling with good surface quality, suited to 3D surfaces and molds.
What should I watch for in deep milling?
Use a square end mill (roughing end mill as an extension), ensure good chip-evacuation space, control the length-to-diameter ratio, and avoid vibration and tool breakage.
How do I choose an end mill shape by need?
Flat → square; surface → ball nose; corner R → corner-radius; deep hole → high-rigidity tool. Aluminum → high helix; steel → standard/low helix. Roughing → roughing end mill; finishing → square or corner-radius for flat faces and walls, ball nose for curved surfaces. For each type's characteristics, see End Mill Types and Features.
This article is part of End Mills: The Complete Guide - Know the Cutter, Choose It, Set the Conditions; Toolpaths Are Another Line; that guide shows how the whole topic fits together.
Published: 2026-03-18 | Last updated: 2026-10-19









