
Flat Drill Machining Guide: Flat-Bottom Holes, Inclined Surfaces & Efficiency
A flat drill produces a flat-bottom hole in one pass, which a twist drill cannot. What this guide helps you decide is when that switch is worth making. Starting a hole on an inclined face, thin plate, and counterbores held to a tolerance are the three places it most often earns its keep; against drilling and then milling flat, what it saves is cycle time and one tool change. Suitable hole types, the chip-evacuation and vibration points to watch, and recommended cutting conditions all follow. For how it differs from twist drills and end mills, see Flat Drill vs Twist Drill vs End Mill.
How a Flat Drill Works
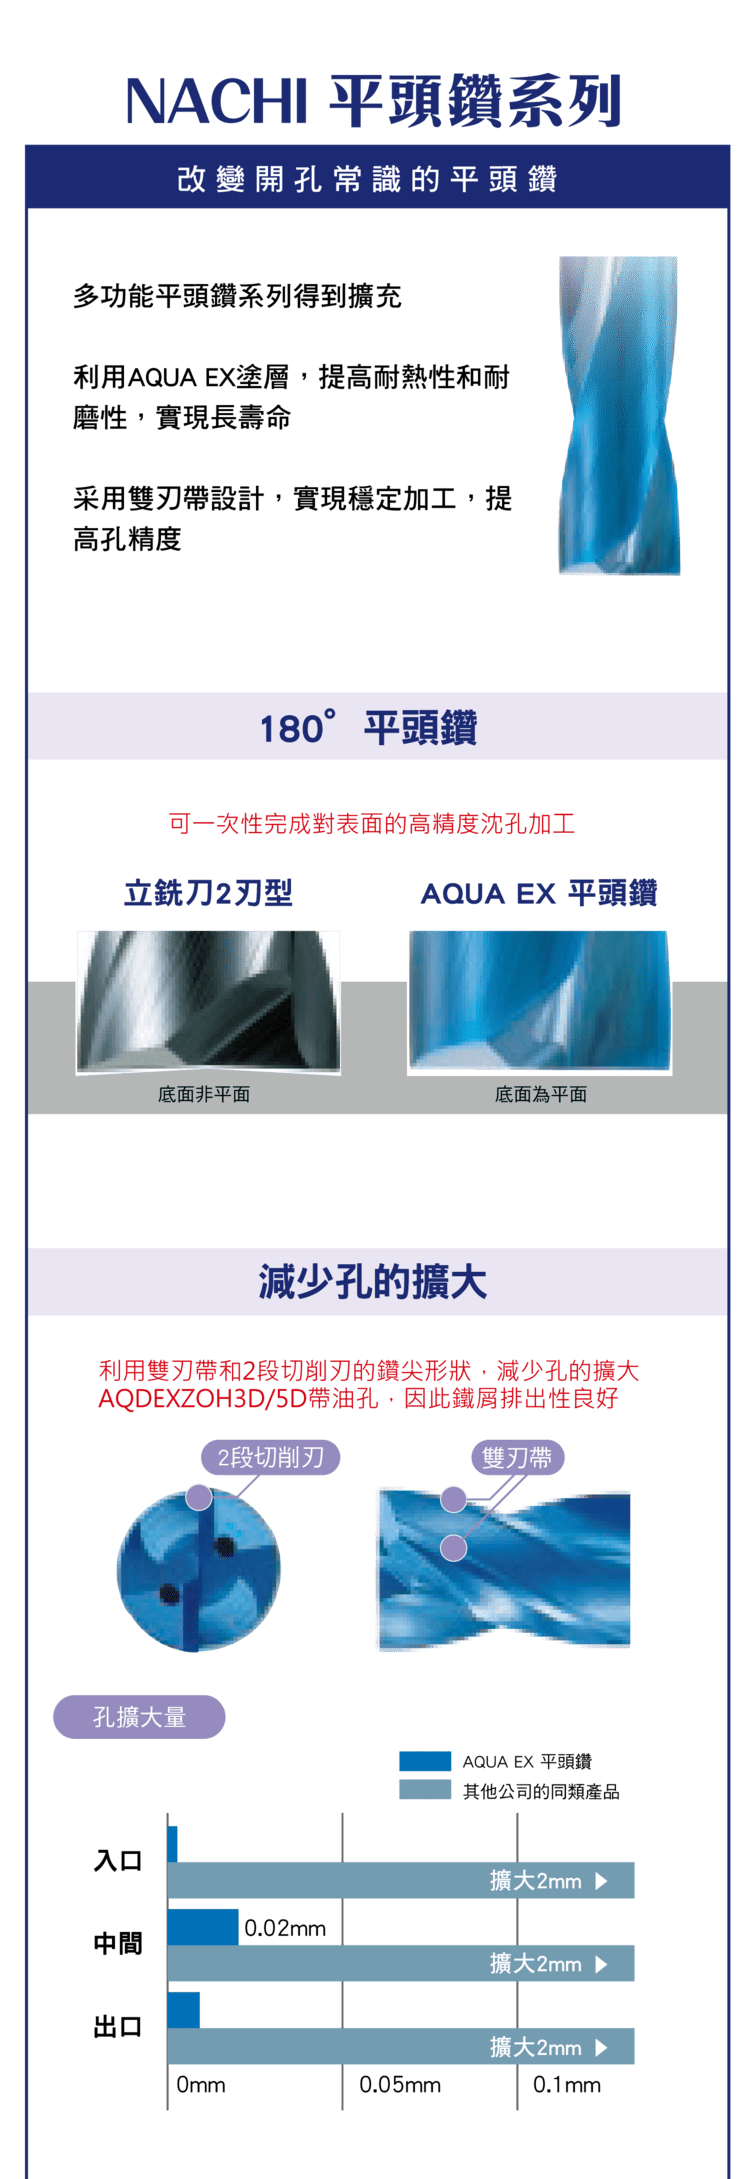
Its point is nearly flat (~180° bottom), drilling flat-bottom holes and finishing the bottom in one pass.
| Item | Flat drill | Ordinary end mill |
|---|---|---|
| Hole bottom | Flat (~180°) | May be uneven |
| Process | Hole + bottom in one pass | Often needs staging |
| Surfaces | Complex faces, inclined surfaces | Mainly lateral cutting |
Performance Advantages
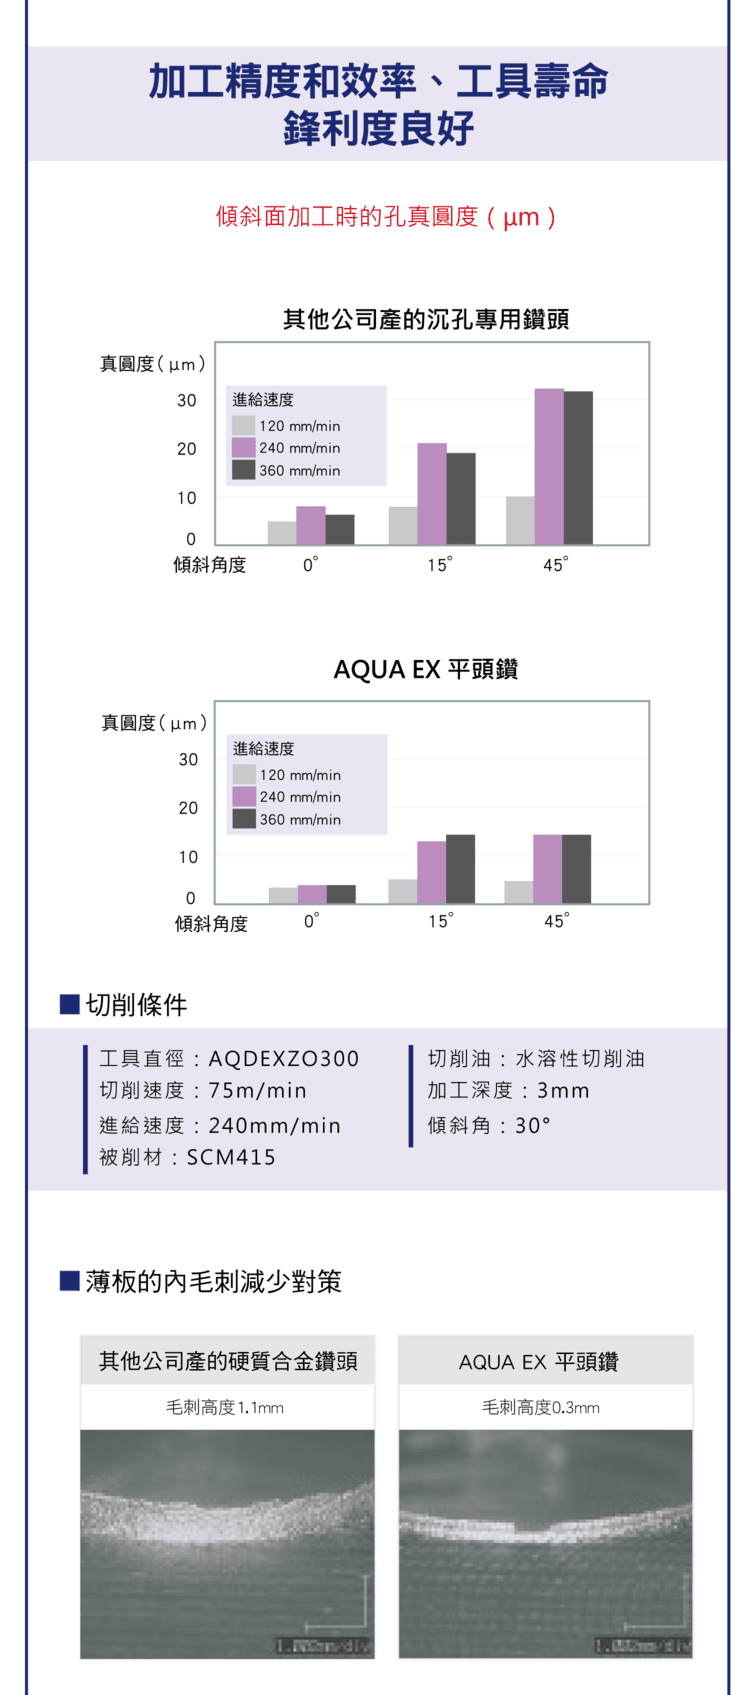
Versus conventional methods, flat drills clearly improve efficiency, life, hole accuracy and chip evacuation.
| Aspect | Conventional | Flat drill (AQUA EX example) |
|---|---|---|
| Efficiency | ~32 s (staged) | ~19 s, about 40% faster |
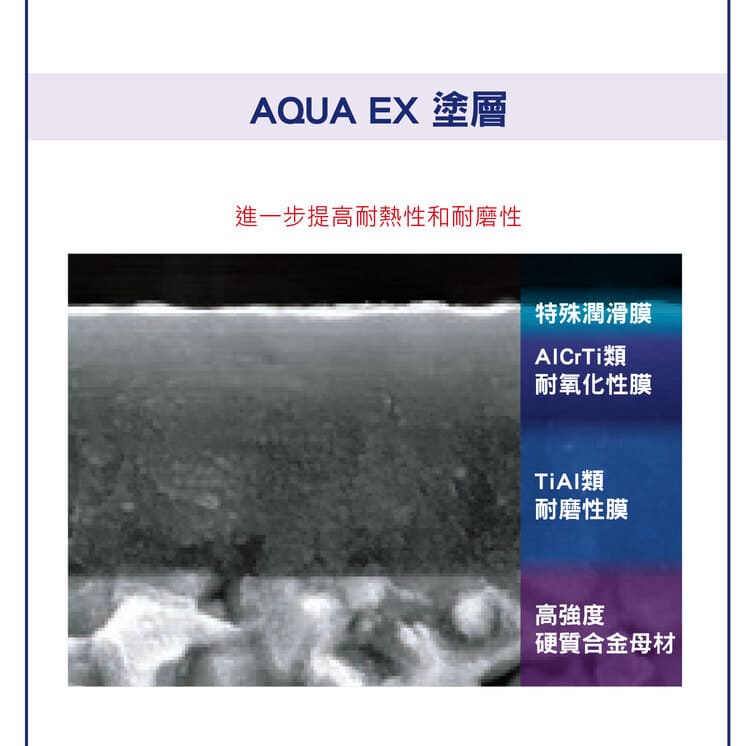
| Tool life | Point wears easily | Twin margin + heat/wear-resistant coating reduces point wear |
| Hole accuracy | Noticeable hole enlargement | Twin-margin guiding, 2-stage edge, minimal oversize |
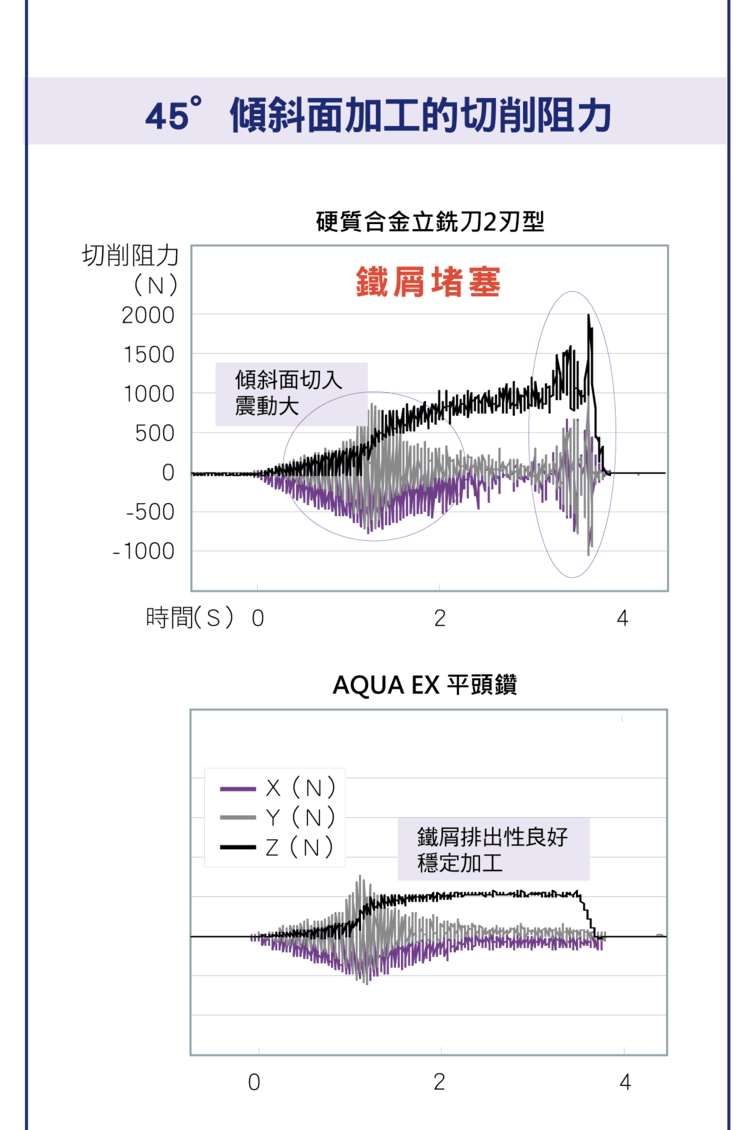
| Chip evacuation & stability | Vibration and chip clogging on inclines | Smooth evacuation, stable force, low vibration |
Multi-Purpose Applications
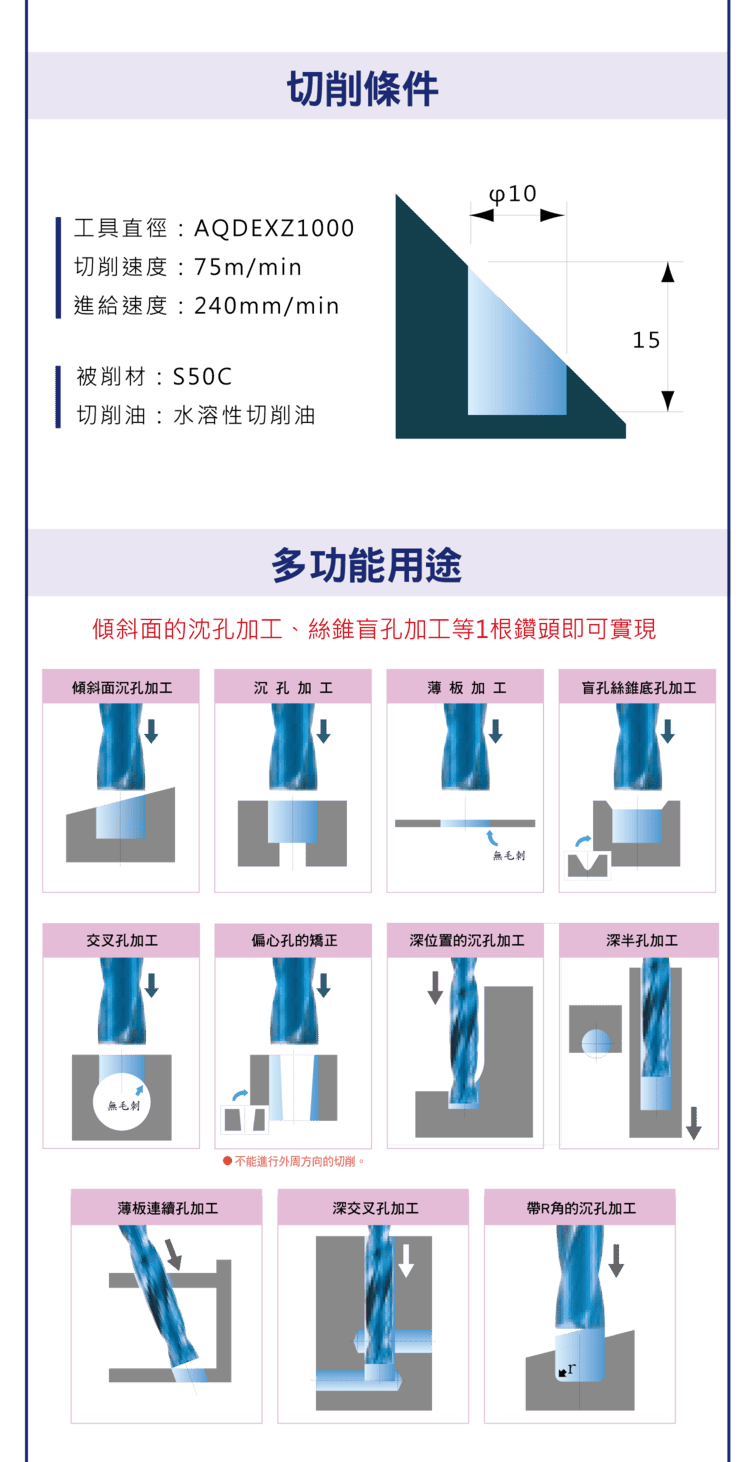
One flat drill covers many operations, raising flexibility.
| Application | Note |
|---|---|
| Inclined-surface drilling | Stable engagement, no slipping |
| Counterbore / deep counterbore | Flat-bottom counterbore in one pass |
| Thin-plate machining | Burr height markedly reduced |
| Blind flat-bottom holes | Flat hole bottom |
| Eccentric-hole correction | Stable engagement, less deflection |
Recommended Cutting Conditions
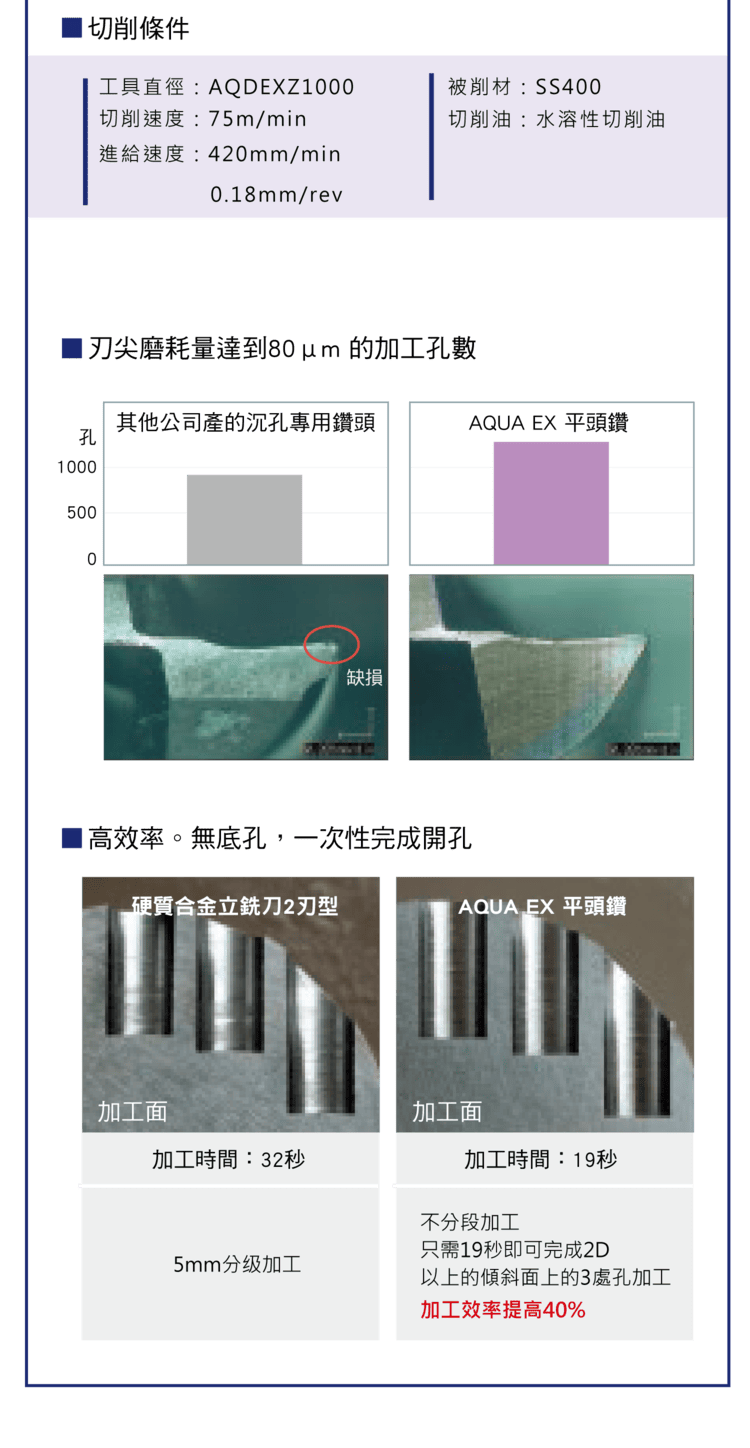
Example maker conditions (carbon/alloy steel); set actual parameters by machine, diameter and material hardness.
| Item | Example |
|---|---|
| Cutting speed vc | ~75 m/min |
| Feed rate vf | ~240–420 mm/min |
| Feed per rev fn | ~0.18 mm/rev |
| Materials | SS400, S50C, SCM415 |
| Coolant | Water-soluble cutting fluid |
For parameter calculation and conversion, see Drilling Parameters Guide.
Quality & Selection Advice
Flat drills give good roundness, low surface roughness and controlled burrs; on thin plates burr height drops markedly. Prefer them in the cases below, paired with a rigid machine.
| When to use | Recommended setup |
|---|---|
| Flat-bottom holes needed | CNC machining center |
| Inclined-surface machining | High-rigidity machine |
| High-efficiency drilling | Stable clamping and ample cooling |
For more application cases, see Flat Drill Applications.
※ The efficiency (~40%), cycle times and cutting conditions are example maker data; actual results depend on machine, clamping, material and cooling.
FAQ
Both flat drills and end mills make flat bottoms — what's the difference?
A flat drill has a ~180° flat point, making the hole and flat bottom in one pass with a flat bottom and good evacuation; an end mill is unstable in axial drilling with a possibly uneven bottom, better suited to side milling.
What is a flat drill good for?
Inclined-surface drilling, counterbores and deep counterbores, thin plates, blind flat-bottom holes and eccentric-hole correction — one tool, many uses, raising flexibility.
Why is hole accuracy better with a flat drill?
Twin-margin guiding and a 2-stage cutting edge give more stable engagement, reducing hole enlargement so oversize is minimal and dimensions are more stable.
Thin-plate drilling makes burrs — does a flat drill help?
Yes. Stable engagement and even cutting force markedly reduce burr height on thin plates, with better roundness and surface quality.
For the full reading guide on this topic, see Hole Accuracy: A Complete Reading Guide.
This article is part of Drill Bits: The Complete Guide - Start From Depth-to-Diameter, Then Pick the Drill and Set the Conditions; that guide shows how the whole topic fits together.
Published: 2026-03-24 | Last updated: 2026-08-08









