
Through-Coolant Drill Guide: Type 1/2/3 & Shank Selection
Should you move to a through-coolant drill, and which one? This guide helps you decide: look at how deep the hole is, how fast you are running and how well the material cuts, then settle which internal-channel structure to use and whether the shank should be taper or straight. The differences between the three cooling arrangements and where each belongs are both laid out.
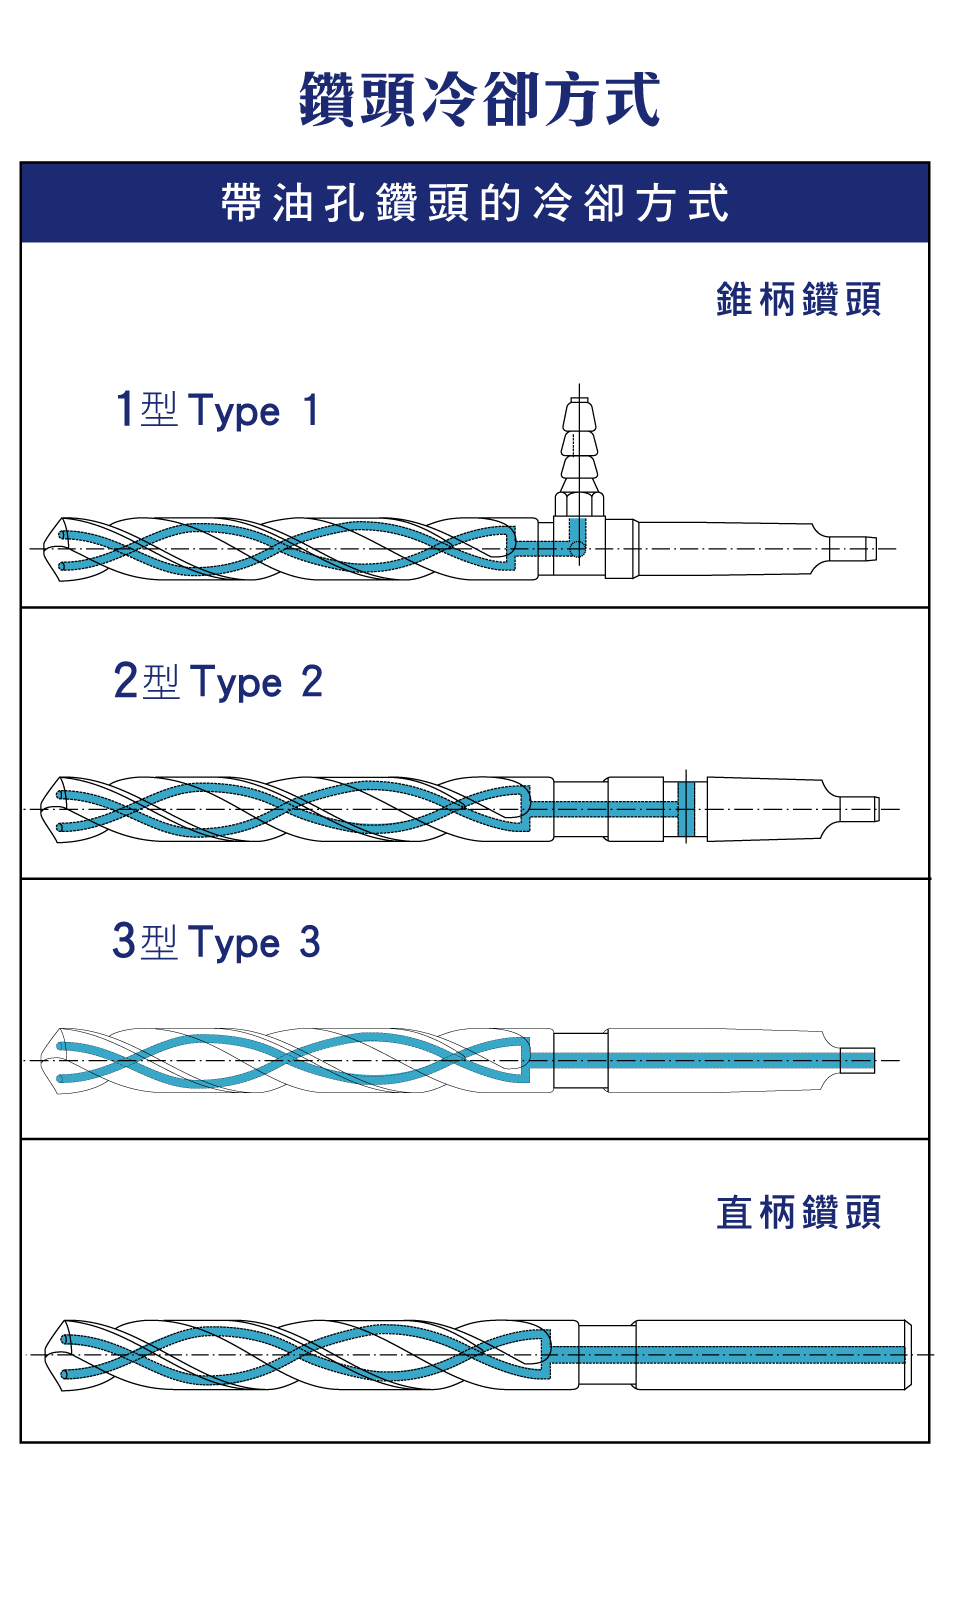
1. Principle and Function
A through-coolant drill has internal oil channels that bring coolant to the tip, raising heat removal and reducing distortion — cooling the tool, improving evacuation, lowering wear, and stabilizing quality and tool life. It is common in deep-hole and high-speed work.
2. Three Cooling Types (Type 1 / 2 / 3)
| Type | Traits | Best for |
|---|---|---|
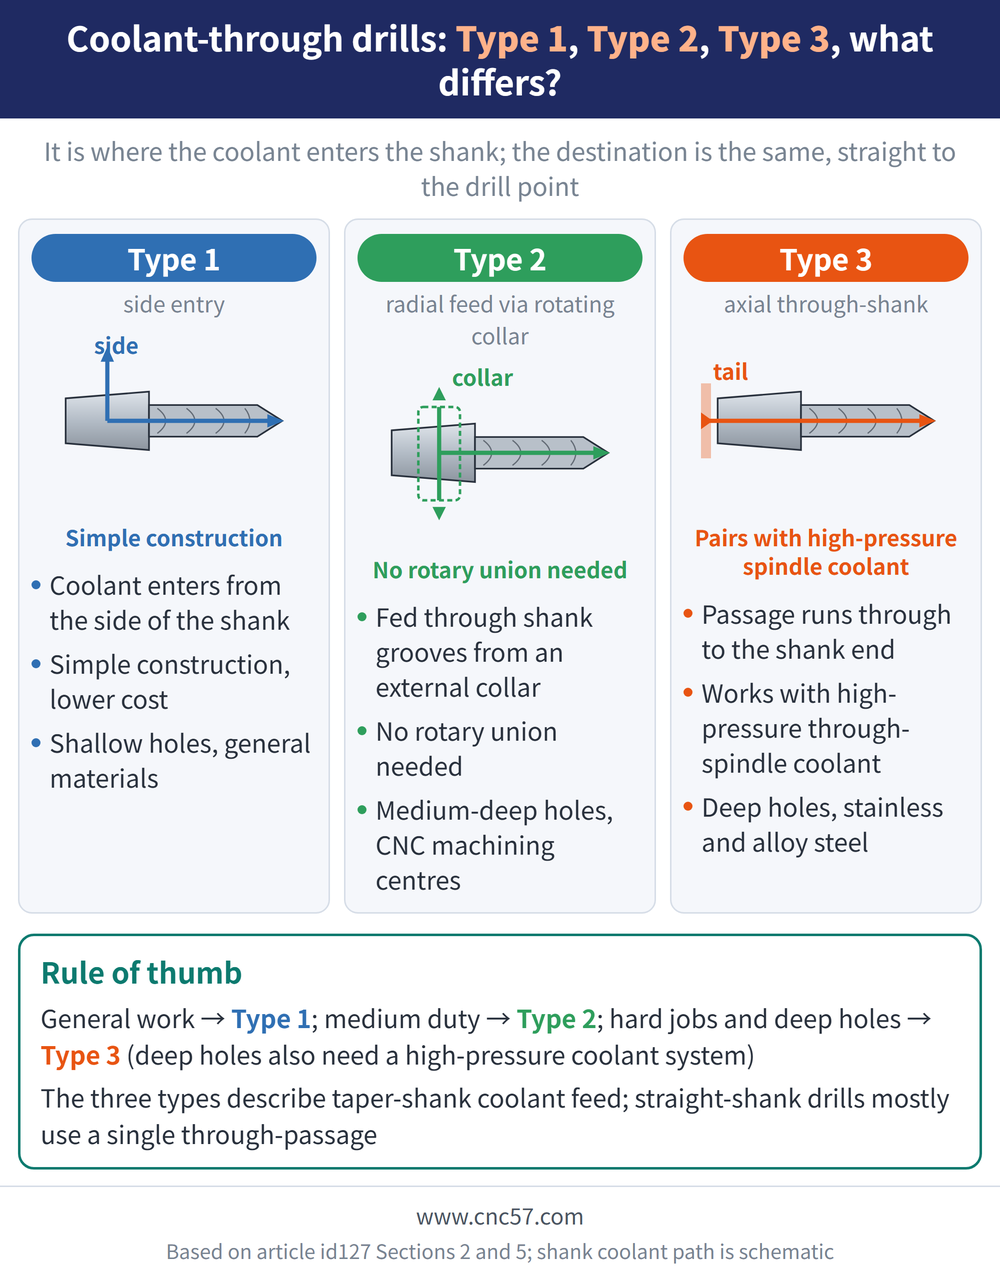
| Type 1 | Side-fed coolant, simple, lower cost | Shallow holes, general materials |
| Type 2 | Rear-fed, steadier flow, better cooling/evacuation | Medium-deep holes, CNC machining centers |
| Type 3 | High-pressure internal, coolant to the cutting zone, best evacuation | Deep holes, stainless/alloy steel |
3. Shank Form: Taper vs Straight
| Shank | Traits | Application |
|---|---|---|
| Taper shank | Good fixation, for larger machines | Heavy cutting, industrial machinery |
| Straight shank | Universal, many holding methods | CNC machining, general drilling |
For taper-shank specs, see the Drill Shank Morse Taper Guide; for straight-shank specs and runout, see the Straight Shank Drill Specification and Runout.
4. Cooling and Machining Effect
| Aspect | Effect |
|---|---|
| Cooling | Lower temperature, less tool wear |
| Evacuation | Smoother chip flow, no clogging |
| Quality | Higher accuracy, fewer burrs |
5. Selection
| Difficulty | Recommendation |
|---|---|
| General | Type 1 |
| Medium | Type 2 |
| High difficulty | Type 3 |
| Deep holes | High-pressure internal coolant |
Weigh material, depth and speed together to raise efficiency, extend life and cut cost. For deep-hole through-coolant long drills, see the Deep Hole Drill Guide.
FAQ
Q: How do I choose Type 1, 2 or 3 cooling?
Use Type 1 for general work (simple, low cost), Type 2 for medium-deep holes (rear-fed, steadier), and Type 3 for deep holes or difficult materials (high-pressure internal, best evacuation).
Q: Is internal coolant always better than external?
For deep holes and difficult materials, internal coolant delivers to the tip and far outperforms external flood; but for shallow, general holes, external cooling or Type 1 is enough.
Q: Taper or straight shank?
Taper shanks fixate well and suit large machines and heavy cutting; straight shanks are universal for CNC holding. Choose by spindle interface and cutting load.
Q: How high should coolant pressure be?
It depends on depth and material; deep holes and difficult materials need higher pressure (Type 3) for evacuation. Set actual pressure and flow per the tool maker and machine capacity.
This article is part of Drill Bits: The Complete Guide - Start From Depth-to-Diameter, Then Pick the Drill and Set the Conditions; that guide shows how the whole topic fits together.
Published: 2026-03-25 | Last updated: 2026-10-31









