
Turning Tool Rake & Clearance Guide: Force, Life & Quality
The rake and clearance angles of a turning tool are key geometry that drive cutting efficiency, tool life and machining quality. Rake affects cutting force, chip flow and temperature; clearance affects wear and the tool-workpiece gap. This guide covers positive/negative rake traits, the angle-life and angle-wear relationships, and pairing strategy to balance efficiency and tool life.
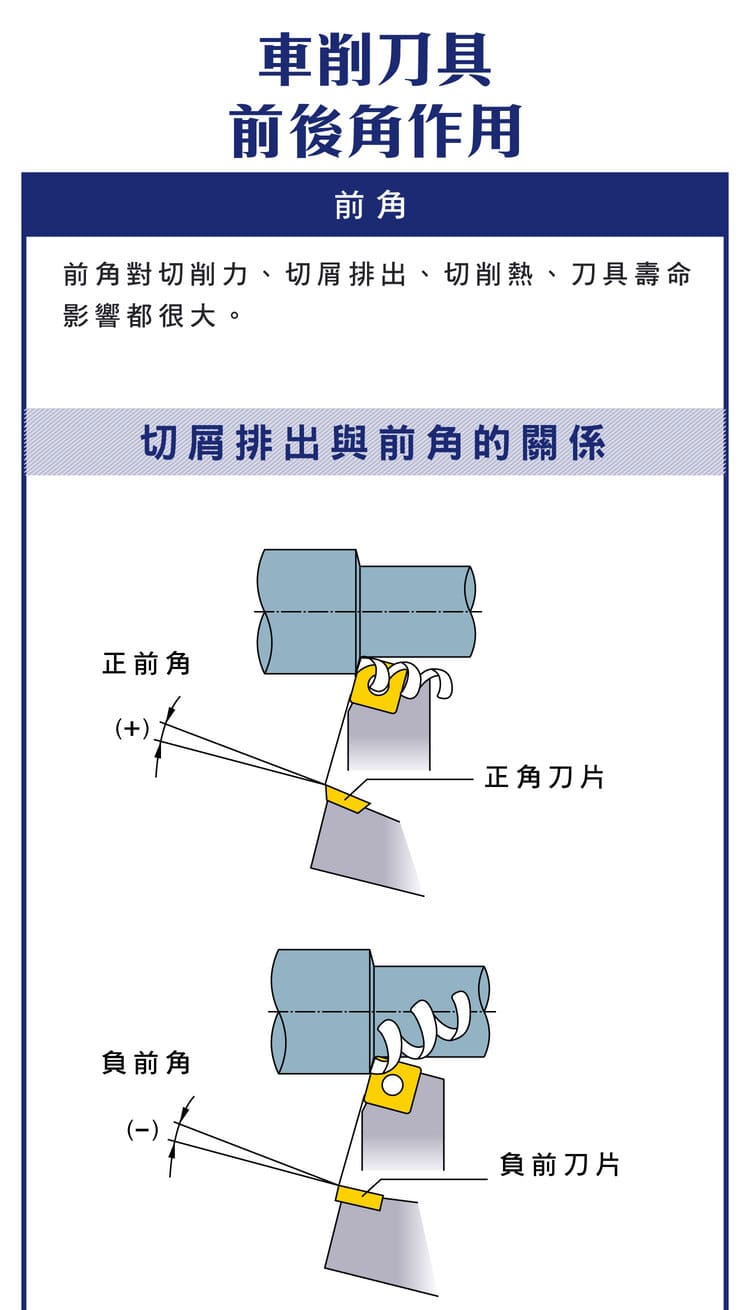
1. Rake and Clearance Basics
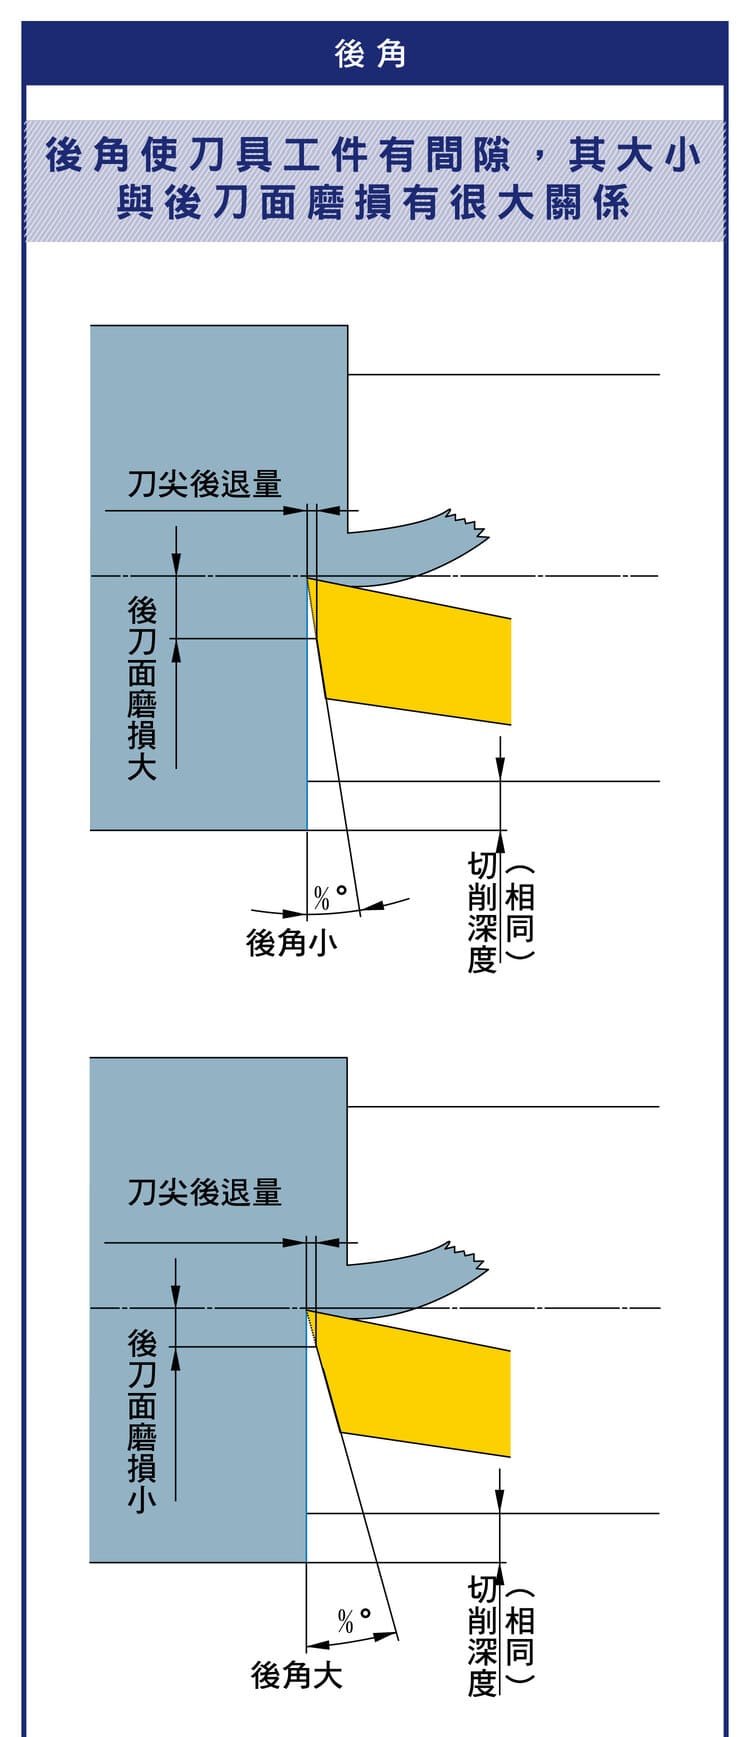
Rake angle: lowers cutting resistance, improves chip evacuation, lowers temperature and affects tool life. Clearance angle: gives a gap between tool and workpiece, reduces flank wear, and avoids friction and heat.
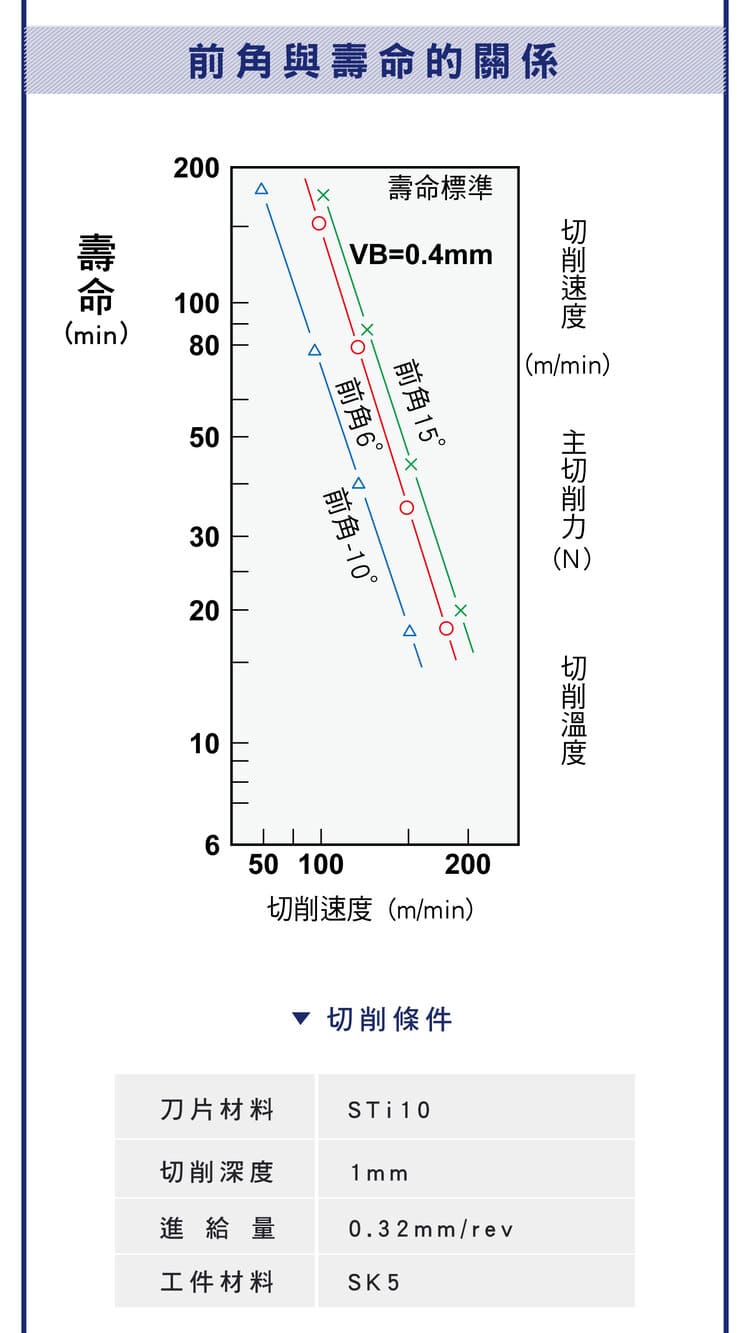
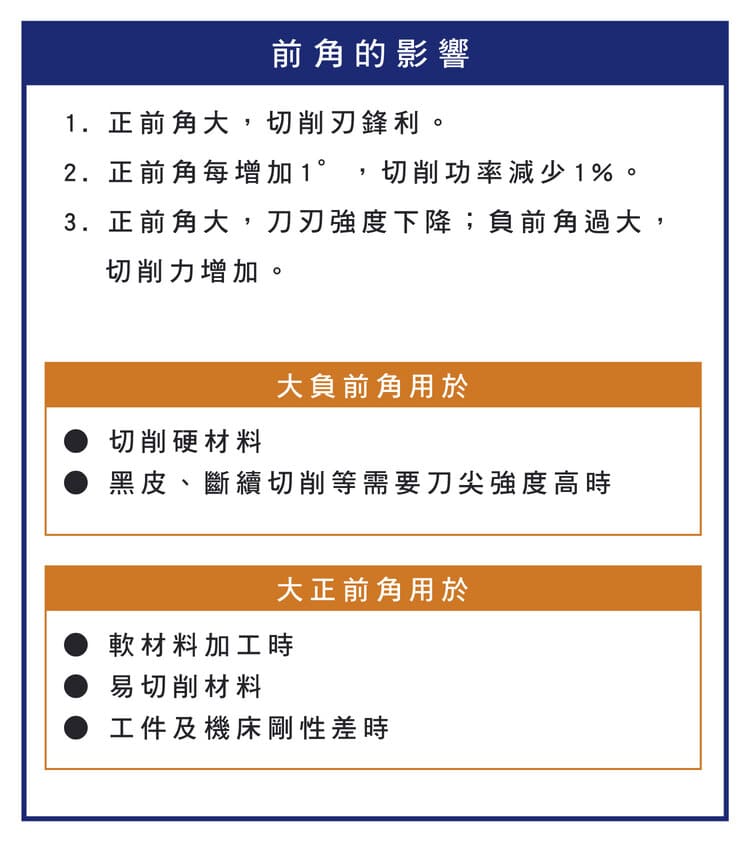
2. Rake Effect: Positive vs Negative
| Rake | Trait | Drawback / use |
|---|---|---|
| Positive | Light cutting, low force, lower temperature | Weaker edge, prone to chipping; soft/easy materials |
| Negative | Strong edge, high impact resistance | Higher force and heat; hard materials / interrupted cuts |
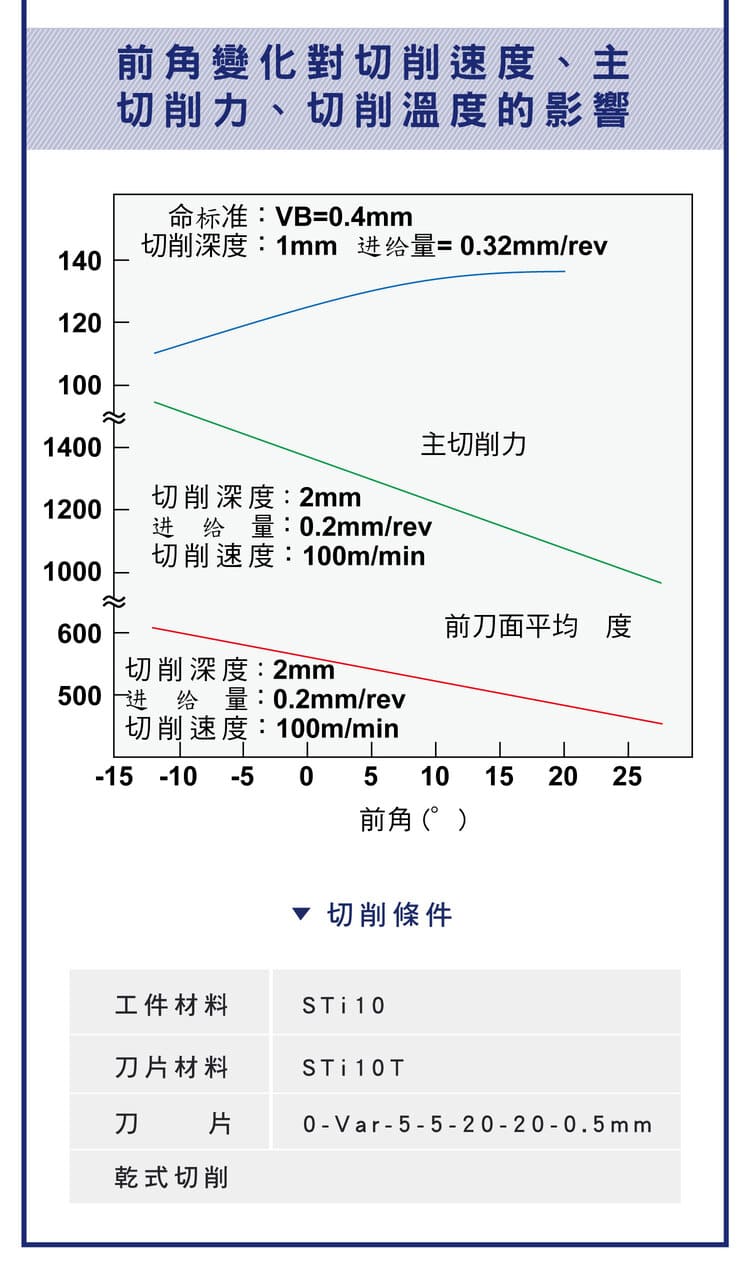
3. Rake vs Life and Parameters
Trend: more rake → lower cutting force and longer life (within a proper range), but excessive rake → insufficient strength → breakage; the key is to balance low force against edge strength. On parameters: more rake → lower main cutting force, lower temperature, smoother cutting.
4. Clearance Effect
Basic relation: larger clearance → less flank wear, but larger clearance → lower tool strength. Too small a clearance → more friction → accelerated wear; too large → a fragile edge.
5. Clearance vs Wear
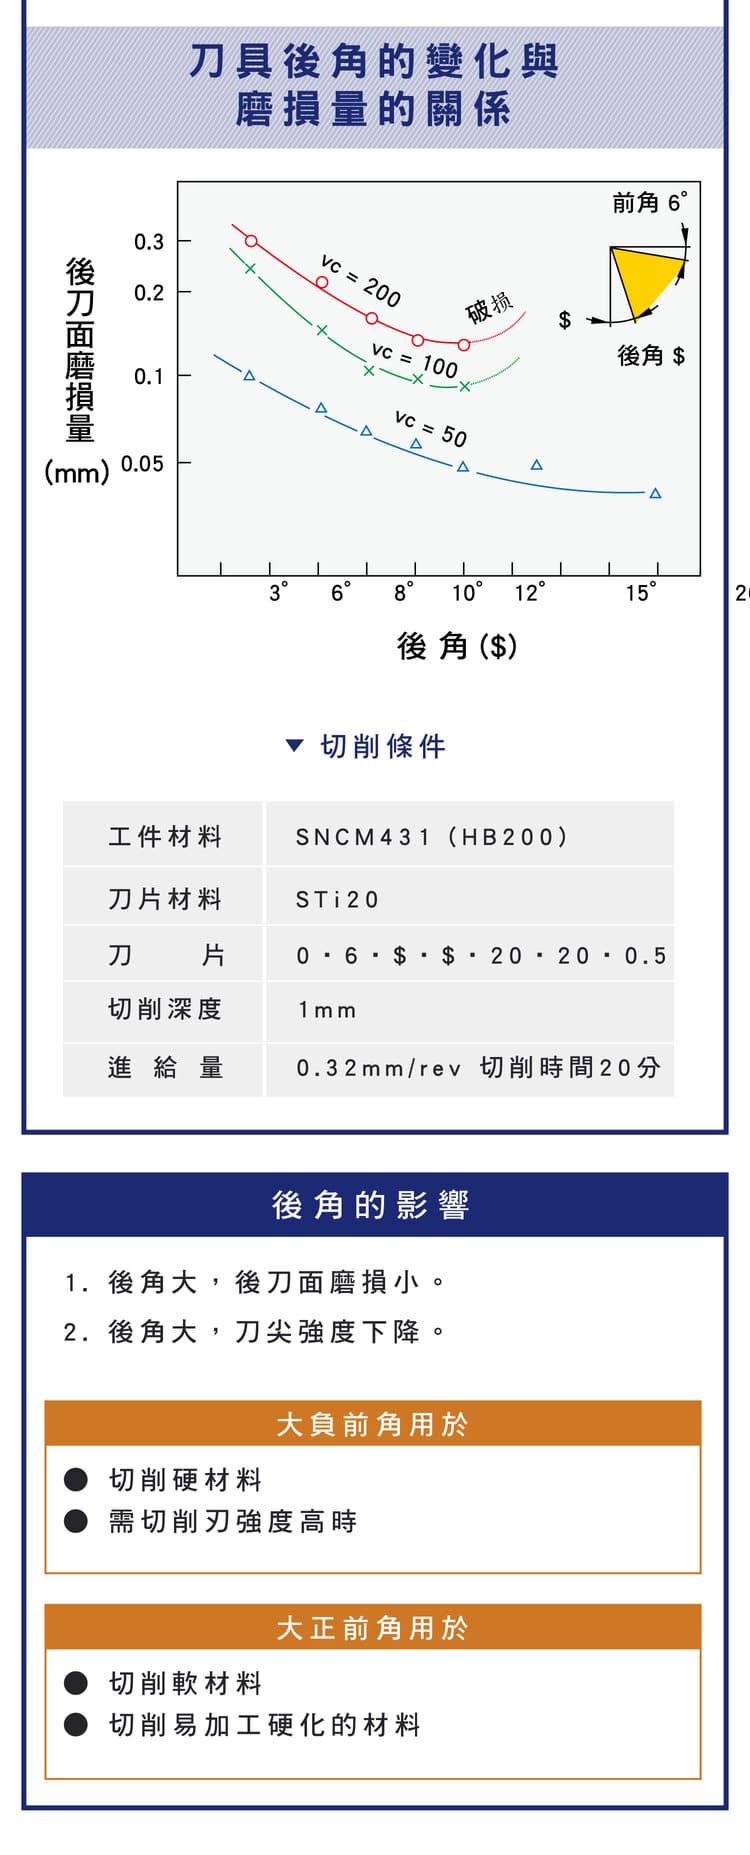
Trend: more clearance → less wear; at high cutting speed wear is more pronounced. The key is to tune clearance to cutting speed — at high speed, increase clearance moderately to curb flank wear. For wear patterns see the Turning Tool Wear Guide.
6. Pairing Strategy and Key Points
Prioritise machining stability: pair rake and clearance to material and cutting speed, and raise machine rigidity to avoid chatter. Core parameters are rake and clearance; the goals are lower cutting force, controlled wear and higher quality, ultimately longer tool life, stable quality and lower cost. For insert selection see the ISO Turning Insert Guide.
As a starting point for rake and clearance, the table below gives reference values for carbide turning tools by workpiece material, roughing and finishing. HSS tools can generally take a somewhat larger rake than listed; carbide tools for roughing usually also carry a negative land and an inclination angle.
| Workpiece material | Rake (roughing) | Rake (finishing) | Clearance (roughing) | Clearance (finishing) |
|---|---|---|---|---|
| Low-carbon steel | 20°~25° | 25°~30° | 8°~10° | 10°~12° |
| Medium-carbon steel | 10°~15° | 15°~20° | 5°~7° | 6°~8° |
| Alloy steel | 10°~15° | 15°~20° | 5°~7° | 6°~8° |
| Hardened steel | −15°~−5° | −15°~−5° | 8°~10° | 8°~10° |
| Austenitic stainless steel | 15°~20° | 20°~25° | 6°~8° | 8°~10° |
| Grey cast iron | 10°~15° | 5°~10° | 4°~6° | 6°~8° |
| Aluminium and aluminium alloys | 30°~35° | 35°~40° | 8°~10° | 10°~12° |
FAQ
Q: Positive or negative rake?
Use positive rake for soft/easy materials or when light cutting and low power are needed; use negative rake for hard materials, interrupted cuts or when edge strength and impact resistance matter. Negative inserts are often double-sided and economical but cut with more force and heat.
Q: Is more rake always better?
Within a proper range, more rake lowers force and extends life; but excessive rake thins the edge and weakens it, causing chipping and breakage. Balance low force against edge strength, choosing by material hardness.
Q: What if clearance is too small or large?
Too small a clearance increases tool-workpiece friction, accelerates flank wear and raises heat; too large makes the edge fragile and prone to chipping. Match it to cutting speed — at high speed, increase clearance moderately to balance wear and strength.
Q: How to balance life and efficiency?
With stability as the premise, pair rake and clearance to material and speed and raise machine rigidity to avoid chatter. A suitable positive rake lowers force while a material-matched clearance controls wear, balancing tool life, quality and cost.
For the full reading guide on this topic, see Tool Life and Wear: A Complete Reading Guide.
For the full reading guide on this topic, see Turning: The Complete Guide.
Published: 2026-03-25 | Last updated: 2026-10-20









