
Tapping Troubleshooting Guide: Chipping, Breakage & Size Defects
Chipped threads, a broken tap, a hole that measures wrong — this guide helps you decide where to start: chip evacuation, feed synchronization, tapping depth, or cutting fluid. Each of the four common symptoms points to a different group of causes, so you can locate the group first and then work through it.
1. Chipping and Breakage Causes
Common problems are tap chipping and breakage, mainly from chips not clearing, chips stuck in the thread and insufficient chip space. The keys are confirming tapping depth and ensuring ample chip space.
2. Typical Evacuation Mistake
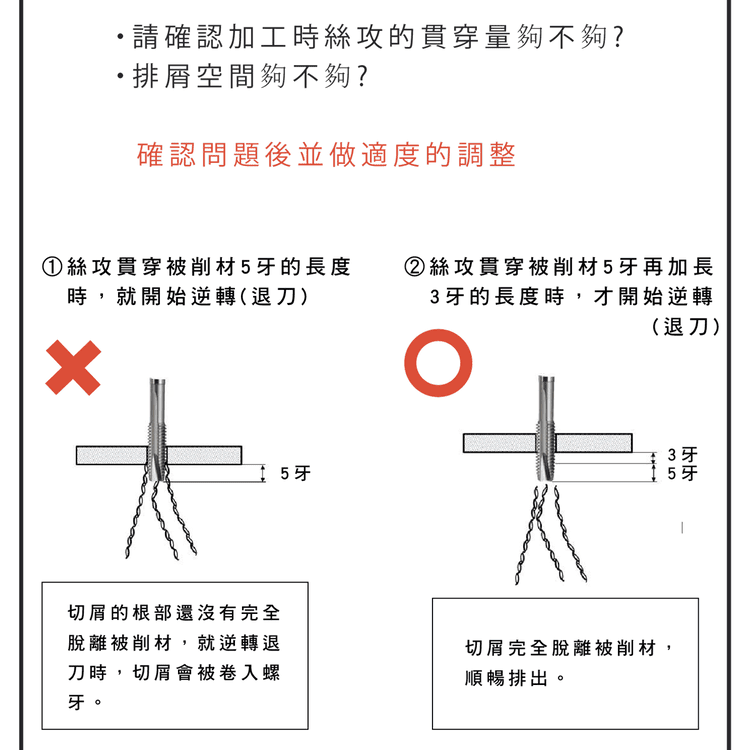
Wrong practice: reversing to retract before the cut fully clears, which wraps chips into the thread, raises load and causes chipping. The right way is to retract only after the cut fully passes and keep evacuation smooth.
3. Chip Space and Structure
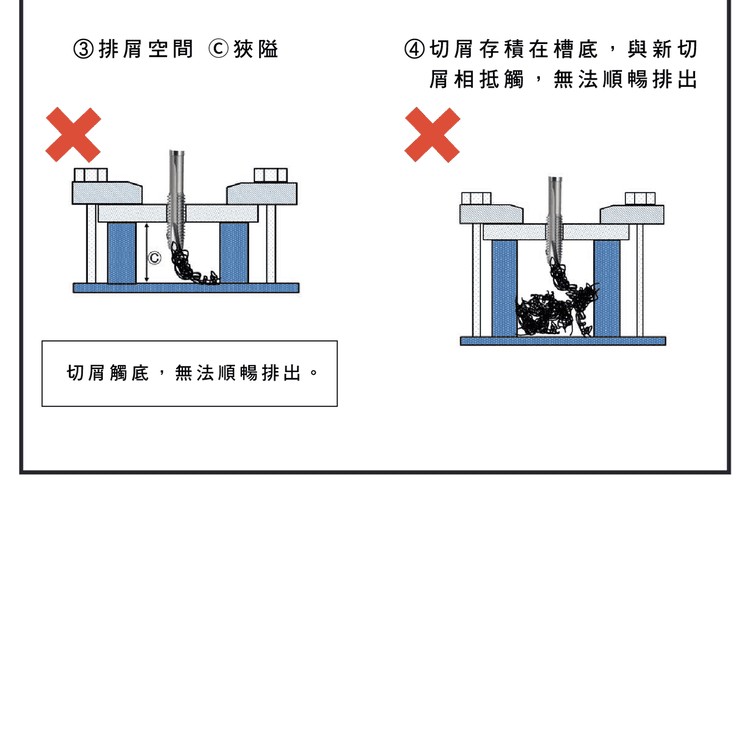
Insufficient bottom space and chips piling at the bottom stop chips from clearing and let them interfere with new cutting. Improve by adding chip space, deepening the hole and avoiding bottom interference.
4. Oversize (Too Large) Causes
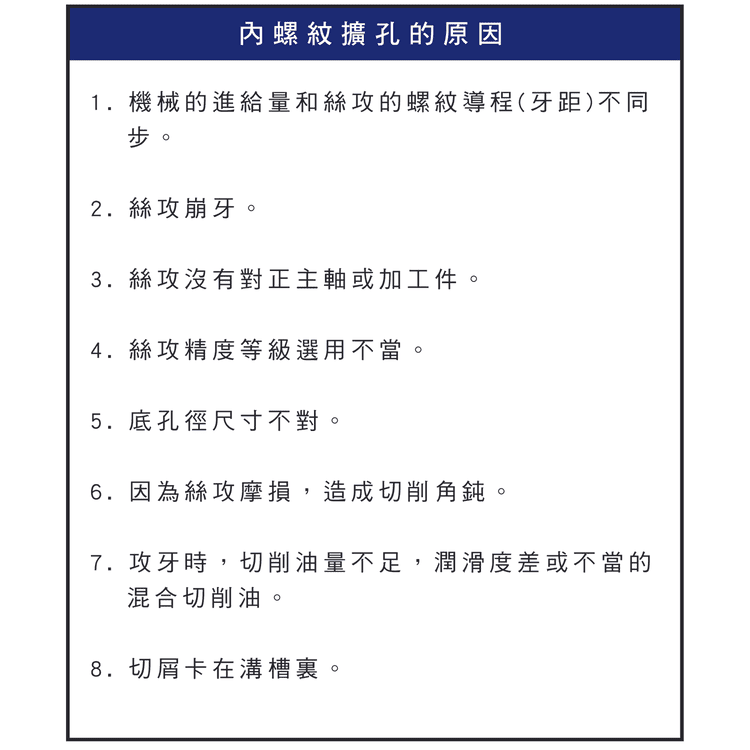
Causes of an oversize thread: machine feed not synced to pitch, tap chipping, workpiece not aligned to spindle, wrong precision grade, wrong hole size, tool wear, poor lubrication and stuck chips. The result is loose threads that miss standard accuracy.
※ Full oversize causes and fixes are in the Internal Thread Oversize Causes.
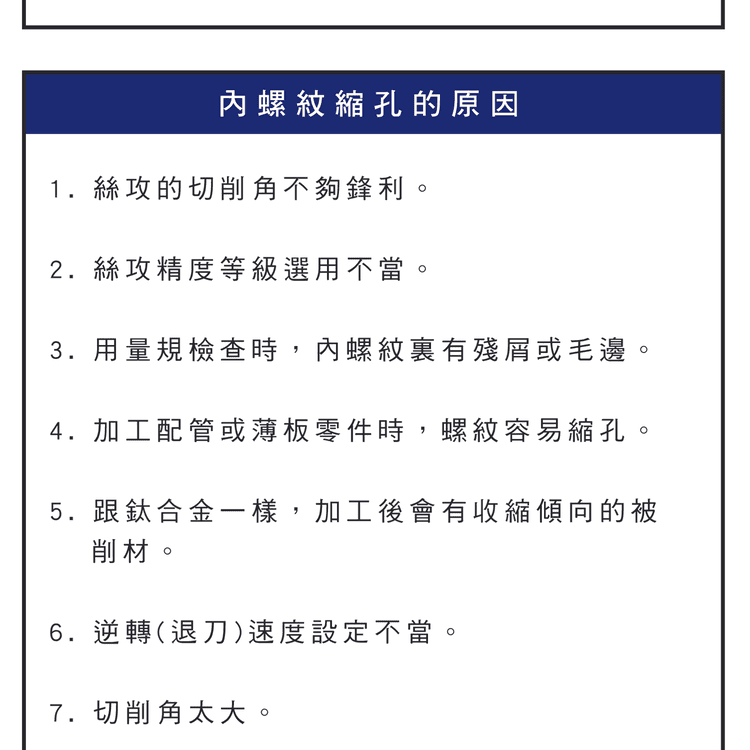
5. Undersize (Too Small) Causes
| Cause | Fix direction |
|---|---|
| Dull tool, too-large rake | Replace/regrind, choose the right geometry |
| Wrong precision grade | Internal thread: 6H etc.; tap: P class (higher number cuts larger). See the Tap Thread Tolerance Guide |
| Residual chips or burrs | Clear chips, deburr |
| Thin-plate/pipe distortion, post-machining shrinkage | Pre-allow compensation, hold steadily |
| Wrong retract speed | Control retract, synchronize feed |
Undersize makes the thread too tight and hard to assemble.
6. Lead and Accuracy
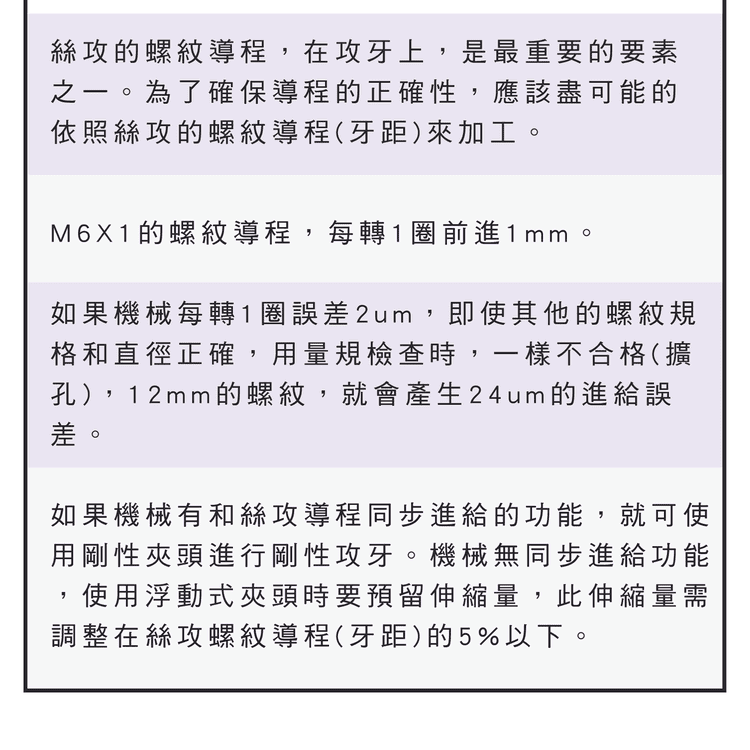
The core is that the lead (pitch) must match the machine feed. For example M6×1 → 1mm per revolution. A 2μm per-rev error accumulates over a long thread, causing oversize or form drift. Rigid tapping (feed = pitch) or a floating holder is key to avoiding lead error.
7. Countermeasures Summary
Chipping/breakage: retract after the cut fully passes, add chip space, clear chips. Size defects: rigid tapping or a floating holder to compensate lead, pick the right grade, control hole and retract. With good cutting fluid and a suitable speed, defects drop sharply.
For oversize detail see the Internal Thread Oversize Causes; for general fixes see the Thread Machining Solutions; for pilot holes see the Metric Tap Drill Chart; for holders see the Tapping Setup Guide.
FAQ
Q: Most common cause of chipping/breakage?
Usually poor evacuation: chips stuck in the thread, insufficient chip space, or reversing to retract before the cut clears and wrapping chips in. Retract after the cut fully passes, deepen the hole for chip space and clear chips to greatly improve.
Q: What causes a too-tight (undersize) thread?
Often a dull tool, residual chips/burrs, thin-plate/pipe distortion or post-machining shrinkage, wrong retract or wrong grade. Clear chips, deburr, use a sharp tool, pre-allow compensation and hold steadily.
Q: Why must lead sync with feed?
Axial feed per revolution must equal the pitch (e.g. M6×1 = 1mm/rev). If not synced, small per-rev errors accumulate over length, overcutting flanks or drifting the form. Rigid tapping or a floating holder ensures sync.
Q: Why does retract timing matter?
Reversing to retract before the cut fully clears wraps chips into the thread, raising load and chipping. Retract only after the cut fully passes and keep evacuation smooth — blind holes especially need bottom chip space.
Last updated: 2026-10-09
For the full reading guides on this topic, see Thread Machining: A Complete Reading Guide and Chip Control: A Complete Reading Guide.









