
Coolant-through tool holders deliver coolant directly to the cutting zone, which matters most for deep-hole drilling, high-speed milling, and chip evacuation. But having a coolant hole doesn't mean you have through-tool delivery. This guide explains how the collet fitted to a coolant-through holder decides where the coolant comes out, why jet through is a separate holder design, and the most common selection mistake.
1. Why Use a Coolant-Through Tool Holder
Compared with flood coolant applied from outside, a coolant-through (internal-cooling) holder routes coolant through internal channels to a point near the cutting edge, carrying away heat and helping chip evacuation far more effectively - especially critical for deep-hole drilling, long-overhang milling, and difficult-to-machine materials. If coolant never actually reaches the cutting zone, its effectiveness drops sharply, which is exactly why "does the holder have a coolant hole" and "does coolant actually reach the tool tip" are two different questions.
Choosing the clamping end: see Collet System Comparison and Selection.
2. Where the Coolant Comes Out - It Depends on the Collet
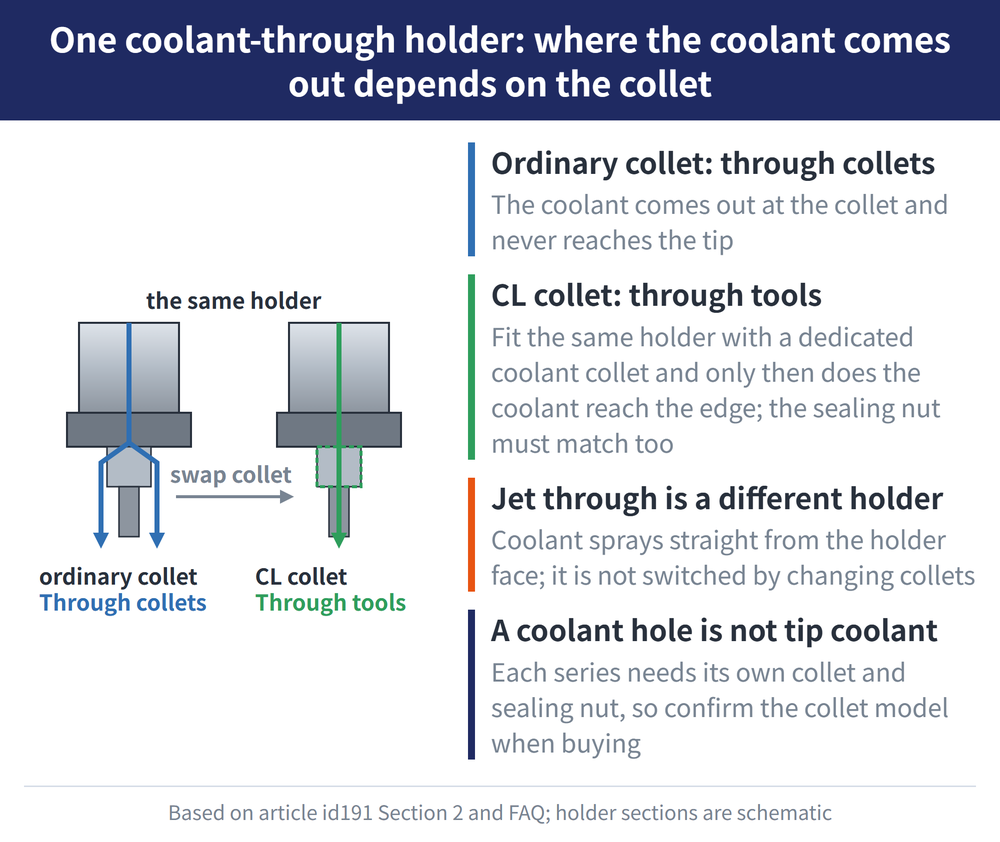
Tool holder catalogs mark where the coolant comes out with photos and English labels. Taking one coolant-through holder series in a catalog as the example, where the coolant comes out of the same holder depends on the collet fitted; jet through is a different holder design:
| Catalog label | Fitted with / where the coolant comes out |
|---|---|
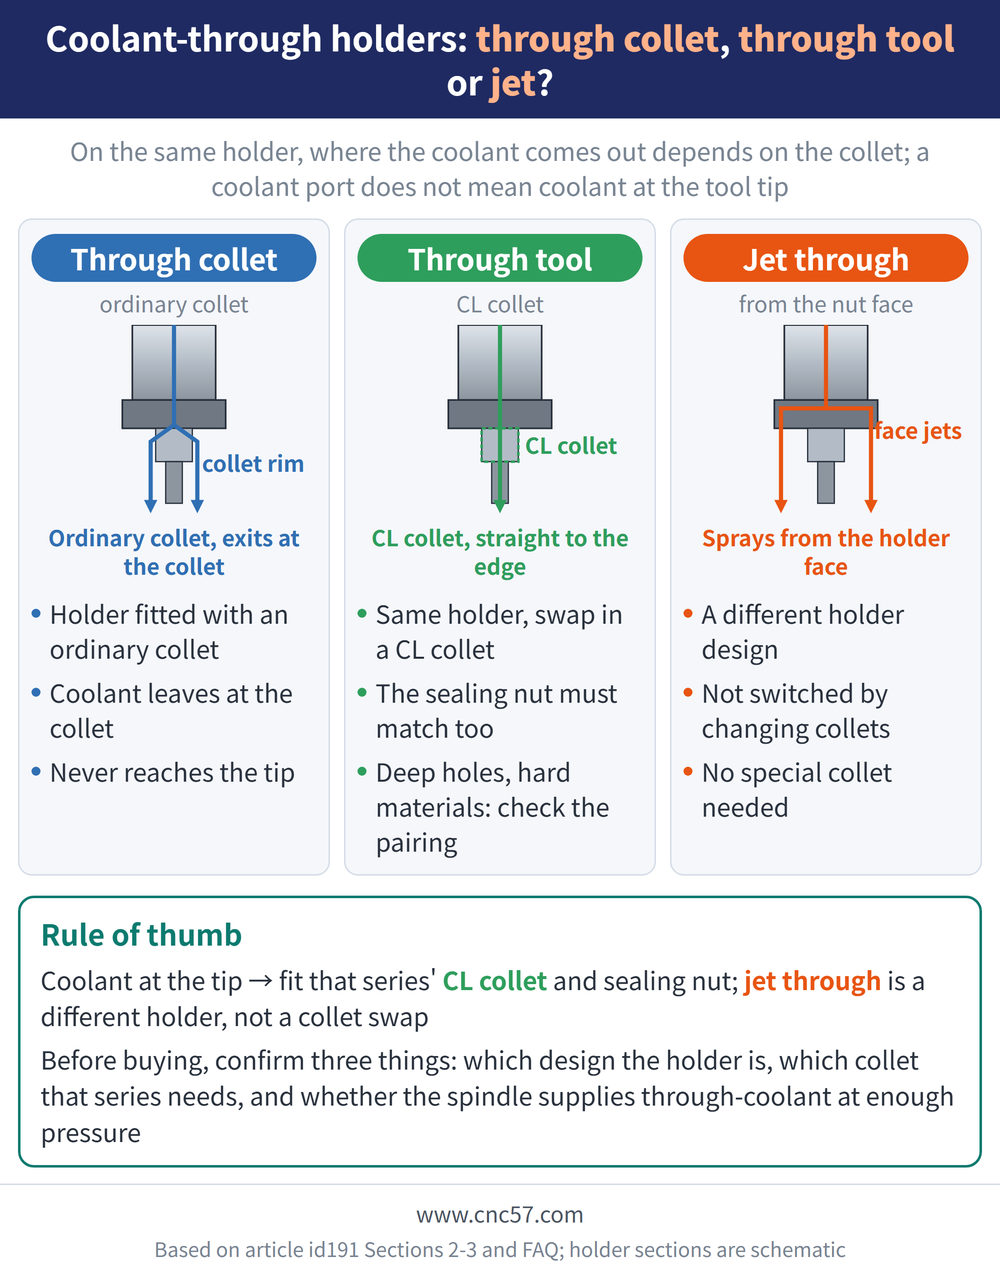
| Through collets | With an ordinary collet fitted to a coolant-through holder, the coolant comes out through the collet |
| Through tools | Fit the same holder with a dedicated coolant collet (a CL collet in the catalog) and only then does the coolant reach the cutting edge |
| Jet through | Coolant sprays straight from the holder's end face; a different holder design, not something you switch by changing collets |
For the coolant to reach the cutting edge, the collet has to be the matching coolant collet; the collet and sealing nut each series needs vary, so confirm the collet model at purchase. Assuming that "the holder body has a coolant hole" automatically means "through-tool delivery" is the most frequently misunderstood point in practice: with a standard (non-sealed) collet fitted, the coolant only comes out at the collet and never reaches the tip.
ER collet torque: see ER Collet Specification and Torque.
3. Selection and Compatibility Checklist
| Item to Confirm | Notes |
|---|---|
| The holder's coolant architecture | Confirm whether it is a coolant-through holder whose outlet is set by the collet, or a jet-through holder design |
| Whether a sealed collet is required | Through-tool delivery requires a dedicated sealed (CL-type) collet and sealing nut - neither is optional |
| Machine support for coolant-through | Confirm the spindle itself has internal coolant supply capability, including sufficient pressure |
| Process requirements | Deep-hole drilling, long-overhang milling and hard-to-machine materials need coolant at the cutting edge; confirm the collet pairing for through-tool delivery is complete |
Start by clearly identifying your process requirements (deep hole, long overhang, or difficult material), then match against the holder's delivery architecture and collet pairing requirements - this avoids buying a holder with "a coolant hole" that never delivers the expected cooling because the collet doesn't match.
Holder clamping methods compared: see Tool Holder Clamping Methods Compared.
FAQ
Q1: If a holder has a coolant hole, will a standard collet give me through-tool coolant?
Not necessarily. Through-tools delivery requires a dedicated sealed collet and sealing nut to work correctly. Fitting a standard (unsealed) collet often lets coolant leak out around the collet instead of reaching the tip - the holder has the coolant hole by design, but you don't actually get through-tool delivery in practice.
Q2: What's the difference between jet-through and through-tools, and which should I choose?
The difference is where the coolant comes out and what it has to be paired with. Jet-through sprays coolant straight from the holder's end face; it is a separate holder design and needs no special collet. Through-tool delivery is what a coolant-through holder gives once it is fitted with a dedicated coolant collet, so the coolant reaches the cutting edge. When deep holes, long overhangs or difficult materials need coolant at the edge, confirm the collet pairing for through-tool delivery first.
Q3: What does a coolant-through holder require from the machine?
The machine spindle itself must have internal coolant supply capability, including adequate pressure and flow, for a coolant-through holder to work as intended. If the machine lacks an internal coolant supply system, the holder's coolant-through feature simply can't be used regardless of its design - confirm machine specifications before selecting.
Q4: Can I switch a single holder between through-collet and through-tool delivery?
For the coolant-through holder series in the catalog, yes: changing the collet changes where the coolant comes out - an ordinary collet gives through-collet delivery, and a dedicated coolant (CL-type) collet gives through-tool delivery. Jet-through is a separate holder design and is not switched by changing collets. Pairing conditions vary by series, so confirm against that series' manufacturer catalogue rather than assuming.









