
Drill and Tap Process Guide: Best Tool Combos by Hole Type
Internal-thread machining combines drilling, guiding and tapping. Matching the right drill and tap to each hole type (blind, deep, curved, inclined, thin plate) improves accuracy and efficiency, lowers breakage and interference risk, and stabilizes production quality and tool life. This guide organizes the tool combinations, drill types and tap-selection rules as a reference for CNC tapping and drilling process design.
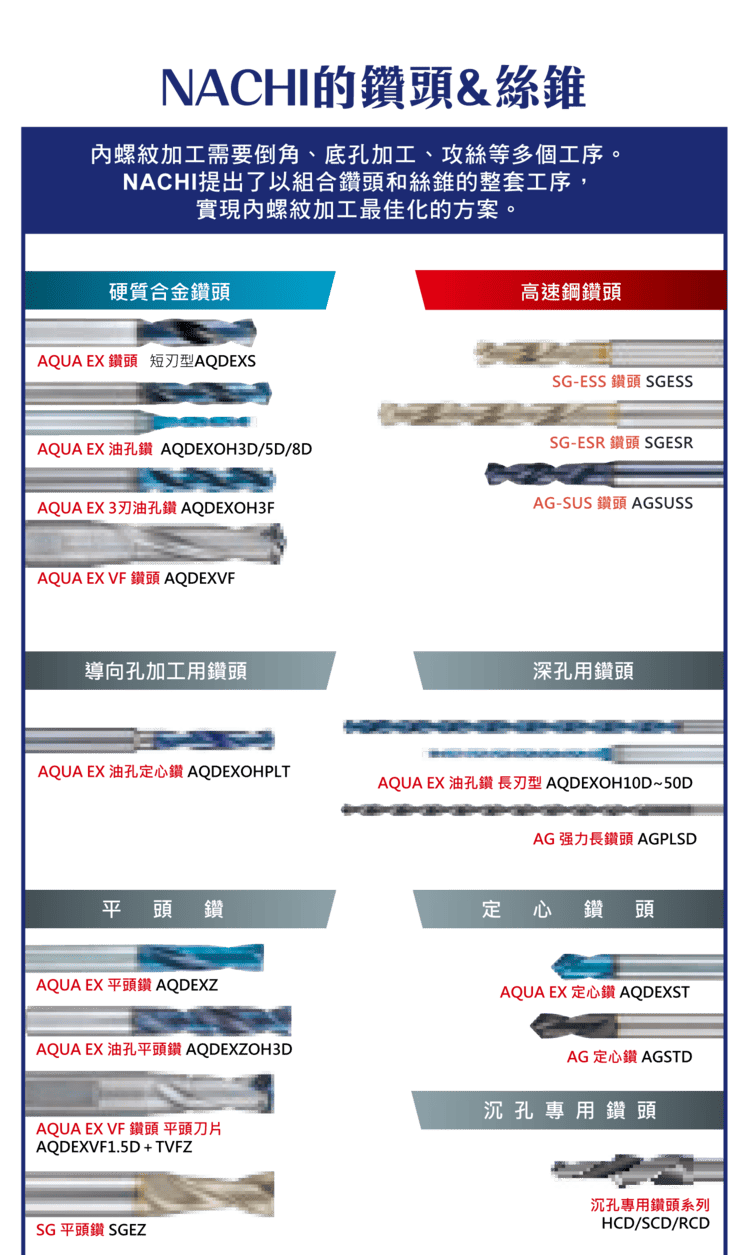
1. Internal-Thread Process Concept
Internal-thread machining usually includes pilot-hole drilling, a guide hole or chamfer, and tapping. Each step must match its tool so size and accuracy stay consistent, avoiding tap interference and bad threads.
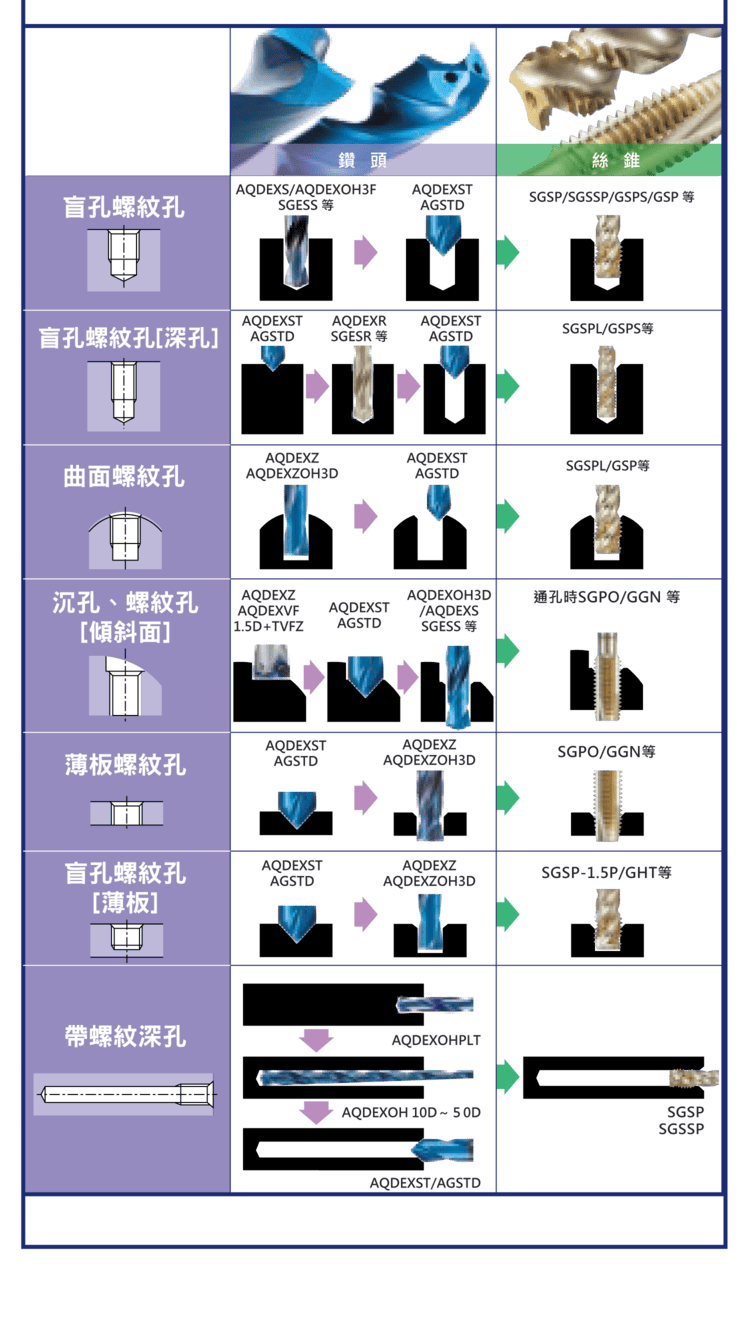
2. Tool Combinations by Hole Type (Manufacturer Example)
| Hole type | Suggested flow | Benefit |
|---|---|---|
| Blind | Drill (standard/oil-hole) → flat or center drill to true the bottom → tap | Better bottom accuracy, avoid tap interference |
| Deep | Deep-hole drill (through-coolant) → guide hole → dedicated tap | Better evacuation, lower breakage risk |
| Curved | Flat or special-edge drill to locate → finishing | Better location, less eccentricity |
| Inclined / counterbore | Flat drill to true the incline → standard drill → tap | Machine inclines directly, less vibration/drift |
| Thin plate | Thin-plate-suited drill → dedicated tap | Better thread integrity, fewer burrs |
| Threaded deep hole | Deep-hole drill (10D–50D, stable evacuation) → matching tap | Suits long holes, more stability |
※ The combinations above are a manufacturer (e.g. NACHI) example flow; follow the tool maker's recommendation and site conditions for actual use.
3. Drill Types and Applications
| Drill type | Best for |
|---|---|
| Standard (short flute) | General holes |
| Oil-hole (through-coolant) | Deep holes |
| 3-flute | High efficiency and accuracy |
| Flat drill | Flat-bottom holes, inclines, curved locating |
| Center drill | Guiding and centering |
4. Tap Selection
| Condition | Suggested tap |
|---|---|
| Through hole | Spiral-point tap |
| Blind hole | Spiral-flute tap |
| Ductile materials (low-carbon steel, stainless, aluminium) / thin plate | Forming (chipless) tap |
The tap must match the pilot-hole size and material; for pilot-drill selection, see the Flat Drill Guide and Deep Hole Drill Guide.
5. Deep-Hole Tapping: Why Deeper Means More Breakage
The deeper the hole, the longer the path the chips must travel; once they jam in the flutes, torque jumps and the tap breaks. So deep-hole tapping is all about chip evacuation and coolant supply:
| Item | Approach |
|---|---|
| Pilot hole | Centre first, then drill to depth with a through-coolant deep-hole drill; keep the hole straight, as a slant side-loads and snaps the tap |
| Blind-hole depth | Drill deeper than the thread depth so chips have room and the tap does not bottom out |
| Tap | Spiral-flute for blind holes; if the reach is short use an extended-shank tap or an oil-hole type |
| Coolant | From about 2-3×D deep prefer through-coolant (oil-hole taps) to flush chips; with external coolant aim at least one nozzle along the tool axis |
| Conditions | Run slower than for a normal hole, then fine-tune by torque |
The coolant threshold follows Sandvik tapping technical data. For choosing models see the Spiral Point Tap Series; for RPM conversion see the Tap Cutting Speed Guide.
6. Benefits of an Integrated Process
Designing the drilling, guiding and tapping tools and flow together raises efficiency, lowers tool wear and stabilizes quality — ideal for CNC production, precision parts, molds and automotive components.
FAQ
Q: Do I need a guide hole or chamfer before tapping?
Recommended. A guide hole or chamfer helps the tap enter cleanly and avoids torn threads and interference; for blind holes, a flat or center drill can true the bottom for better accuracy.
Q: How do I choose taps for through vs blind holes?
Use a spiral-point tap for through holes (chips push forward) and a spiral-flute tap for blind holes (chips lift out). High-strength or thin plate can use a forming (chipless) tap.
Q: Deep-hole tapping keeps breaking — what helps?
Deep holes need evacuation. Use a through-coolant (oil-hole) deep-hole drill for the pilot, a dedicated tap, and steady coolant with pecking to lower breakage risk.
Q: How do I tap on an inclined or curved face?
First true the incline/curve with a flat or special-edge drill to create a flat locating face, then drill and tap — this reduces eccentricity and vibration and improves location.
This article is part of Drill Bits: The Complete Guide - Start From Depth-to-Diameter, Then Pick the Drill and Set the Conditions; that guide shows how the whole topic fits together.
Published: 2026-03-23 | Last updated: 2026-10-31









