
Machine Tool Daily Maintenance: Chips, Lubrication and Accuracy Checks
A machine tool's accuracy is not fixed on the day it arrives — daily operation slowly consumes it. And the fastest cause of that loss is usually the least conspicuous one: chips that were not cleared away. This article sets out what to do daily, weekly and annually, and how to read an accuracy check.
1. Three Things to Do Every Day
Ten minutes before the end of the shift covers all of it, and the cost of skipping it accumulates quietly:
Clear the chips — especially from the way covers and the corners of the table. Check oil levels — that lubricant and hydraulic oil sit between the marks. Listen — whether the spindle and the axis moves sound any different from usual.
The third is the easiest to skip and often the only early warning there is: when a bearing or a guideway begins to degrade, the sound changes before the accuracy does.
2. Why Chips Are the Number One Enemy
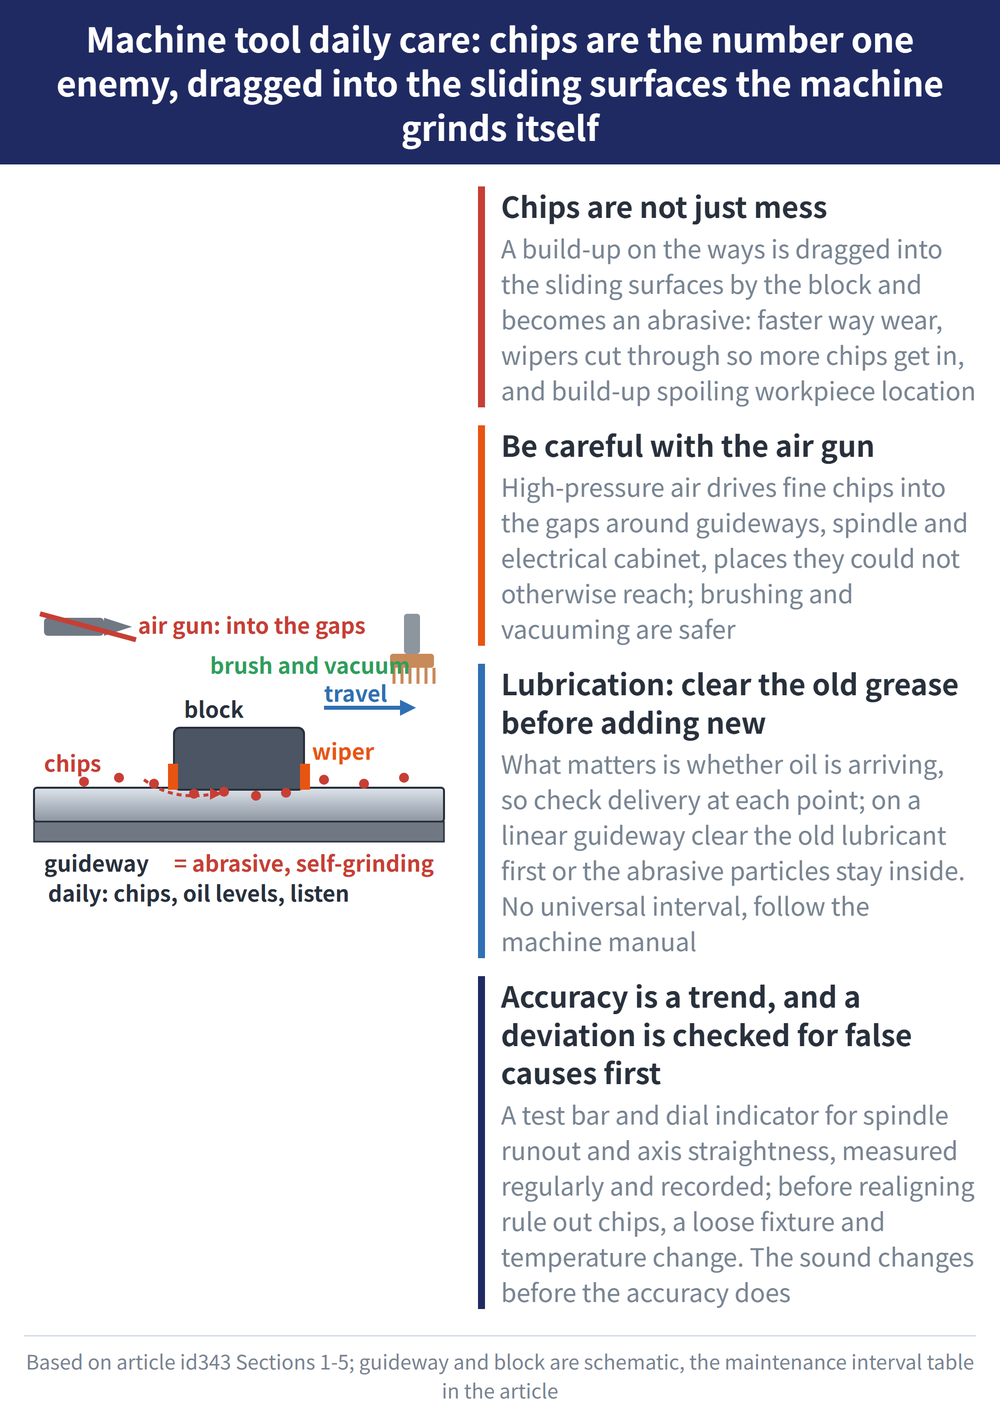
Chips are not just mess. A build-up on the ways gets dragged into the sliding surfaces by the blocks and becomes an abrasive medium — in effect the machine grinding itself.
Three consequences follow: accelerated way wear, wipers cut through (so more chips get in, and the cycle feeds itself), and chip build-up affecting how accurately the workpiece locates.
Be careful blowing chips off with an air gun. High-pressure air drives fine chips into the gaps around guideways, the spindle and the electrical cabinet — places they could not otherwise reach. Brushing and vacuuming are safer.
3. Lubrication: Clear the Old Grease Before Adding New
What matters in a lubrication system is not only whether there is oil but whether the oil is arriving. A line in a centralised system can be blocked so that one point receives nothing, which is why the delivery at each lubrication point should be checked periodically.
Topping up a linear guideway involves one step that is routinely skipped: clear the old lubricant before adding new. Adding fresh grease on top of old grease loaded with contamination leaves the abrasive particles inside the guideway.
There is no universal relubrication interval — it depends on stroke length, travel speed, load and how clean the environment is. Follow the recommended value in the machine's own manual; this is not a parameter to copy from someone else.
4. Maintenance Intervals by Layer
| Interval | Items |
|---|---|
| Daily | Clear chips, check lubricant and hydraulic levels, listen to the machine |
| Weekly | Clean the heat exchanger filter, check coolant condition and concentration |
| Monthly | Check wipers, the air preparation unit and delivery at each lubrication point |
| Annually | Change hydraulic tank oil, professional service and accuracy inspection |
⚠ The table above is one supplier's practical recommendation; models and duty cycles vary widely, so work from your machine's own maintenance manual. On day-to-day coolant management see Managing Cutting Fluid and Consumables: Mixing, Daily Checks and Protection.
5. Accuracy Checks
Accuracy drifts with use, so the habit to build is measuring regularly and keeping the records — a single reading means little, the trend is what means something.
The common method is a test bar with a dial indicator to check spindle runout and the straightness of each axis; another approach is to take a test cut with a gauge part and measure the result. Permissible values are specific to each maker and model and cannot be transferred between machines. On a lathe, working back from defects in the part to the machine fault is covered in Lathe Accuracy and Troubleshooting: Taper, Ripples and Uneven Pitch Point to the Machine; the full set of CNC lathe checks is in Checking a CNC Lathe's Accuracy and Tracing Its Faults: 18 Tests and the Outside-In Rule; what to measure when accepting a machining center is in Checking a Machining Center's Accuracy: Three Classes and Five Conditions Before You Measure.
If a clear deviation shows up, the first thing to check is usually not the machine itself — chips, a loose fixture, a change in temperature can all create a false reading. Rule those out before talking about realignment. On shop floor safety rules see Machine Shop Safety.
6. Thermal Deformation and Warm-Up
If the first few parts after start-up keep drifting in size, or morning and afternoon parts come out different, the cause is usually not the tool but a machine that has not yet settled thermally. Studies cite thermal error as 40–70% of a machine tool's total error and the main source of part error: heat sources in and around the machine make the structure expand and contract, and the relative position of tool and workpiece shifts with it.
So warm the machine up until its temperature is stable before setting tools and cutting. Acceptance rules likewise require temperature-related accuracy to be measured only after the machine has warmed up and stabilised — a cold machine does not show its working accuracy. The routine checks in the previous section should also be taken in the same warmed-up state, or the records cannot be compared.
How long warm-up takes differs from machine to machine, and you can measure it yourself: with a tool-length probe, measure tool length every 5 minutes of spindle running for 1 hour and plot the curve. Where the curve flattens is this machine's warm-up time; after a speed or tool change it must settle again. For the method see Hard Milling or EDM: When to Finish a Hardened Mold with a Cutter; for telling thermal drift apart from insert wear see Turning Troubleshooting Guide | Tool Wear, Accuracy and Surface Issues.
7. Frequently Asked Questions (FAQ)
Q: Can I blow chips off with an air gun?
Be careful. High-pressure air drives fine chips into the gaps around guideways, the spindle and the electrical cabinet, places they could not otherwise reach. Brushing and vacuuming are safer.
Q: What should I watch when relubricating a linear guideway?
Clear the old lubricant before adding new. Adding fresh grease on top of contaminated old grease leaves abrasive particles inside the guideway and accelerates wear.
Q: How often should accuracy be inspected?
It depends on the maintenance manual and how hard the machine is worked. A common approach is to include it in the annual professional service, and to measure and record in between to watch the trend.
Q: Does a measured deviation mean the machine is faulty?
Not necessarily. Residual chips, a loose fixture and temperature change can all create a false reading. Rule those out before deciding whether realignment is needed.
This article is part of CNC Machining Fundamentals: The Complete Guide - Know the Machine and Shop, Then Read the Drawing; that guide shows how the whole topic fits together.
Published: 2026-08-25 | Last updated: 2026-10-25









