
Peck Drilling: When You Need It and How to Set It
Peck drilling means drilling a little, then backing off, so chips clear out and coolant gets back in. Not every hole needs it — used in the wrong place it just wears the tool and lengthens cycle time. The key is judging when to peck, and how to set the retract amount and peck depth.
1. What Peck Drilling Actually Solves
In a deep hole, chips that cannot escape wrap the tool, pack the flutes, cause re-cutting and build up heat — at best scratching the wall, at worst snapping the drill. Peck drilling uses an interrupted retract to carry chips out and let coolant re-enter the bottom of the hole, pulling chip evacuation out of continuous cutting and handling it on its own.
Core idea
Peck drilling trades time for chip evacuation and cooling: each retract is one more chance to clear chips and let coolant in. The cost is a longer cycle, so peck only when the hole genuinely needs it.
2. Choosing Between the Two Retract Modes
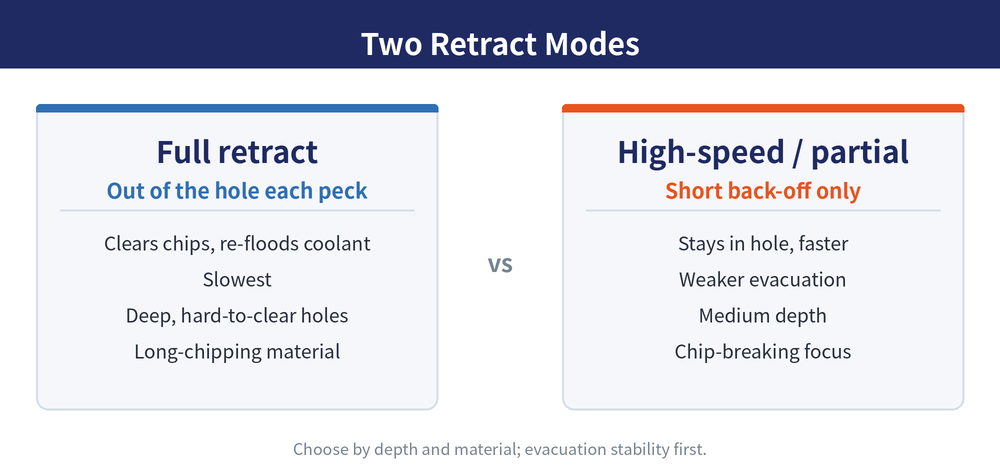
Peck drilling comes in two retract strategies, differing in how far the tool backs off and how much evacuation that buys:
| Mode | Action | Advantage | Best for |
|---|---|---|---|
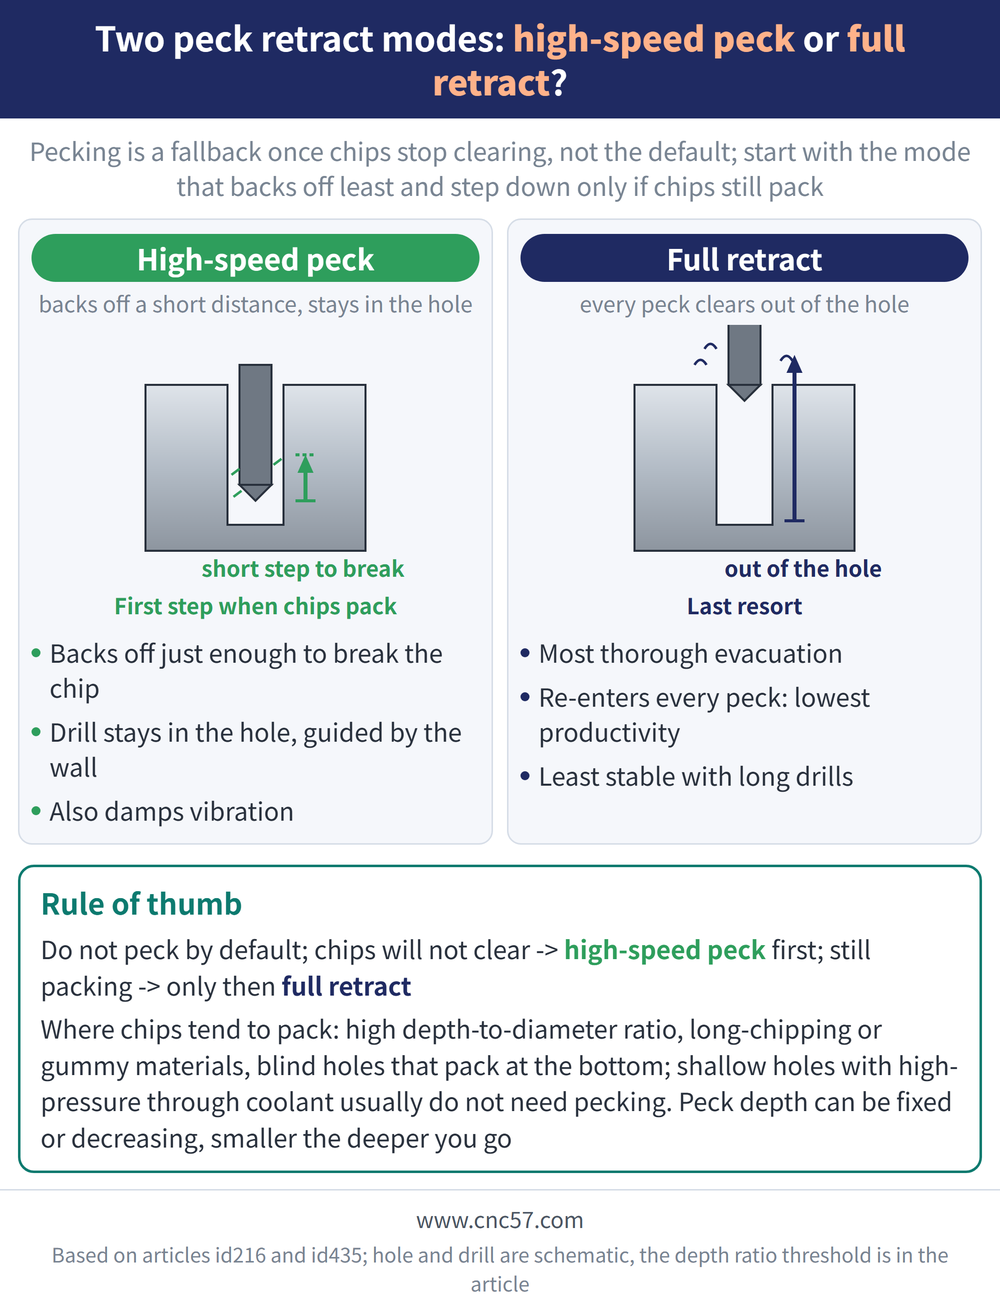
| Full retract | Every peck clears right out of the hole for complete chip evacuation and re-entry of coolant | Most thorough evacuation; chips never accumulate inside the hole | Only when a short peck still cannot clear chips: lowest productivity, least stable with long drills |
| High-speed / partial peck | Backs off only a short distance to break the chip, without leaving the hole | Faster cycle; relies on chip breaking to keep evacuation going | First step once chips start to pack; the drill stays in the hole, which also damps vibration |
The order is: do not peck by default; when chips will not clear, try high-speed peck first; only if chips still pack, use full retract. Full retract re-enters the hole on every peck, so productivity is lowest and tool life and hole quality may suffer, more so the longer the drill. For the full three-step fallback, see Drilling Cycle Selection. For the overall deep-hole strategy, see the Deep-Hole Drilling Methods Overview.
3. When You Need to Peck
Do not peck by default. The table lists situations where chips tend to pack: when you meet one, check whether chips actually clear, peck only if they do not, and start with high-speed peck:
| Situation | Chip risk and what to do |
|---|---|
| High depth-to-diameter ratio (roughly L/D>3–5, typical) | High risk: the deeper the hole, the harder chips clear; peck once they stop clearing |
| Long-chipping / gummy materials | Chips resist breaking: when they wrap, use high-speed peck to break them |
| Shallow holes with high-pressure through-tool coolant | Usually not: the internal coolant already flushes chips out, and pecking only lengthens cycle time |
| Blind holes where chips pack at the bottom | Nowhere to clear at the bottom: when chips pack, retract to clear them and avoid re-cutting |
The depth-to-diameter threshold is a typical value; refer to the catalogue or standard. Whether pecking is actually needed still depends on the material, cooling method and drill geometry.
If chip evacuation or chip wrapping is already going wrong, use the Drilling Troubleshooting Guide to find the root cause first, then decide whether pecking is the fix.
4. How to Set the Parameters
Peck depth can be fixed or decreasing: a decreasing scheme (smaller pecks the deeper you go) keeps chips from getting too long where evacuation is hardest. Match it with the right feed — too low actually causes rubbing and work hardening, especially when re-entering the cut at the hole bottom.
Set speeds and feeds by diameter and material as described in the Drilling Parameters Guide; for the formulas and cycle-time estimates, see the Drilling Formula Handbook. For the principles of chip formation and chip breaking, see Drilling Feed Rate vs Chip Formation. For deep-hole-specific drills such as oil-hole drills, see the Deep Hole Drilling Guide.
Peck depth and the decreasing ratio are typical practice; refer to the catalogue or standard. Confirm actual values against the drill maker's recommendation and a trial cut.
Last updated: 2026-10-31
5. Frequently Asked Questions (FAQ)
Q: When do I need peck drilling?
Do not peck by default. A high depth-to-diameter ratio (roughly L/D>3–5, typical), long-chipping or gummy materials, and blind holes that pack chips at the bottom are where chips tend to pack; peck only when chips actually stop clearing, starting with high-speed peck and moving to full retract only if that fails.
Q: What is the difference between full retract and high-speed peck?
High-speed peck backs off only a short distance to break the chip and keeps the drill in the hole, so it is faster and the hole wall steadies the drill and damps vibration; it is the first step once chips pack. Full retract clears out of the hole on every peck for the most thorough evacuation, but productivity is lowest and every re-entry can hurt the tool and the hole, so use it only when high-speed peck still cannot clear the chips.
Q: How much peck depth should I set?
Peck depth can be fixed or decreasing, with a decreasing scheme taking smaller pecks the deeper you go to avoid over-long chips. Actual values are typical practice — refer to the catalogue or standard — and compute speeds and feeds with the Drilling Formula Handbook, then confirm with a trial cut.
Q: Do shallow holes need pecking too?
Usually not. Shallow holes clear chips easily, and with high-pressure through-tool coolant flushing them out, pecking only lengthens cycle time — unless it is a blind hole packing chips at the bottom that needs a retract to clear them.
For the full reading guide on this topic, see Chip Control: A Complete Reading Guide.
This article is part of Drill Bits: The Complete Guide - Start From Depth-to-Diameter, Then Pick the Drill and Set the Conditions; that guide shows how the whole topic fits together.









