
PVD Insert Coating Chart: ISO Classes & Grade Selection
PVD insert coating is the key technology for high-precision and interrupted cutting, with high toughness and chipping resistance, suited to stainless steel, alloy steel and high-hardness materials. By cross-referencing ISO classes (P, M, K, S, H) and brand grades you can quickly find substitute inserts and optimize efficiency. This guide covers the PVD insert cross-reference and selection logic to improve stability and tool life. For the ISO workpiece groups, see ISO Workpiece Material Classification.
What Is PVD Insert Coating?
PVD (Physical Vapor Deposition) is a low-temperature coating process with a thinner film; key traits and uses below.
| Item | Detail |
|---|---|
| Coating traits | Thin coating (high toughness), strong chipping resistance, good for interrupted cutting |
| Common use | Milling, stainless steel, high-precision machining |
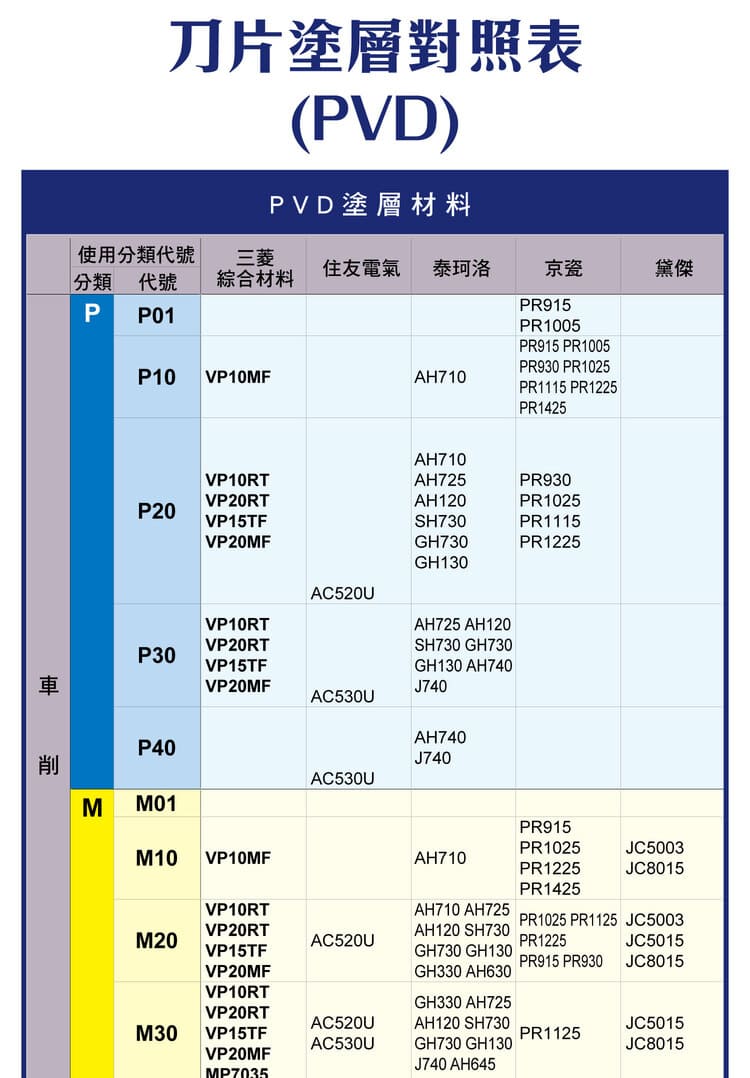
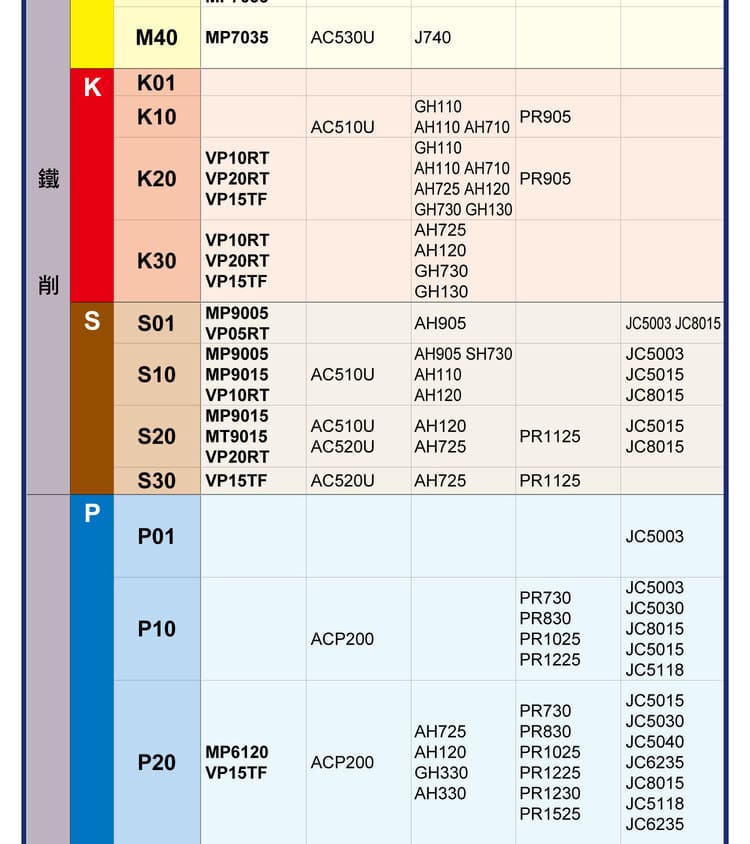
ISO Classes and Common Grades
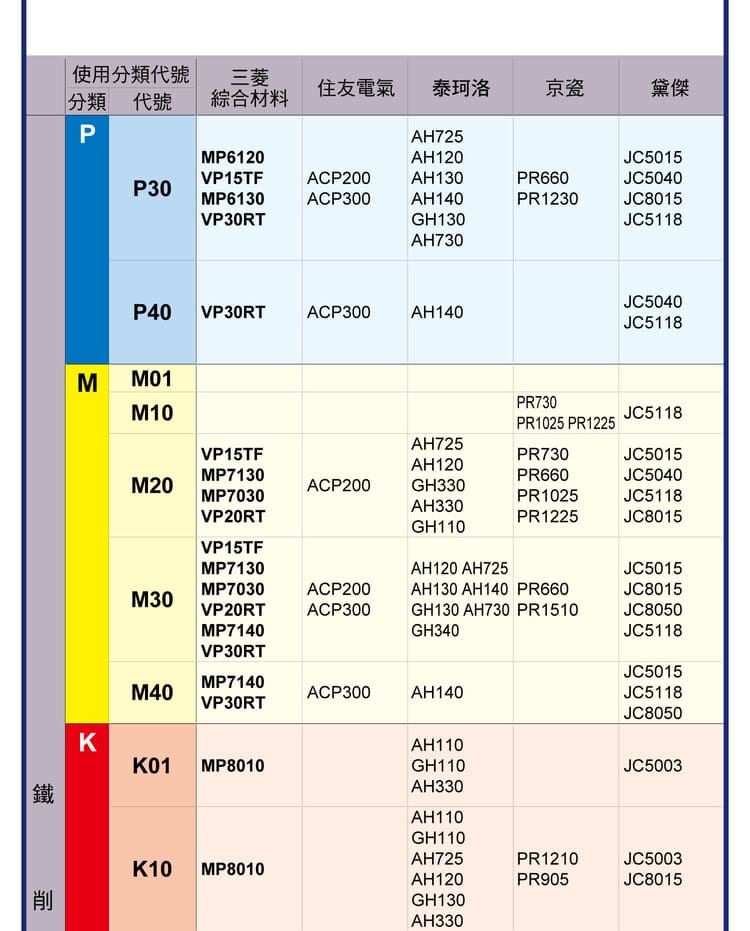
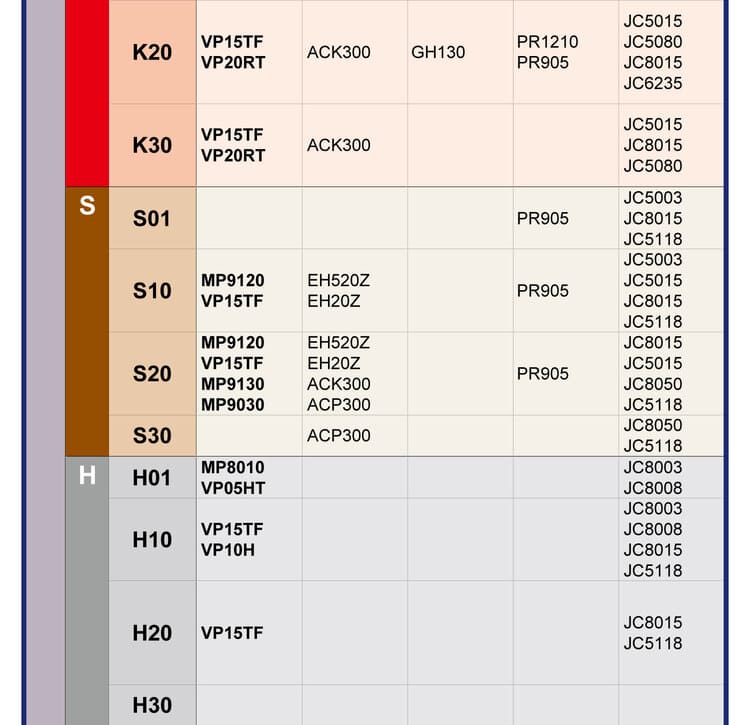
By ISO group: material, traits and common PVD insert example grades for same-group substitution.
| ISO group | Material / trait | Common grades (example) |
|---|---|---|
| P | Carbon / alloy steel | VP10MF, VP20RT, VP15TF, AH710, AH725, GH130, PR930, PR1025, PR1225 |
| M | Stainless (gummy, work-hardening) | VP10MF, VP20RT, AC520U, AC530U, PR1025, PR1225 |
| K | Cast iron (high wear demand) | VP10RT, VP15TF, GH110, AH110, PR905 |
| S | Titanium, superalloys | MP9005, MP9015, AH905, EH520Z, PR1125 |
| H | Hardened steel (high hardness) | VP05HT, VP10H, BH200, BH250, KC635M |
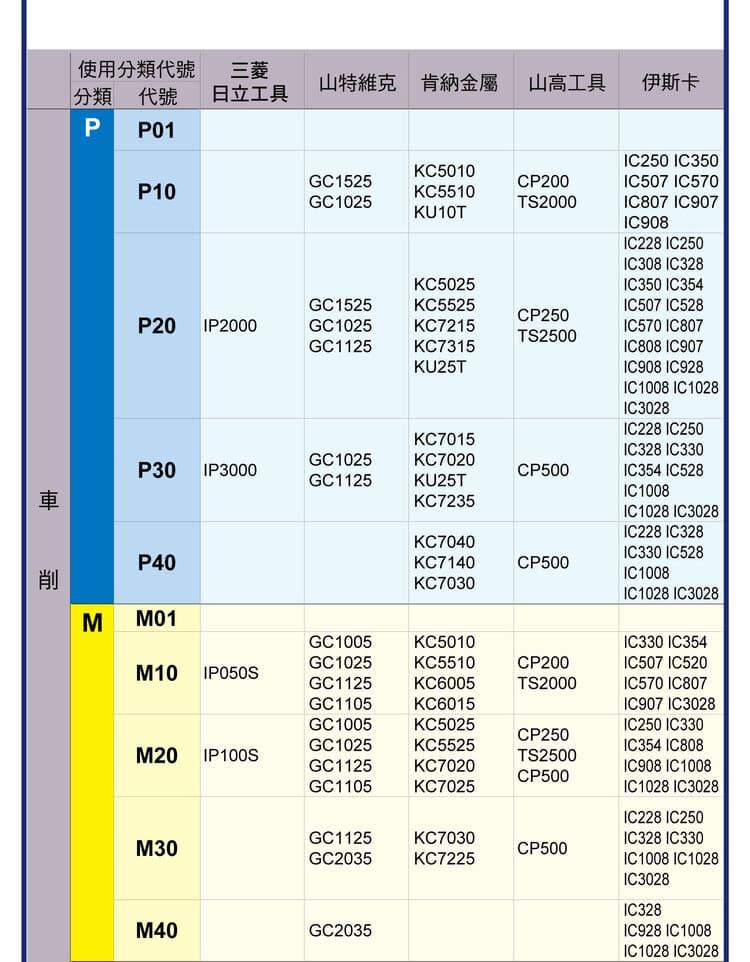
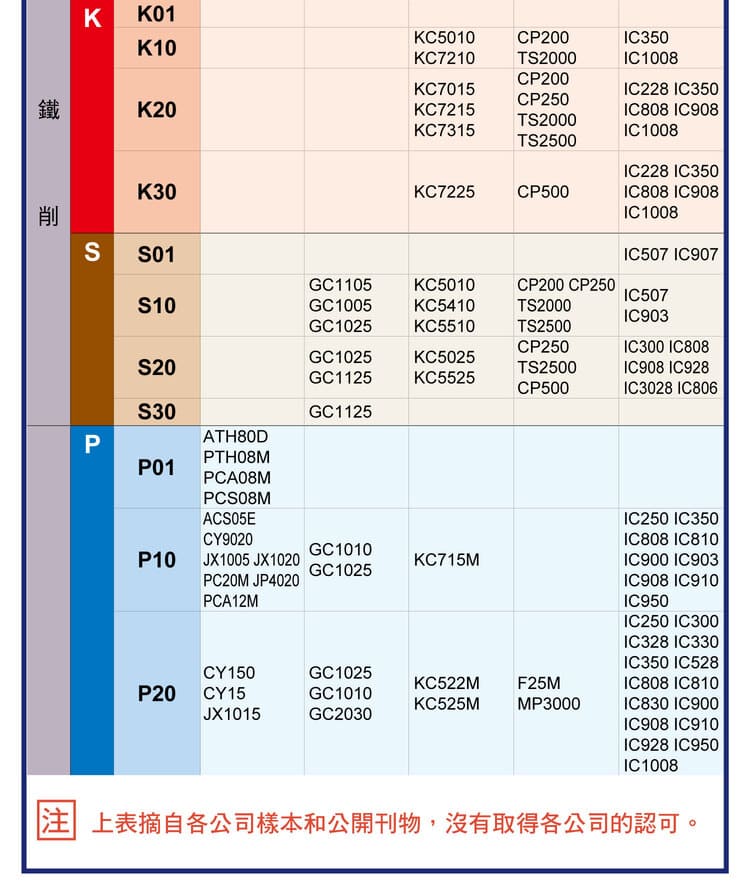
Brands Covered
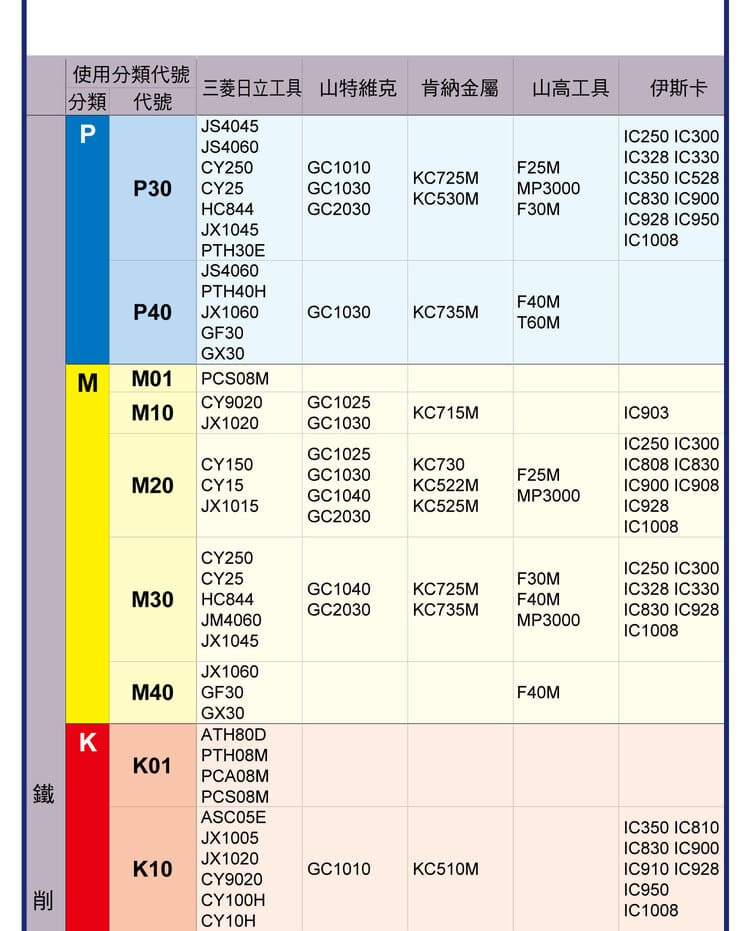
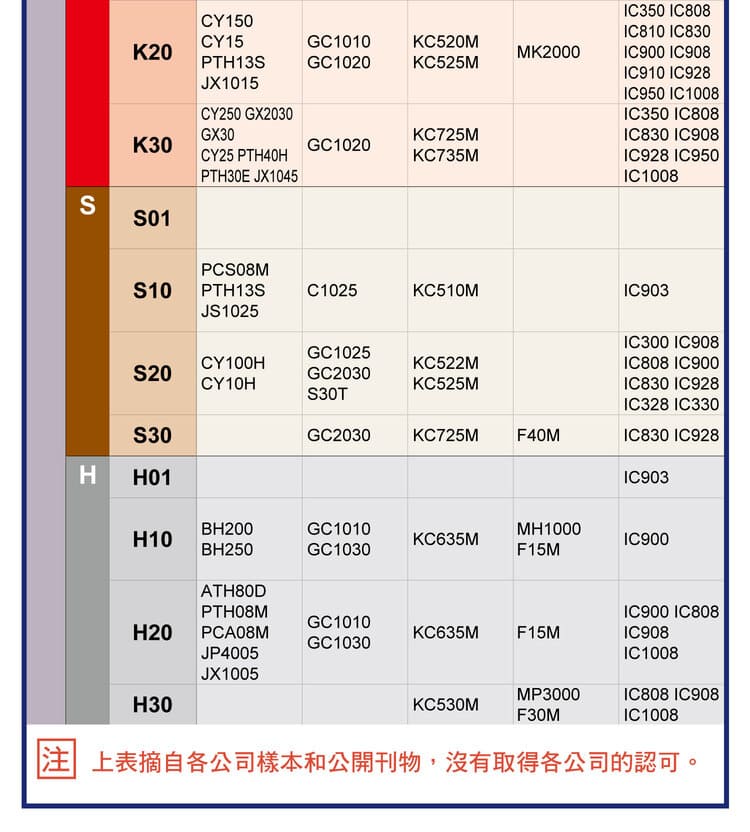
The chart consolidates major tool brands; the same ISO class points to substitutes with similar application and performance.
| Brand | Origin |
|---|---|
| Mitsubishi Materials | Japan |
| Sumitomo | Japan |
| Tungaloy | Japan |
| Kyocera | Japan |
| Daijet | Japan |
| ISCAR | Israel |
Turning vs. Milling Inserts
| Type | PVD use | Emphasis |
|---|---|---|
| Turning insert | For finishing and stainless | High surface quality |
| Milling insert | PVD is mainstream | Strong impact resistance |
Continuous / heavy cutting mostly uses CVD—see CVD Insert Coating Chart; the ISO and brand overview is in Carbide Insert Coating Chart.
Advantages of PVD Coating
| Advantage | Detail |
|---|---|
| High toughness | Strong chipping resistance |
| High precision | Good surface finish |
| Suits interrupted cutting | Reduces tool breakage |
PVD Insert Selection
| Scenario | Recommended grade |
|---|---|
| Finishing | P10–P20 |
| Stainless | M10–M30 |
| Cast iron | K10–K30 |
| High-hardness | H series |
Three-step tool selection: Step 1 classify material (steel→P, stainless→M, cast iron→K); Step 2 assess conditions (interrupted→PVD, continuous→CVD); Step 3 pick grade (substitute via the brand chart). Set actual parameters by machine and material hardness—see End Mill Cutting Conditions Guide.
※ Grades are common examples compiled from the source for same-ISO-group substitution reference only; verify exact equivalents and applicability against each brand's catalog.
FAQ
What machining suits PVD coating?
PVD is thin, tough and chip-resistant, suited to milling, interrupted cutting, stainless and high-precision work, plus high-hardness materials (H series).
How do I choose between PVD and CVD?
Choose PVD for interrupted cutting, milling, finishing and high-hardness materials (thin, tough, chip-resistant); choose CVD for continuous cutting, turning and heavy cutting (thick, wear- and heat-resistant).
Why do milling inserts mostly use PVD?
Milling is interrupted cutting with repeated impact; PVD's thin coating is tough and chip-resistant, reducing tool breakage—so it is the milling mainstream.
Which PVD grade for hardened steel?
It is the H series; use high-hardness PVD grades (e.g. examples VP05HT, VP10H). For even higher hardness, switch to CBN. Verify against the maker's catalog.
For the full reading guides on this topic, see Tool Life and Wear: A Complete Reading Guide and Insert Selection: A Complete Reading Guide.
This article is part of Tool Materials and Coatings: The Complete Guide - Separate Substrate From Coating, Then Work Back From the Workpiece; that guide shows how the whole topic fits together.









