
Surface Finish: A Complete Reading Guide
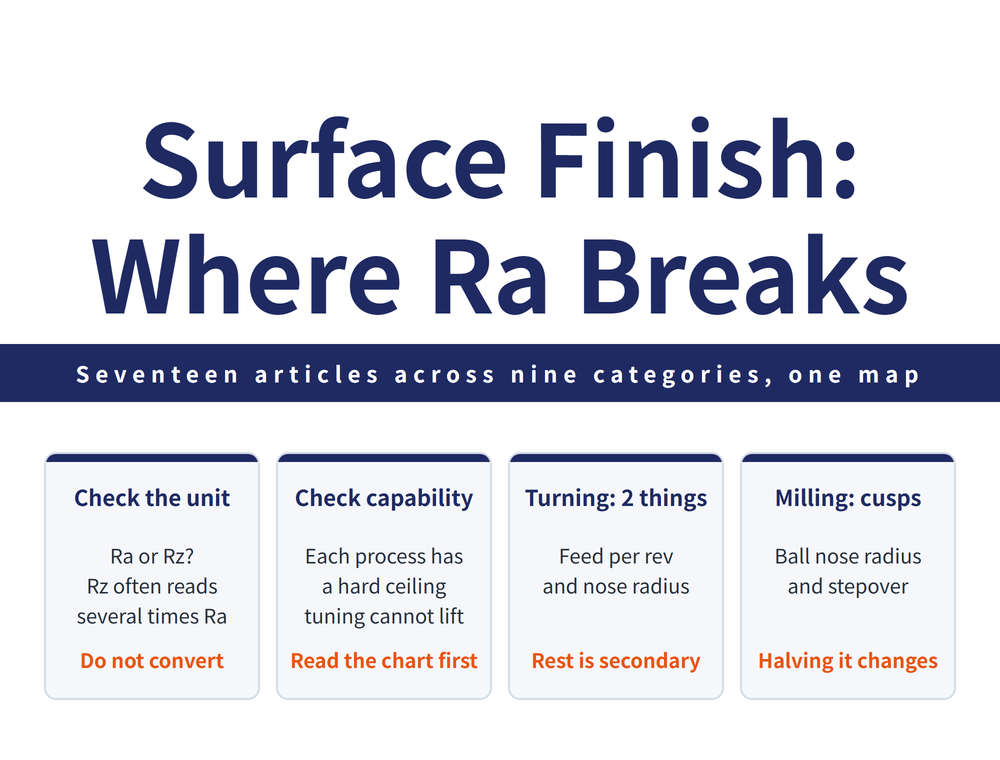
Surface finish is the topic that spans the most categories on this site: 17 articles across 9 of them. This page is a reading guide. It does not repeat what those articles say; it only answers one question: which one should you open, given where you are stuck.
1. First, Which Number Are You Talking About: Ra, Rz or RzJIS?
Understand the number on the drawing first; nothing after that matters otherwise. On the same surface the Rz figure is usually several times the Ra figure (about 4× in the standard series), so reading the wrong parameter misjudges the whole batch.
| Article | When to open it |
|---|---|
| Surface Roughness: Ra, Rz and RzJIS Explained | Ra 1.6 on a drawing and Rz 6.3 are not the same requirement; definitions, maths and conversion all live here |
2. Can This Process Even Reach the Ra You Need?
Not every process can reach the Ra you want. Confirm the capability band before touching parameters.
| Article | When to open it |
|---|---|
| Surface Roughness Chart by Process | Start with capability: the Ra band turning, grinding and polishing each reach |
| Machining Route Selection | When one operation cannot reach it: which operations to chain from rough to finish (38 process routes) |
| How Easy Is a Material to Cut? Machinability | Change the material and the same parameters behave differently; finish is one of the four axes of machinability |
| Cermet Cutting Tool Guide | When you are chasing a mirror finish, the tool material itself becomes the limit |
3. Turning: Feed and Nose Radius Already Decide Half of It
Theoretical roughness in turning comes from feed per revolution and nose radius. Fix those two first.
| Article | When to open it |
|---|---|
| Turning Tool Nose Radius Selection Guide | The trade-off between nose radius, finish and tool life; read this one first on the turning side |
| Turning Wiper Inserts | Why doubling the feed can improve the finish; it is edge geometry, not magic |
| Turning Formulas Reference | The formulas, when you need to calculate theoretical roughness |
| Turning Cutting Conditions Guide | How speed, feed and tool life interact, which sets how far you can back the feed off |
4. Milling: Ball Nose Radius and Stepover Set the Cusp Height
Milling is about cusp height: ball nose radius and stepover. Halve the stepover on the same tool and the surface changes completely.
| Article | When to open it |
|---|---|
| Milling Surface Roughness Formula | The ball nose R and stepover P formula, the core of the milling side |
| Face Milling Surface Finish Guide | Wiper inserts, runout and feed, and how to adjust them |
| Face Milling Formula Reference | vc, fz, vf, Tc and Pc in one place; you need them before deciding if the feed can come down |
| Cutting Conditions vs Surface Finish | How flute count and side milling affect the machined face |
5. Inside a Hole: Drilling, Reaming, Boring and Tapping
You cannot easily see or measure inside a hole, so it comes down to operation sequence and chip control.
| Article | When to open it |
|---|---|
| Hole Accuracy and IT Tolerance Guide | A hole is not an outside diameter; the drill, ream and bore sequence changes the outcome |
| Boring Troubleshooting Guide | Feed marks, vibration and what to do when power runs short |
| Pipe Tap Troubleshooting Guide | A rough thread flank is one of the most common complaints in pipe tapping |
6. When You Cannot Calculate It, Achieve It or Measure It Reliably
Three entry points: the formula sheet if you need to calculate, the troubleshooting guide if it will not come out, and the measurement guide if your reading does not match the drawing.
| Article | When to open it |
|---|---|
| Machining Formulas Cheat Sheet | Turning, milling, drilling and boring on one page, when you are in a hurry |
| Turning Troubleshooting Guide | Surface problems, tool wear and dimensional error often share one root cause |
| How to Measure Surface Roughness | When your Ra reading does not match the drawing or the customer’s, check first that the measuring method is the right one |
7. Frequently Asked Questions (FAQ)
Q: Can I convert Ra to Rz directly?
No. They are different statistics and only relate approximately for specific profiles. Read what the drawing actually calls out; do not convert and ship.
Q: Will the lowest possible feed give the best finish?
No. Too low a feed makes the edge rub instead of cut, which builds up edge and leaves bright marks. The nose radius and wiper articles in section 3 explain why.
Q: Why is surface finish content spread across nine categories?
Because every machining method runs into it, while the category axis follows product lines, not problems. Cross-category problems are handled by this guide layer and by tags, not by adding a category.
Q: I just need one number, not a whole article.
The process capability chart in section 2 and the formula cheat sheet in section 6 are both look-up material.
Published: 2026-08-10 | Last updated: 2026-10-21









