
Manufacturing Process: The Complete Guide - Set the Datum First, Then Sequence, Allowance and Dry Cutting
This line holds 18 articles on one subject: how a drawing becomes a sequence of operations that can be made, and costed. The order is fixed - see the whole route and set the datum, then decide how many passes and how much stock to leave, then pick the machine and work out the time, then whether it pays at all, and last whether to run dry. Reverse it and you keep missing the problem: a part machined off the wrong datum will never be explained by checking the machine.
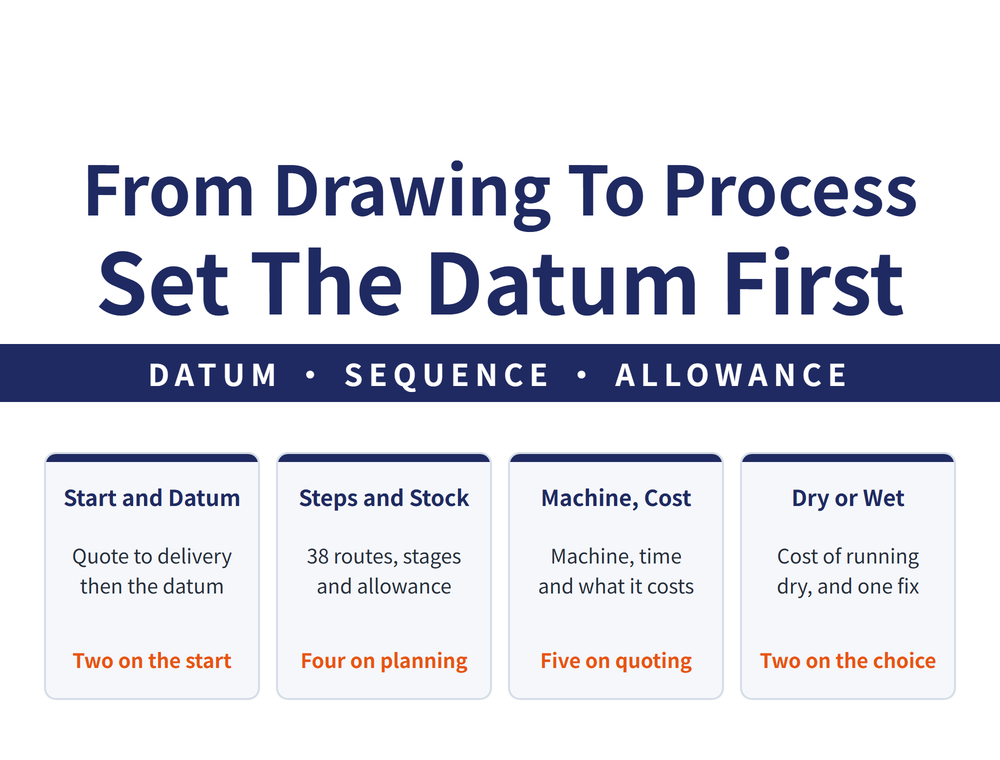
1. The order here is fixed: see the whole route, then set the datum
Process planning does not start with choosing a machine. First know which stages a part passes through, then decide which face the first cut references. Only then can the rest of the operations be laid out.
| Article | When to read it |
|---|---|
| From Quote to Delivery | The entry point. The whole route before the detail |
| Choosing a Locating Datum | When two machinists plan the same drawing differently |
One line from the second article is worth remembering up front: pick the wrong datum and every later operation is compensating for it. This is also where process problems part company with machine problems - no amount of machine maintenance will explain this kind of error. To read what the drawing is actually asking for, see Reading Tolerance and Fit in the fundamentals category; hole tolerance and runout form their own line, in Hole Accuracy: A Complete Reading Guide.
2. How many passes, in what order, and how much to leave
With the datum set, three things get decided together: how many passes this surface needs, how those passes are ordered, and how much stock sits between them. These four articles are the core of the line.
| Article | When to read it |
|---|---|
| Machining Route Selection | Use it as a lookup. 38 chains, read backwards |
| Sequencing Machining Operations | Deciding on stages, and concentration vs division |
| Roughing, Semi-Finishing and Finishing | When you want to know why one pass will not do |
| How Much Machining Allowance | When allowance is still a number picked by feel |
How to read the four: the first decides which passes, the second and third decide their order, the fourth decides what sits between them. The last one carries an idea that often gets missed - the allowance for this operation cannot be smaller than the error left by the one before it, so it is not this operation's decision alone. Where heat treatment belongs in the sequence is in the second article.
3. Machine, time, and a list you can tape to the machine
Once the sequence is set, what remains is which machine with what tooling, how long the batch will take, and the rules the shop floor actually follows.
| Article | When to read it |
|---|---|
| Machine, Tooling and Time Standards | When quoting, or planning capacity |
| General Machining Practice Rules | When you want a list to tape beside the machine |
The first article contains one order that must not be reversed: set depth of cut first, then feed, and speed last - do it the other way round and tool life drops quickly. The second draws on an industry standard published in mainland China, and the article marks which clauses need local judgement in Taiwan. Holding the part so it neither moves nor distorts is a complete line of its own - locating pins, clamping force, pneumatic or hydraulic power - all of it in Workholding and Fixtures: The Complete Guide.
4. Once You Have the Time, Work Out Whether It Pays
A time figure does not tell you the job is worth running that way. What has to be settled here is how long tool life should be and how fast to cut, and neither has a single answer: the parameters only resolve once you pick minimum cost or maximum output, and the same tool runs at different speeds under those two goals.
| Article | When to read it |
|---|---|
| How Long Should Tool Life Be | Before quoting or planning capacity, when you must pick cost or output |
| How Fast to Run | Once the goal is set and it has to become an actual speed and feed |
| Machining Cost Structure | When you want to know whether saving on tooling helps at all |
Read them in that order, and note that the third one rewrites the first two: tooling is a smaller share of machining cost than most people assume, so stretching tool life does not necessarily save money - the time on the machine does. The time figure from section 3, set against the cost structure here, is what a quote can actually stand on.
5. The last decision: whether to take the coolant away
This belongs to the planning stage, not to someone reaching over and closing the nozzle. It drives tool material, tool geometry and chip evacuation, so it has to be settled while the method is still being chosen.
| Article | When to read it |
|---|---|
| The Cost of Dry Cutting | Read it before you decide. It only argues against |
| What Is Electrostatic Cooling | When weighing dry cutting and looking for a middle way |
The first article holds a counter-example that is easy to misread: in the same aluminium alloy, drilling and boring point the opposite way, so "this material can be cut dry" cannot be applied across the board. Dry cutting itself is a longer line - dry milling, dry drilling, dry tapping, and how tool material and geometry have to change - spread across the end mill, drill, tap and tool material categories. These two are its entry point at the planning level, not the whole of it.
6. After heat treatment: check the parts, then see how much is left to cut
Where heat treatment falls in the sequence is settled in section 2; once the parts go out and come back, two things need checking before finishing: whether the batch itself is right, and how deep the surface layer still lets you cut.
| Article | When to read it |
|---|---|
| Heat-Treated Parts Come Back Wrong: Uneven Hardness, Distortion, and the Kind That Cracks Two Days Later | When finishing stops going smoothly on parts back from heat treatment: tool wear varies, sizes do not match, some crack after two days |
| How Much Is Left to Cut on a Case-Hardened Part: Case Depth Is Your Allowance Ceiling | When a surface-hardened part is due for finishing and you need to know how much is left to cut |
Read them in order: the first confirms the parts are sound, the second decides how much you can still cut. The first sets out the three things to measure at goods-in and what each symptom means for your machining - change the tool, re-plan the allowance, or simply wait. The second covers the side section 2 does not: allowance has a lower bound set by the previous operation, and a surface-hardened part adds a ceiling - you can only cut as deep as the case goes, and once it is ground through the hardness is gone.
7. Changing the method, and cutting the stock: hardened molds by cutter, band saw blades chosen and checked
A planned sequence still gets revisited. This section covers two cases: whether hardened mold finishing should move from EDM to a cutter, and the stock cutting at the very start.
| Article | When to read it |
|---|---|
| Hard Milling or EDM: When to Finish a Hardened Mold with a Cutter | When hardened mold finishing still goes to EDM and you want to know if an end mill can take it |
| Choosing a Band Saw Blade: Terms, Pitch in TPI, and Tooth Forms | When all the catalogue gives is width, thickness and a pitch like 2/3 or 3/4 |
| Band Saw Blade Troubleshooting: Five Failure Types and Two Measurable Benchmarks | When the saw cuts crooked, leaves a rough face, breaks a blade or chips teeth, before fitting a new blade |
The point of the first is that not every shape can switch, and three conditions must be met first; large molds and small parts also follow different routes. The other two are a pair: choose the right blade with the second, and when a cut goes wrong, work through the five failure types in the third; excessive feed alone is a common cause in four of the five, so before fitting a new blade, measure the two benchmarks and check the feed.
8. Frequently Asked Questions (FAQ)
Q: Where should I start with these 18 articles?
It depends on the problem in front of you. New to this, start with From Quote to Delivery in section 1; it gives the whole route. Drawing in hand and ready to plan, read Choosing a Locating Datum, the first real decision. If the drawing itself is unclear, fill in Reading Tolerance and Fit first. To decide how many passes, go straight to the route chart in section 2. Quoting or planning capacity, jump to section 3, then section 4 for whether it pays. Already weighing dry cutting, read section 5.
Q: A part is out of tolerance - is it the sequence or the machine?
Look at what the error tracks. Same batch, same machine, and the error appears in the same place or the same direction every time - that usually points at the datum or the sequence, and the fixes live in this line: change the datum, add a semi-finishing pass, leave more stock. If the same program gives different results at different times, or accuracy drifts with temperature and hours, look at the machine and the shop floor instead, where the fixes are geometric checks, chip clearing and maintenance - that side starts at CNC Machining Fundamentals: The Complete Guide - Know the Machine and Shop, Then Read the Drawing, with checks and upkeep in Machine Tool Daily Maintenance: Chips, Lubrication and Accuracy Checks and the lathe's accuracy tests and fault order in Checking a CNC Lathe's Accuracy and Tracing Its Faults: 18 Tests and the Outside-In Rule. The two sets of fixes are not interchangeable, and searching the wrong side means never reaching the cause.
Q: How much allowance should I actually leave?
Allowance has a hard lower bound rather than a feel for it: the allowance for this operation cannot be smaller than the error left by the previous one, or this pass will not reach what it is meant to cut. In practice you take a starting figure from a table, then adjust it against four factors - and only one of those four comes from this operation, the rest from the previous pass and the stock. Too much costs cycle time and tool life; too little means the part cannot be finished or has to be reworked. The last article in section 2 takes the four factors apart.
Q: Why does dry cutting sit in the process planning category?
Because it is decided when the method is chosen, not a setting you change halfway through. Whether coolant is used goes on to determine tool material and coating, tool geometry, chip evacuation, and sometimes whether the sequence has to be rearranged. Leave it until the program is written and the tools are loaded, and closing the nozzle is exactly how you land in one of the cases that article warns against. How each tool type is run dry is a separate line crossing several categories; what sits here is only the judgement the planning stage has to make.
Published: 2026-09-10|Last updated: 2026-10-25









